

PCB manufacturing PCB manufacturing
Home > Blog

Security Monitoring PCB Manufacturing & Assembly Services | Factory-Direct

November 11th, 2026

A security monitoring PCB must detect alarm signals accurately, maintain stable communication, and operate reliably around the clock. Unstable sensor inputs, electrical interference, poor solder connections, and power disturbances can cause false alarms, missed events, or equipment shutdowns. How can these risks be reduced without adding unnecessary manufacturing complexity or cost?

EBest Circuit provides factory-direct security monitoring PCB manufacturing and assembly services, including custom multilayer PCB fabrication, SMT/THT assembly, component sourcing, and functional testing. We support intrusion detection controllers, alarm monitoring boards, perimeter security equipment, and communication interface PCBs from prototyping to mass production, with a free DFM check before manufacturing.
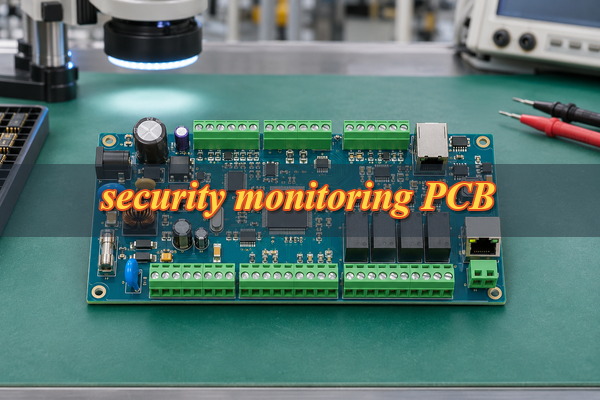
security monitoring PCB, https://www.bestpcbs.com/blog/2026/11/security-monitoring-pcb/

What Causes Signal Failures and False Alarms in Security Monitoring PCBs?

Security monitoring PCB signal failures commonly result from unstable input circuits, power disturbances, defective connections, and electrical interference. However, a false alarm may also originate from the sensor, external wiring, or firmware rather than the PCB itself.

The most common PCB-related causes include:

  • Unstable sensor inputs: Electrical noise, incorrect input resistance, or excessive leakage current may cause the controller to detect an unintended alarm state.
  • Power supply disturbances: Relay switching, insufficient decoupling, or excessive voltage drop can reset the controller or interrupt signal processing.
  • Electromagnetic interference: Switching power supplies, motors, and long field cables may introduce unwanted signals into sensitive monitoring circuits.
  • Soldering and connector defects: Cracked solder joints, insufficient solder, and poor terminal connections can produce intermittent failures.
  • Communication faults: Incorrect termination, damaged traces, or unreliable connections may interrupt Ethernet or RS-485 communication.
  • Moisture and contamination: Condensation, ionic residues, and corrosion can increase leakage currents or damage electrical connections.

For example, an alarm controller that resets when a relay operates may have inadequate power decoupling or insufficient transient suppression. If only one sensor channel produces intermittent alarms, the input circuit, terminal connection, and field wiring should be investigated first.

Fault diagnosis should begin with measured input signals, supply voltages, and communication status. These measurements help distinguish PCB defects from sensor, wiring, and software problems before unnecessary design changes are made.

What Are the Key Design Parameters for Security Monitoring PCB Reliability?

Security monitoring PCB reliability depends on the layer structure, copper thickness, electrical clearances, material selection, and manufacturing tolerances. These parameters must support the required sensor channels, communication interfaces, power distribution, and mechanical installation.

The following table combines common design references with EBest Circuit’s relevant FR-4 PCB manufacturing capabilities.

PCB Parameter Design Reference / Manufacturing Capability Engineering Consideration
PCB Layers 2–4 layers common; EBest standard 1–10 layers, special up to 32 Routing density, grounding, and signal integrity
PCB Material Standard or high-Tg FR-4 Thermal requirements and assembly conditions
Board Thickness 1.0–1.6 mm common; EBest standard 0.4–3.5 mm Enclosure fit, connectors, and mechanical loading
Copper Weight EBest standard: 0.5–5 oz inner, 1–5 oz outer Current capacity, temperature rise, and trace geometry
Minimum Trace / Space 4/4 mil standard at applicable copper weights; 3/3 mil special Copper thickness and fabrication feasibility
Finished Mechanical Hole 0.20 mm standard; 0.15 mm special Hole plating and aspect ratio
Ethernet Differential Impedance Typically 100 Ω PHY specifications and controlled-impedance stackup
RS-485 Termination Commonly 120 Ω at each physical bus end Cable characteristic impedance and network topology
Creepage / Clearance Based on working voltage and applicable safety requirements Isolation, surge protection, and installation environment
Surface Finish ENIG, lead-free HASL, OSP Component pitch, solderability, and assembly requirements

Manufacturing limits cannot automatically be combined in one PCB design. Fine-line processing, heavy copper, small finished holes, and high layer counts must be evaluated against the complete stackup.

For a security monitoring controller combining Ethernet, relay outputs, multiple sensor channels, and switching power supplies, a four-layer PCB may provide better routing flexibility and reference-plane continuity than a crowded two-layer structure.

Connector mounting also deserves attention. Field wiring terminals may experience repeated mechanical loading during installation and maintenance, making PCB thickness, mounting support, and solder-joint reliability important considerations.

Final manufacturing feasibility should be confirmed using the approved PCB stackup, copper distribution, drill files, mechanical drawing, and assembly requirements.

How Can Security Monitoring PCBs Maintain Stable Sensor and Alarm Signal Transmission?

Stable signal transmission requires correct input conditioning, controlled PCB routing, reliable connectors, and appropriate communication termination. Different alarm and monitoring interfaces need different electrical requirements.

The main design considerations include:

  • Digital alarm inputs: Use defined logic thresholds, suitable pull-up or pull-down networks, and debounce filtering to prevent unintended switching.
  • Supervised alarm loops: Apply the specified end-of-line resistor arrangement to distinguish normal, alarm, open-circuit, and short-circuit conditions.
  • Analog sensor inputs: Keep sensitive traces separated from switching regulators, relay drivers, and high-current return paths.
  • RS-485 communication: Use appropriate termination, minimize branch stubs, and verify grounding and common-mode voltage requirements.
  • Ethernet communication: Maintain the required differential impedance and follow the PHY manufacturer’s routing recommendations.
  • Field connectors: Verify terminal assignments, solder-joint integrity, mechanical support, and contact reliability.

For example, a supervised intrusion detector may report different resistance states for normal operation, an alarm, and a wiring fault. Incorrect resistor values, excessive leakage, or an intermittent PCB terminal connection can cause the controller to interpret the wrong state.

Filtering must also match the required response time. Excessive filtering may delay valid alarm events, while insufficient filtering can allow short electrical disturbances to trigger unwanted alarms.

EBest Circuit manufactures security monitoring PCBs according to the approved circuit and layout specifications, with attention to trace geometry, component footprints, connector assembly, and soldering quality. Alarm thresholds and response timing must be verified through customer-defined functional testing.

How Can Security Monitoring PCBs Withstand EMI, ESD, and Power Surges?

Security monitoring PCBs require suitable electrical protection at external power, sensor, and communication interfaces. Long field cables and exposed connectors can carry electrical disturbances into the board, potentially causing signal errors, damaged components, or controller resets.
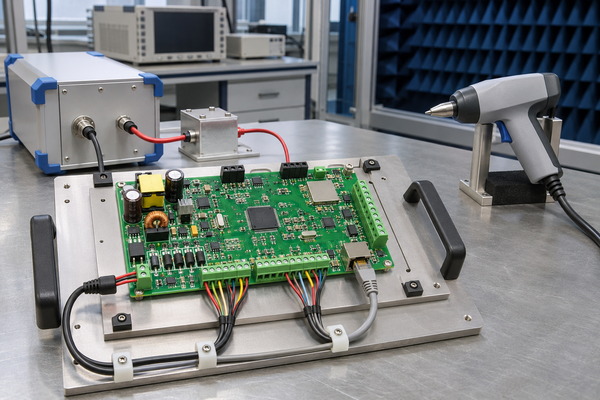
security monitoring PCB, https://www.bestpcbs.com/blog/2026/11/security-monitoring-pcb/

The following protection measures address different electrical risks:

  • ESD protection: Place appropriately rated TVS devices close to exposed connectors and use short return paths.
  • Surge protection: Select protective components according to the specified transient waveform, voltage, and installation conditions.
  • Power input protection: Include suitable reverse-polarity, overcurrent, and transient protection for the power architecture.
  • EMI control: Separate high-current switching paths from sensitive sensor traces and maintain appropriate reference-plane continuity.
  • Communication isolation: Consider galvanic isolation where cable grounding, potential differences, or installation requirements justify it.
  • Inductive load suppression: Apply suitable flyback or transient-suppression circuits to relay coils and other inductive loads.

For security monitoring controllers using 12 V or 24 V DC, protection circuits must accommodate the actual supply voltage range and expected transients. Nominal supply voltage alone is insufficient for selecting protective devices.

PCB layout is equally important. A correctly rated TVS diode connected through a long, inductive return path may provide inadequate protection during a fast transient.

Relevant test methods include IEC 61000-4-2 for ESD immunity and IEC 61000-4-5 for surge immunity. The required test levels depend on the equipment and applicable product standards.

EBest Circuit can manufacture the specified protection footprints, electrical clearances, and trace structures. Complete-system EMC compliance must still be verified through equipment-level testing with representative cables, enclosures, and operating conditions.

Which PCB Manufacturing and Assembly Defects Affect Long-Term Security System Reliability?

Soldering defects, inadequate hole plating, conductor damage, contamination, and connector stress are major manufacturing risks for security monitoring PCBs. These problems may pass an initial power-on check but develop into intermittent failures after temperature changes, vibration, or repeated maintenance.

The manufacturing controls should address the specific defect mechanisms:

  • Insufficient plated-through-hole copper: Control drilling, desmear, and copper plating to reduce weak or discontinuous hole-wall connections.
  • Conductor defects: Use suitable imaging, etching control, PCB AOI, and electrical testing to detect damaged traces, unwanted copper, and open circuits.
  • Poor solder-joint formation: Control stencil printing, component placement, and reflow conditions to reduce insufficient solder, bridges, and improperly formed joints.
  • Through-hole connector defects: Verify solder filling, alignment, and mechanical support for terminal blocks and connectors.
  • Incorrect components or orientation: Check approved BOM information, polarity, package compatibility, and placement before and during assembly.
  • Contamination and corrosion: Control cleaning, handling, and specified protective processes to reduce leakage and corrosion risks.

Terminal blocks deserve particular attention because field wiring may be connected, disconnected, or adjusted repeatedly during the equipment’s service life.

For security monitoring assemblies exposed to humidity, the cleaning requirements, connector protection, and any conformal coating specifications should be established before production.

Preventing manufacturing defects requires process control, while confirming workmanship requires inspection. Neither activity alone guarantees long-term reliability without appropriate product-level validation.

How Are Security Monitoring PCBs Inspected and Tested for 24/7 Operation?

Security monitoring PCB testing must verify bare-board electrical integrity, component assembly quality, alarm input and output functions, communication interfaces, and power stability. Each test addresses a different type of failure, so the inspection plan should follow the customer’s approved PCB and functional requirements.
security monitoring PCB, https://www.bestpcbs.com/blog/2026/11/security-monitoring-pcb/

EBest Circuit can support the following inspection and testing steps:

  • Bare PCB electrical testing: Checks for unintended open and short circuits against the approved netlist. Specified dimensional, hole-quality, and controlled-impedance checks can be included when required.
  • Solder Paste Inspection (SPI): Verifies solder paste deposition before component placement, helping identify insufficient or excessive paste and printing misalignment.
  • Automated Optical Inspection (AOI): Detects selected visible soldering defects, missing components, placement errors, and incorrect component orientation.
  • X-ray inspection: Evaluates inaccessible solder joints, including suitable BGA and bottom-terminated packages where hidden-joint inspection is required.
  • ICT or flying probe testing: Identifies selected electrical and assembly faults when suitable test access and an approved test program are available.
  • Alarm input testing: Verifies normal, triggered, restored, open-circuit, and short-circuit conditions for applicable supervised alarm channels.
  • Output and communication testing: Checks relay operation under specified loads and verifies Ethernet or RS-485 communication against the approved test procedure.
  • Power and recovery testing: Measures the required power rails and current consumption, and checks startup, reset, and recovery after specified supply interruptions.
  • Environmental and continuous-operation testing: Where required, evaluates operation under defined temperature, humidity, loading, or extended-running conditions.

Each functional test must have defined inputs, expected results, and pass/fail criteria. For example, an alarm input test should specify the electrical state applied to the channel and the corresponding response expected from the controller.

Passing AOI, electrical testing, and short functional tests does not automatically prove years of uninterrupted operation. 24/7 reliability requires suitable equipment-level qualification, with operating conditions and test duration established according to the actual application.

What Custom Security Monitoring PCB Manufacturing and Assembly Services Does EBest Circuit Offer?

EBest Circuit provides custom multilayer PCB fabrication, SMT/THT assembly, component sourcing, and project-specific testing for security monitoring equipment. Manufacturing follows the customer’s approved Gerber files, BOM, assembly drawings, and acceptance requirements.

Our services include:

  • Custom PCB fabrication: Single-sided, double-sided, and multilayer FR-4 PCBs, including high-Tg materials and controlled-impedance constructions where applicable.
  • SMT assembly: Placement and soldering of microcontrollers, communication ICs, power devices, protection components, and surface-mounted passive components.
  • THT assembly: Installation of terminal blocks, relays, connectors, and other through-hole components.
  • Component sourcing: Full-turnkey, partial-turnkey, and customer-consigned assembly arrangements based on approved component specifications.
  • Manufacturing preparation: Review of PCB panelization, component footprints, connector orientation, soldering accessibility, and assembly documentation.
  • Inspection and functional testing: Bare PCB electrical testing, assembly inspection, and customer-defined testing according to the agreed project scope.
  • Prototype and production manufacturing: Support for engineering samples, pilot quantities, and repeat production orders.

Security monitoring boards frequently combine fine-pitch SMT components with mechanically loaded through-hole connectors. Coordinating these different assembly requirements helps prevent footprint conflicts, soldering problems, and unnecessary rework.

Before manufacturing, EBest Circuit offers a free DFM check to review fabrication and assembly feasibility, including trace spacing, hole structures, component footprints, and production accessibility.

Which Quality Certifications and IPC Standards Support Security Monitoring PCB Manufacturing?

ISO 9001 quality management and applicable IPC workmanship standards provide an important quality framework for security monitoring PCB manufacturing. They support controlled production documents, inspection criteria, corrective actions, and repeatable manufacturing processes.

EBest Circuit lists ISO 9001:2015 among its quality management certifications. The current certificate, covered manufacturing location, and applicable scope should be confirmed during project qualification.

Relevant requirements include:

  • ISO 9001: Quality management requirements for controlled processes, documented information, supplier management, and corrective actions.
  • IPC-A-600: Acceptability criteria for bare PCBs, including specified workmanship and structural characteristics.
  • IPC-A-610: Acceptability criteria for electronic assemblies, including component placement and solder-joint workmanship.
  • IPC-6012: Performance and qualification requirements for rigid PCBs when specified by the customer.

The applicable IPC revision, acceptance class, and inspection requirements should be established before production.

A manufacturing quality certificate does not automatically establish finished-product compliance. Security monitoring equipment may require separate electrical safety, EMC, environmental, or application-specific certification.

For projects requiring formal quality documentation, EBest Circuit can review the specified inspection records, acceptance criteria, and applicable certificate scope before order confirmation.

What Is the Lead Time for Security Monitoring PCB Manufacturing and Assembly?

Security monitoring PCB lead time depends on the layer count, fabrication specifications, component availability, assembly complexity, and testing requirements. Bare-board fabrication and PCBA assembly are separate production stages and should not be treated as one guaranteed delivery period.

EBest Circuit provides the following reference schedules for standard FR-4 prototype fabrication and general PCBA assembly.

Production Stage Reference Lead Time Applicable Conditions
2-Layer FR-4 PCB Prototype 8 days Standard bare-board fabrication
4-Layer FR-4 PCB Prototype 10 days Standard bare-board fabrication
8-Layer FR-4 PCB Prototype 12 days Standard bare-board fabrication
PCBA Assembly Approximately 1 week General assembly reference; material and process conditions must be confirmed

Standard FR-4 prototype references apply to conventional specifications, including a 0.4–1.6 mm board thickness, H/H or 1 oz copper, lead-free HASL, green solder mask, and standard trace and hole requirements.

Special materials, ENIG finishes, controlled impedance, fine-line fabrication, complex through-hole assembly, and additional testing may affect the schedule.

For turnkey security monitoring PCB projects, the complete lead time must also account for material procurement, fabrication, assembly, testing, and shipping. Some activities can overlap, but production cannot proceed until the required materials and approved documents are available.

Send the Gerber files, BOM, order quantity, required delivery date, delivery location, and testing requirements to receive a project-specific production schedule.

How Much Does Security Monitoring PCB Manufacturing and Assembly Cost?

Security monitoring PCB manufacturing cost depends on PCB construction, component selection, assembly operations, testing requirements, and production quantity. A simple alarm input board will generally have a different cost structure from a multilayer controller with several communication interfaces and relay outputs.

The main cost factors are:

  • PCB construction: Additional layers, special via structures, and controlled-impedance requirements increase fabrication complexity.
  • Board size and panelization: Efficient panel layouts reduce material waste and unnecessary manufacturing handling.
  • Copper thickness and materials: Heavy copper, high-Tg laminates, and nonstandard materials may increase processing costs.
  • Component selection: Specialized communication ICs, connectors, relays, and protection devices affect sourcing costs and availability.
  • Assembly operations: Double-sided SMT, through-hole soldering, programming, and coating require additional processes.
  • Testing scope: Custom test fixtures, extended operation tests, and specific inspection documentation affect the total project cost.

Several manufacturing decisions can help reduce unnecessary expenses:

  • Use standard FR-4 materials and surface finishes when they satisfy the electrical and environmental requirements.
  • Optimize PCB dimensions and panelization without compromising mounting or connector accessibility.
  • Confirm component availability before BOM release to reduce shortages and unplanned substitutions.
  • Avoid unnecessary layer counts or special processes when standard fabrication can meet the specifications.
  • Define functional-test requirements before production to reduce late fixture changes and repeated testing work.

For example, reducing an eight-layer PCB to six layers may lower bare-board fabrication cost, but only if the modified stackup still satisfies the routing, impedance, and mechanical requirements.

EBest Circuit can review PCB files and the BOM to identify feasible manufacturing options before quotation. Any proposed design or component changes require customer approval.

Why Choose EBest Circuit for Factory-Direct Security Monitoring PCB Manufacturing?

EBest Circuit helps security monitoring equipment manufacturers simplify production coordination, identify manufacturability problems early, and maintain consistent specifications across repeat orders.

Our factory-direct manufacturing services provide the following support:

  • Fewer supplier handoffs: PCB fabrication, component procurement, assembly, and agreed testing can be coordinated through one manufacturing provider, reducing communication gaps between different suppliers.
  • Earlier identification of manufacturing risks: Our free DFM check helps detect fabrication constraints, footprint mismatches, and assembly problems before production release.
  • Controlled prototype-to-production transition: Approved PCB files, BOM revisions, assembly instructions, and testing requirements provide a consistent manufacturing baseline for repeat orders.
  • Reduced risk of unauthorized substitutions: Alternative components and materials are reviewed against customer-approved specifications before implementation.
  • Clearer quality acceptance: Applicable inspection records and agreed functional-test results help customers evaluate completed assemblies against defined requirements.
  • Confidentiality protection: NDA arrangements can be established before customers provide proprietary circuit information or security hardware documentation.

For security monitoring equipment, an acceptable first prototype is only the beginning. Subsequent production orders must maintain the correct circuit revision, approved components, and required inspection criteria.

Working directly with EBest Circuit gives customers one manufacturing contact for technical clarification, production changes, and repeat-order coordination, while keeping responsibility for system architecture and firmware requirements clearly defined.

Security Monitoring PCB Manufacturing and Assembly Case Study

An EBest Circuit manufacturing project involved an 8-layer FR-4 PCB for surveillance and security equipment used in commercial and residential monitoring applications. The project provides a relevant reference for multilayer security monitoring PCB fabrication.

Project Background

The security equipment required a multilayer PCB to accommodate dense circuitry and signal transmission. The board construction needed to meet the specified material, thickness, copper, and surface-finish requirements while remaining suitable for subsequent electronic assembly.

Project Requirements and Challenges

The recorded PCB specifications included:

  • PCB Layers: 8 layers
  • Material: FR-4, Tg 170°C
  • Finished Thickness: 1.3 mm ±10%
  • Inner-Layer Copper: 1 oz
  • Outer-Layer Copper: 1 oz
  • Surface Finish: ENIG, specified gold thickness of 1 μin
  • Solder Mask: Blue
  • Silkscreen: White
  • Delivery Format: Panelized PCB

The main manufacturing considerations involved fitting the required eight-layer construction within the specified thickness, maintaining multilayer registration, and applying the required copper and surface-finish specifications.

EBest Circuit’s Manufacturing Approach

The manufacturing specification established the approved high-Tg FR-4 material, copper weights, finished thickness, ENIG surface finish, and panel format.

For this multilayer construction, lamination, layer registration, hole plating, dimensional control, and surface finishing were the relevant fabrication processes.

Project Results

The documented project output was a panelized 8-layer FR-4 PCB for security equipment, with the construction and manufacturing specifications described above.

The available project information establishes the application and PCB specifications but does not include separately verified PCBA functional-test results, production yield, or field-reliability measurements. The project therefore serves as a multilayer PCB manufacturing reference rather than evidence of complete-system reliability qualification.

FAQs About Security Monitoring PCB Manufacturing and Assembly

Q1: Can EBest Circuit sign an NDA before receiving confidential PCB design files?

A1: Yes. NDA arrangements can be discussed and signed before confidential Gerber files, BOM information, schematics, or proprietary assembly documents are exchanged. Customers can specify confidentiality and document-handling requirements in the agreement.

Q2: Can customer-supplied components be used for security monitoring PCB assembly?

A2: Yes. Customer-consigned components can be used under an agreed assembly arrangement. Supplied materials should include approved manufacturer part numbers, quantities, packaging information, and relevant handling instructions. Incoming material status is reviewed before production.

Q3: What happens if an approved BOM component becomes unavailable?

A3: A replacement component must be reviewed and approved before use. The review should cover electrical ratings, package dimensions, operating temperature, and relevant functional requirements. Approved substitutions are recorded against the applicable BOM revision.

Q4: Can PCB design revisions be introduced after prototype production?

A4: Yes. Customers should provide the revised PCB data, updated BOM, assembly changes, and modified testing requirements. The new manufacturing package is reviewed before the next production release. Changes introduced after production begins may affect materials, scheduling, and cost.

Q5: Can individual PCBA serial numbers be added for traceability?

A5: Serial-number labeling and corresponding production records can be arranged when specified. Customers should define the numbering format, label position, identification method, and required traceability information before manufacturing.

Q6: Can customer firmware be programmed during PCB assembly?

A6: Firmware programming support can be arranged using approved firmware files, compatible programming equipment, instructions, and verification procedures. Firmware version control, security credentials, and access permissions should be confirmed before production.

Q7: Can conformal coating be applied to security monitoring PCB assemblies?

A7: Conformal coating can be arranged where required for protection against moisture or contamination. Customers should specify the coating material, masking areas, thickness requirements, and acceptance criteria. Connectors, test points, and electrical contacts may require masking.

Q8: How are security monitoring PCB assemblies packaged for international shipping?

A8: Packaging requirements can address ESD protection, mechanical damage, connector protection, and moisture-sensitive components. ESD bags, protective trays, moisture-barrier packaging, or individual labeling should be specified before shipment.

Q9: Can inspection documents be supplied with a PCB order?

A9: Inspection documentation can be arranged according to the agreed manufacturing requirements. Depending on the project, documents may include electrical-test records, dimensional inspection reports, certificates of conformity, or specified assembly-test results. Required documents should be identified before production.

Request a Quote for Custom Security Monitoring PCB Manufacturing and Assembly

Looking for a factory-direct security monitoring PCB manufacturer that can handle custom PCB fabrication, SMT/THT assembly, and quality testing? EBest Circuit provides manufacturing support for intrusion detection controllers, alarm monitoring boards, perimeter security equipment, and custom security communication PCBs.

Send your Gerber files, BOM, order quantity, required delivery date, delivery location, and testing requirements to sales@bestpcbs.com. EBest Circuit offers a free DFM check to identify potential fabrication and assembly issues before production and prepare a quotation based on your approved specifications.
Ethernet PCB Routing Guide: From PHY to RJ45

November 11th, 2026

Start Ethernet PCB routing by dividing the interface into two parts: the digital link from the MAC to the PHY, and the cable-facing differential pairs from the PHY toward the RJ45. Get the PHY vendor’s layout guide and the fabricator’s stackup before drawing traces. Route the cable pairs as balanced transmission lines, keep their return paths intact where the design calls for a reference plane, and preserve the isolation boundary specified by the connector and system design.

Evaluation PCB with an RJ45 connector and nearby Ethernet PHY region
Illustrative Ethernet board. Use the selected parts and their drawings to verify the actual placement and pinout.

ethernet pcb routing

Assign each net to its electrical interface first. The media access controller (MAC) handles Ethernet frames; the physical-layer transceiver (PHY) converts data into the signals used by the medium. The medium-dependent interface (MDI) is the PHY’s cable-facing side. It is not the MAC interface and does not use the same length-matching rules.

Use a hypothetical industrial controller with a 1000BASE-T port as a running example. Its connector sits at the enclosure edge, while a switch-mode regulator competes for nearby space. Moving the PHY close to the connector is useful only if the move also leaves a clean, balanced path and preserves the isolation and protection layout.

ethernet phy pcb design layout checklist

Convert the vendor’s electrical requirements into separate CAD checks before routing. Use the exact PHY and magnetics documentation. For example, Texas Instruments’ SNLA387 uses 100 Ω differential routing for MDI traces; it is not a universal width, spacing, or skew limit.

Design item Set from Check before release
MDI impedance, Ω PHY guide and stackup Width, gap, layer
Intra-pair skew Selected PHY guide Delay and transitions
Digital timing MAC and PHY timing Clock and data delays
Isolation keepout Parts and system spec Planes and copper

ethernet differential pair impedance

Set differential impedance using the trace width and gap together with copper thickness, dielectric thickness and properties, and the reference layer. Moving an apparently identical pair to a different layer changes that geometry. Ask the fabricator for a matched stackup and obtain approval before substituting material or dielectric thickness. Use an appropriate controlled-impedance coupon where specified; a coupon pass checks its test structure, not every discontinuity on the port.

ethernet differential pair length matching

Check the two conductors of each pair first. Follow the PHY guide for any separate pair-to-pair requirements; do not impose one total-length target on unrelated nets. For illustration, if a stackup gives an assumed effective delay of 6 ps/mm, a 3 mm mismatch corresponds to 18 ps before accounting for different via structures or layers. That is not a pass limit. Compare the actual extracted delay and path geometry against the selected device’s requirements.

Fix an asymmetric breakout or transition before adding a long meander. A trace can have the right CAD length and still encounter a different reference plane or more vias than its partner. A small symmetric change is often easier to verify than a large correction near the connector.

ethernet magnetics layout

Choose discrete magnetics or an integrated magnetic jack before fixing the PHY position. Both can work; the decision depends on the approved circuit, footprint, signal path, and isolation needs.

Option Useful when Verify
Discrete magnetics Placement flexibility matters Extra route and keepout
Integrated jack Edge area is limited Pinout and shield

Integrated vs discrete does not change the need to read center-tap and termination guidance. Confirm the exact transformer ratio, approved pin mapping, and isolation requirements. Do not infer compatibility from identical connector footprints.

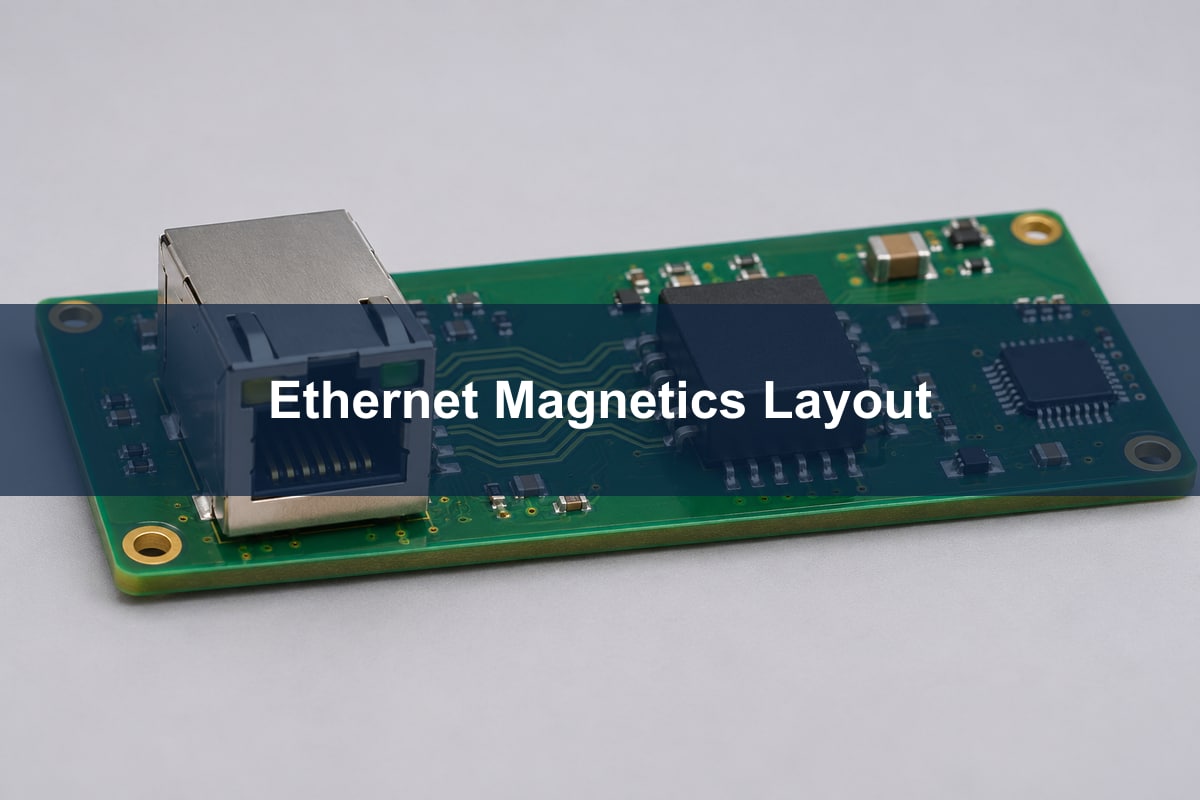
Discrete Ethernet magnetics package next to a shielded RJ45 jack
Illustrative discrete-magnetics layout. Check the space for copper keepouts and protection before committing to placement.

rj45 pcb layout

Treat the connector area as a system boundary. Place the connector to suit the enclosure, and follow the reference design for the specified separation between circuit ground and chassis or shield. Do not carry an ordinary ground pour across a required isolation keepout to make an otherwise shorter route. Plan the ESD discharge path and protection placement with the connector and PHY documentation; a short route on a drawing can still return transient current through the wrong area.

rmii pcb layout guidelines

RMII is a digital MAC-to-PHY interface, not a method for routing the cable pairs. For a 10/100 design using RMII, identify the clock source, then review the clock and associated signals against both device documents. Do not apply the MDI differential rule to RMII signals. The gigabit example normally needs a different MAC interface, such as RGMII when supported. Check its timing and configured clock delays separately; changing PHY mode changes which design rules apply.

ethernet pcb routing guidelines

Release the port only after you can show that the layout meets the selected part requirements and the board works under the intended conditions. In the controller example, first route the MDI channel away from the regulator’s noisy node. If layer changes are necessary, keep pair transitions balanced and provide the return path required by the reference stackup, without bridging the connector’s isolation boundary.

  1. Cross-check schematic and footprint against the PHY, transformer, and jack documents. Confirm polarity, center taps, digital interface mode, and shield connection.
  2. Review the released artwork and fabricator stackup for impedance, pair transitions, plane continuity, and keepouts. Resolve any deviations before order release.
  3. On the first article, confirm power, clock, reset and link negotiation at the intended modes. Transfer sustained traffic, check error counters, and repeat with the intended cable, supply conditions and enclosure. A link LED alone does not establish margin.
  4. Where required, run the specified physical-layer and EMC tests. If errors correlate with converter loading, review coupling and return paths before changing pair length.

FAQ

Are vias prohibited in Ethernet differential pairs?

No universal rule prohibits them. Follow the PHY guidance, minimize unnecessary transitions, use comparable transitions on both conductors, and preserve the return path as required. Inspect the actual transition, not just the via count.

Do all Ethernet MDI routes use two pairs?

No. Conventional 100BASE-TX uses two pairs, while 1000BASE-T uses four. Confirm the PHY mode and connector mapping rather than copying a two-pair layout into a gigabit design.

Can I swap pair polarity or pair positions?

Do not assume so. Some devices can compensate for selected swaps, but support varies with device, interface, and mode. Check the exact PHY documentation and the magnetics pinout.

Can I omit magnetics between two devices on the same board?

Only if the selected devices and system requirements support the chosen topology. Follow a device-specific transformerless design note, and do not assume a board-to-board topology is suitable for a cable port.

Can power and data share the same connector?

Power over Ethernet does this with a compatible circuit and magnetics. It changes the connector, thermal and protection requirements. Do not repurpose an ordinary design without reviewing the power path and its applicable requirements.

Do I need a four-layer PCB?

Layer count alone is not a qualification test. Verify the target impedance, routing density, ground references and isolation boundaries in the proposed stackup. Use the selected device guide to decide whether the layout is credible.

Is this guide for 10G or single-pair Ethernet?

No. The examples cover common copper 10/100/1000 ports, not single-pair, 10G or serial backplane interfaces. Use the specifications and layout documents for the intended PHY and medium.

What should I send for a stackup review?

Provide the current layer count, impedance targets, routing layers, copper thickness, and board outline. Include the relevant PHY and connector part numbers and separate any additional timing constraints from fabrication tolerances. See the related microstrip design guide.

References

For a board fabrication review, send the proposed stackup, differential impedance requirements, and current fabrication revision to Best Technology at sales@bestpcbs.com.

Network Monitoring PCB Design, Prototyping & Assembly | Free DFM Check

November 11th, 2026

Network monitoring PCB manufacturing requires accurate impedance control, reliable assembly, and stable operation under continuous network traffic. Incorrect trace geometry, connector misalignment, or soldering defects may cause communication errors, unstable links, and repeated prototype failures. How can you identify these manufacturing risks before they affect your project schedule?

EBest Circuit provides network monitoring PCB fabrication, prototyping, component sourcing, and SMT/THT assembly. With 20 years of PCB manufacturing experience, standard FR4 manufacturing from 1–10 layers, and special processes supporting up to 32 layers, we help customers meet demanding manufacturing requirements. Our free DFM check identifies potential manufacturability concerns before fabrication.

network monitoring PCB, https://www.bestpcbs.com/blog/2026/11/network-monitoring-pcb/

What Are Network Monitoring PCBs Used For?

Network monitoring PCBs are used in equipment that captures, measures, analyzes, and records network activity, including traffic volume, packet transmission, link status, communication errors, and network performance.

Unlike ordinary network device PCBs, network monitoring boards may need to support continuous data acquisition, accurate event timing, and reliable operation under sustained traffic loads.

Common applications include:

  • Network traffic monitoring equipment: Captures network traffic for bandwidth analysis, performance monitoring, and fault investigation.
  • Packet capture and protocol analyzers: Connects Ethernet interfaces, processors, and memory circuits for packet inspection and recording.
  • Network TAP equipment: Provides connections and monitoring paths for observing network traffic.
  • Optical network monitoring devices: Integrates SFP/SFP+ interfaces, management circuits, and processing modules for optical link monitoring.
  • Industrial network diagnostic systems: Monitors Ethernet connectivity, communication errors, and equipment status in industrial networks.

A monitoring board using a 100 Mb/s Ethernet interface does not have the same routing and signal-integrity requirements as a multiport 10 Gb/s packet analyzer.

The PCB stackup, materials, routing density, and inspection requirements should match the actual interface speed and equipment configuration.

What Are the Key Design Requirements for Network Monitoring PCBs?

Network monitoring PCB design must establish measurable impedance, signal timing, power, thermal, and mechanical requirements before fabrication. The selected Ethernet PHY, MAC, or transceiver specification determines the applicable electrical limits.

network monitoring PCB, https://www.bestpcbs.com/blog/2026/11/network-monitoring-pcb/

The following values are engineering references for specific Ethernet PHY interfaces, not universal rules for every network monitoring PCB.

Design Parameter Engineering Reference Application and Verification
Ethernet MDI Differential Impedance 100 Ω Common PHY-to-magnetics interface requirement
Ethernet MDI Single-Ended Impedance 50 Ω Referenced to the specified ground plane
SGMII Differential Impedance 100 Ω Applicable SGMII PHY interfaces
SGMII Intra-Pair Skew Less than 5 ps Example requirement for compatible PHY devices
RGMII Single-Ended Impedance 50 Ω Applicable PHY-to-MAC interface
RGMII TX Data-Group Skew Less than 11 ps Example PHY-specific data-lane matching requirement
RGMII RX Data-Group Skew Less than 11 ps Example PHY-specific data-lane matching requirement
RGMII Trace Length Below 50.8 mm preferred Example PHY recommendation; device-specific limits apply

Ethernet MDI, SGMII, and RGMII require different routing rules. The impedance and timing limits for one interface should not be automatically applied to another. High-speed SFP+ links must follow their specific transceiver and channel requirements.

PCB stackup construction directly affects whether the routing targets can be achieved. Trace width, spacing, copper thickness, dielectric thickness, and reference-plane position must be evaluated together.

For example, a 100 Ω differential pair does not have a fixed trace width across different FR4 stackups. Changing copper thickness or dielectric configuration may require different conductor dimensions.

Other important design considerations include:

  • Power integrity: Verify supply voltage tolerances, decoupling placement, and current requirements against the selected IC specifications.
  • Clock stability: Confirm oscillator accuracy, reference-clock routing, and timing requirements for the selected monitoring architecture.
  • EMI/ESD protection: Design shielding, grounding, return paths, and interface protection according to the equipment’s applicable requirements.
  • Thermal management: Keep processor and interface-component temperatures within their specified operating limits.
  • Mechanical integration: Confirm board thickness, mounting-hole positions, connector dimensions, and enclosure clearances.

For monitoring equipment that records precise event timestamps, clock accuracy and timing behavior require appropriate system-level validation.

Controlled-impedance PCB manufacturing supports signal integrity, but it does not independently guarantee packet-capture accuracy or timestamp precision.

What Are the Common Network Monitoring PCB Design and Manufacturing Challenges and Solutions?

Network monitoring equipment manufacturers frequently encounter unstable high-speed links, limited routing space, connector assembly problems, and inconsistent production results. EBest Circuit addresses manufacturing-related risks through engineering review, appropriate fabrication processes, and assembly inspection.

Challenge: Network links become unstable after prototype assembly.

Unexpected link drops, excessive communication errors, or failure to establish the required connection speed may result from impedance discontinuities, connector defects, soldering problems, or circuit-level faults.

Our solution: We review the approved stackup, critical trace geometry, via structures, and connector requirements before fabrication. Controlled-impedance measurements and relevant inspections can be arranged according to the project specification. Assembly-related defects are addressed through the agreed inspection process, while complete link performance is verified through customer-defined functional testing.

Challenge: High-density components exceed conventional routing limits.

FPGAs, network processors, memory devices, and fine-pitch ICs may require dense routing around component pads. Insufficient spacing or inappropriate drilling structures can prevent successful PCB fabrication.

Our solution: EBest Circuit evaluates the proposed routing density, copper weight, drill structure, and layer count. Our special FR4 processes support 3/3 mil line/space and 0.10 mm laser microvias under applicable manufacturing conditions. We also assess whether conventional multilayer construction can meet the design requirements without unnecessary HDI processing.

Challenge: Network connectors do not align with the equipment enclosure.

RJ45 connectors, SFP/SFP+ cages, and board-edge interfaces require accurate mechanical positioning. Incorrect board dimensions or connector placement may cause assembly problems or mechanical stress.

Our solution: We check board outlines, mounting-hole dimensions, connector footprints, and relevant tolerances against the supplied manufacturing drawings. Connector positioning and soldering quality can be included in the assembly inspection plan.

Challenge: Prototype performance changes during repeat production.

Material substitutions, PCB revisions, component changes, and soldering-process variations may affect production consistency.

Our solution: We coordinate production using the customer’s approved PCB files, BOM revisions, assembly requirements, and inspection criteria. Proposed changes are reviewed before implementation, helping maintain a consistent manufacturing configuration.

How Are Network Monitoring PCB Prototypes Fabricated and Assembled?

Network monitoring PCB prototyping follows a sequence of engineering review, bare-board fabrication, component assembly, inspection, and functional verification. Each stage helps identify potential problems before the design enters volume production.

Step 1 — Review PCB and Assembly Files

The manufacturing review covers Gerber or ODB++ files, drill data, PCB stackup, BOM, pick-and-place files, and assembly drawings.

Our free DFM check examines trace spacing, drilling feasibility, stackup requirements, solder mask openings, and relevant assembly clearances.

Manufacturing questions are confirmed with the customer before production release.

Step 2 — Fabricate the Bare PCB

PCB fabrication follows the approved material, copper weight, layer structure, drilling requirements, and surface finish.

Depending on the construction, manufacturing includes inner-layer imaging and etching, lamination, drilling, metallization, outer-layer processing, solder mask application, and surface finishing.

For controlled-impedance designs, the required conductor geometry and stackup are confirmed before fabrication.

Step 3 — Inspect the Fabricated PCB

Electrical testing checks continuity and isolation against the approved netlist.

AOI, dimensional inspection, and additional specified measurements help identify manufacturing defects before component assembly.

Step 4 — Verify Components and Prepare Assembly

The approved BOM is checked for manufacturer part numbers, package compatibility, quantities, and component availability.

Stencil preparation and placement-program verification are completed before SMT production. Any proposed component substitution requires customer approval.

Step 5 — Perform SMT Assembly

Solder paste is applied to the appropriate pads, followed by component placement and controlled reflow soldering.

SPI and AOI are used according to the assembly inspection requirements. X-ray inspection can be arranged for suitable packages with hidden solder joints.

Step 6 — Complete THT Assembly

RJ45 connectors, headers, and other through-hole components are installed using the appropriate soldering process.

Connector alignment, mechanical positioning, and solder-joint quality are checked according to the assembly requirements.

Step 7 — Program and Functionally Test the PCBA

When the required firmware, fixtures, and test procedures are available, functional verification may include:

  • Ethernet link establishment at the specified interface speed.
  • Port communication and packet-transfer testing.
  • Power-rail voltage and current measurements.
  • Clock or timestamp verification against a defined reference.
  • Sustained operation under specified traffic loads.

Step 8 — Perform Final Inspection and Shipment Preparation

The approved PCB revision, BOM, assembly condition, identification requirements, and agreed inspection records are checked before packaging.

Prototype approval should be based on the customer’s measurable electrical, mechanical, and functional acceptance criteria. A successfully assembled PCB is not automatically a fully qualified network monitoring system.

What Network Monitoring PCB Manufacturing and Assembly Services Does EBest Circuit Provide?

EBest Circuit supports network monitoring PCB projects from design-for-manufacturing review to finished PCBA delivery. Our manufacturing services can be selected according to the customer’s approved design, component requirements, and production plan.

  • PCB Design for Manufacturability Support: Review stackup feasibility, controlled impedance, fine-line routing, drilling, solder mask, and assembly requirements.
  • Custom PCB Fabrication: Manufacture FR4 multilayer boards and suitable HDI constructions according to approved production files.
  • PCB Prototyping: Support engineering samples and pilot builds before volume production.
  • Component Sourcing: Procure approved Ethernet PHYs, processors, memory devices, passive components, and network interface connectors.
  • SMT and THT Assembly: Assemble surface-mount and through-hole components, including mixed-technology PCBA.
  • Programming and Testing Support: Arrange applicable inspection, firmware programming, and customer-defined functional testing when the required resources are available.

For customers requiring both PCB fabrication and assembly, these services can be coordinated through a single manufacturing project.

The standard free DFM check focuses on the manufacturability of customer-provided designs. Original circuit development or complete PCB layout design requires separate project confirmation.

What Are Our Network Monitoring PCB Manufacturing and Assembly Capabilities?

EBest Circuit supports FR4 PCB manufacturing from standard multilayer boards to high-density special-process constructions. Our capabilities help engineers evaluate the feasibility of network monitoring PCBs with dense interfaces, fine-pitch packages, and multilayer routing.

Manufacturing Capability Standard Process Special Process
FR4 Layer Count 1–10 layers 10–32 layers
Inner-Layer Line/Space, 0.5–1 oz Copper 4/4 mil 3/3 mil
Outer-Layer Line/Space, 1 oz Copper 4/4 mil 3/3 mil
Outer-Layer Line/Space, 2 oz Copper 8/8 mil 6/6 mil
Laser Microvia Diameter 0.10 mm 0.10 mm, subject to construction review
Minimum Finished Mechanical Hole 0.20 mm 0.15 mm
Maximum Through-Hole Aspect Ratio 8:1 10:1
PTH Hole Diameter Tolerance ±3 mil ±2 mil
NPTH Hole Diameter Tolerance ±2 mil ±1 mil

Manufacturing limits must be evaluated as a complete PCB construction. Minimum line spacing, minimum finished hole size, maximum layer count, and maximum aspect ratio are not automatically achievable together.

Actual feasibility depends on copper thickness, finished board thickness, laminate properties, layer stackup, plating requirements, drilling structures, and other process conditions.

For high-density network monitoring PCBs, the approved design should be evaluated against these combined requirements before fabrication.

Assembly feasibility is assessed separately according to component packages, connector geometry, soldering requirements, and inspection access.

How Do We Ensure Network Monitoring PCB Quality and Reliability?

Network monitoring PCB quality is verified through bare-board inspection, PCBA workmanship checks, and customer-defined functional testing. These methods address different manufacturing and operational risks.

network monitoring PCB, https://www.bestpcbs.com/blog/2026/11/network-monitoring-pcb/

Bare-Board Quality Control

  • AOI: Identifies visible conductor-pattern defects.
  • Electrical Testing: Checks continuity and isolation against the approved PCB netlist.
  • Impedance Measurement: Verifies specified controlled-impedance structures when required.
  • Dimensional Inspection: Checks board outlines, mounting holes, and other critical dimensions.

PCBA Quality Control

  • SPI: Evaluates solder-paste deposits before component placement.
  • AOI: Identifies visible placement and soldering defects.
  • X-ray Inspection: Examines hidden joints where required.
  • Connector Inspection: Checks mechanical alignment and soldering condition.

Network Monitoring Functional Verification

A monitoring device may require testing at its intended link speed, port configuration, and operating load.

For example, a multiport monitoring PCBA can be evaluated for link establishment, communication errors, supply stability, and sustained operation under the specified traffic conditions.

When event timestamping is required, the test plan should identify the reference source, measurement method, and acceptable timing error.

Bare-board electrical testing cannot independently verify packet-capture accuracy, timing precision, or complete network monitoring performance. These characteristics require appropriate assembled-system validation.

What Quality Certifications Support Our Network Monitoring PCB Production?

EBest Circuit maintains quality management certifications that support production control, manufacturing traceability requirements, and supplier qualification.

Our quality certification portfolio includes:

  • ISO 9001:2015: General quality management covering production processes, inspection, and corrective actions.
  • ISO 13485:2016: Medical device quality management for applicable manufacturing activities.
  • IATF 16949: Automotive quality management for applicable electronics manufacturing programs.
  • AS9100D: Aerospace quality management for applicable high-reliability manufacturing requirements.

For commercial and industrial network monitoring PCB projects, ISO 9001 is the primary general quality-management reference. Industry-specific certifications may be relevant to medical, automotive, or aerospace applications.

Customers can request applicable certificate copies and verify the certificate holder, manufacturing site, scope, and validity before supplier approval.

Network Monitoring PCB Prototyping and Assembly Case Study

A compact Ethernet traffic monitoring module illustrates how PCB manufacturing and assembly requirements can be evaluated before prototype production.

The following is an engineering application example using representative design requirements.

Project Background

Consider a compact network monitoring module integrating Ethernet PHY circuitry, processing components, memory, and network connectors.

The proposed construction uses a 4-layer FR4 PCB with a finished thickness of 1.6 mm, 1 oz outer copper, and ENIG surface finishing.

Project Requirements and Challenges

The PCB requires controlled-impedance routing, suitable layer-stackup design, accurate connector positioning, and reliable SMT assembly.

The principal manufacturing concerns are maintaining the specified conductor geometry, confirming enclosure compatibility, and ensuring that the assembled PCB can be tested against the required communication functions.

Manufacturing Approach

The production review would confirm stackup, copper weight, trace spacing, drilled-hole requirements, solder mask openings, and connector dimensions.

For 1 oz outer copper, EBest Circuit supports 4/4 mil standard line/space and 3/3 mil special-process line/space, subject to the applicable manufacturing conditions.

After fabrication, bare-board electrical inspection and the agreed assembly inspection procedures would be performed.

Qualification Requirements

Prototype approval would require verification of PCB dimensions, electrical continuity, connector alignment, assembly quality, Ethernet link operation, and specified traffic or timing requirements.

The customer-defined test plan must establish the measurement methods and pass/fail limits before production release.

Why Choose EBest Circuit for Network Monitoring PCB Prototyping and Assembly?

With 20 years of PCB manufacturing experience, advanced FR4 fabrication, and integrated PCBA services, EBest Circuit supports network monitoring projects from prototype review to volume production.

  • 20 Years of Manufacturing Experience: Since 2006, we have supported complex PCB projects, helping customers address stackup, drilling, and fabrication challenges before production.
  • Advanced PCB Capabilities: We support up to 32 FR4 layers, 3/3 mil line/space, and 0.10 mm laser microvias under applicable conditions, meeting the needs of high-density monitoring equipment.
  • One-Stop PCB & PCBA Services: PCB fabrication, component sourcing, SMT/THT assembly, and testing support are coordinated through one supplier, simplifying procurement and production.
  • Certified Quality Management: Our certifications include ISO 9001, ISO 13485, IATF 16949, and AS9100D, supporting supplier qualification for applicable industrial and specialized applications.
  • Free DFM & Flexible Production: We identify manufacturability issues before fabrication and support prototypes, small batches, and volume production, helping customers reduce revisions and prepare for repeat orders.

EBest Circuit combines manufacturing capability, quality management, and assembly services to support reliable network monitoring PCB production.

What Is the Lead Time for Network Monitoring PCB Prototyping and Mass Production?

Network monitoring PCB lead time depends on layer count, materials, drilling requirements, controlled impedance, component availability, and assembly complexity.

For qualifying standard FR4 PCB prototype orders below 1 m², our reference manufacturing lead times are:

  • 2-layer PCB: Approximately 8 days.
  • 4-layer PCB: Approximately 10 days.
  • 6-layer PCB: Approximately 10 days.
  • 8-layer PCB: Approximately 12 days.
  • 10-layer and higher: Confirm according to the project specifications.

These standard reference schedules apply to qualifying FR4 designs with conditions such as 0.4–1.6 mm board thickness, 0.5 oz or 1 oz copper, lead-free HASL, line/space above 8 mil, and finished holes above 0.3 mm.

For projects meeting expedited-service requirements, faster prototype manufacturing may be available after engineering review and production scheduling.

Network monitoring PCBs requiring ENIG, fine-line routing, controlled-impedance inspection, HDI structures, or special materials may follow different manufacturing schedules.

PCBA assembly lead time must be calculated separately from bare-board fabrication. Component procurement, stencil preparation, programming, inspection, and functional testing must be included when establishing the complete production schedule.

International transportation and customs clearance are not included in manufacturing lead time unless specified in the quotation.

What Factors Affect Network Monitoring PCB Manufacturing and Assembly Costs?

Network monitoring PCB costs depend on PCB construction, materials, manufacturing processes, component procurement, assembly complexity, and testing requirements. The most effective cost reductions usually come from avoiding unnecessary manufacturing complexity while preserving the approved electrical and reliability requirements.

Practical cost-reduction methods include:

  • Avoid unnecessary HDI structures: Use conventional multilayer through-hole routing where component escape and signal-integrity requirements permit. Reserve laser vias and sequential lamination for designs that actually need them.
  • Use standard line/space where possible: If 4/4 mil routing satisfies the approved design, special 3/3 mil processing may not be necessary.
  • Select copper weight according to actual requirements: Choose 1 oz, 2 oz, or heavier copper based on current and thermal requirements. Increasing copper thickness unnecessarily may create tighter manufacturing constraints.
  • Choose a suitable surface finish: Select ENIG, OSP, or another approved finish based on assembly, storage, and application requirements rather than specifying a more expensive finish without a technical reason.
  • Review the BOM before prototype release: Identify unavailable, obsolete, or long-lead components. Evaluate alternative parts early, with customer engineering approval.
  • Improve panel utilization: Optimize the board outline and panel arrangement where manufacturing and mechanical constraints allow.
  • Compare prototype and volume pricing: Request separate quotations for prototype, pilot, and production quantities using consistent design revisions.
  • Define testing requirements early: Avoid unnecessary duplicate tests while retaining the inspections and functional checks needed for product acceptance.

Do not reduce PCB layer count or remove necessary reference planes solely to lower fabrication costs. For high-speed network monitoring equipment, these changes may increase signal-integrity problems and lead to additional redesign expenses.

A complete quotation should distinguish PCB fabrication, component purchasing, assembly, testing, tooling, and applicable one-time charges.

FAQs About Network Monitoring PCB Design, Prototyping and Assembly

Q1. Can an NDA be signed before sharing confidential network monitoring PCB files?

A1. Yes. A non-disclosure agreement can be discussed and signed before confidential Gerber files, BOMs, circuit drawings, or other proprietary technical information are exchanged. The confidentiality scope should be confirmed in advance.

Q2. What files are required for a network monitoring PCBA quotation?

A2. Provide Gerber or ODB++ files, drill data, fabrication drawings, BOM with manufacturer part numbers, pick-and-place files, assembly drawings, quantity, required delivery date, and delivery location. Include programming and functional test specifications where applicable.

Q3. Can customers supply their own network processors, PHYs, or connectors?

A3. Customer-supplied components can be evaluated for assembly. Part numbers, quantities, packaging, moisture sensitivity, and component condition should be confirmed before production.

Q4. What happens if an approved Ethernet PHY becomes unavailable?

A4. The component shortage should be identified during BOM review. Proposed alternatives require evaluation of pinout, electrical specifications, package compatibility, firmware dependencies, and qualification requirements. Substitutions must be approved before procurement or assembly.

Q5. Can different PCB revisions be manufactured under one project?

A5. Yes. Each PCB revision must be identified and controlled separately. The manufacturing files, BOM, assembly instructions, and inspection requirements must correspond to the correct approved revision.

Q6. Can customers provide firmware and functional test fixtures?

A6. Customer-provided firmware, programming instructions, and test fixtures can be evaluated. The required equipment, interfaces, and pass/fail criteria should be agreed before testing.

Q7. Can inspection records be provided with the PCBA shipment?

A7. Required inspection documentation can be discussed during quotation. Depending on the agreed scope, records may include bare-board electrical test results, impedance measurements, dimensional inspection, or assembly inspection reports.

Q8. Can PCB and component lot traceability be specified?

A8. Yes. Traceability requirements can be reviewed before production. Customers should specify the required PCB lot identification, component batch information, serial numbers, and related record requirements.

Q9. Can network monitoring PCBAs be supplied with special ESD protection?

A9. Packaging requirements can be specified according to ESD sensitivity, connector protection, mechanical handling, and transportation conditions. Special packaging arrangements should be confirmed during order preparation.

Q10. Can network monitoring PCBA orders be delivered in separate shipments?

A10. Split shipments can be discussed according to the production schedule. The quantity, inspection status, delivery destination, and shipping arrangements for each shipment must be agreed in advance.


Looking for a network monitoring PCB manufacturer that combines advanced PCB fabrication capabilities with assembly and production support? EBest Circuit provides custom FR4 PCB manufacturing, multilayer and HDI fabrication, SMT/THT assembly, component sourcing, and agreed testing services to support your project from prototypes to volume production.

Send your Gerber files, BOM, assembly drawings, quantity, required delivery date, and delivery location to sales@bestpcbs.com. Get a free DFM check and a project-specific quotation covering PCB manufacturing, assembly, testing requirements, and lead time.

Broadside Coupled Stripline Guide: Check Layer Offset

November 10th, 2026

Use broadside coupled stripline when routing the two conductors on adjacent inner layers solves a real routing constraint, and only if the pair still meets its impedance requirement at the fabricator’s expected layer offset. If side-by-side routing fits, start with edge-coupled stripline: moving both conductors onto one signal layer removes one critical dependency on alignment between two signal layers.

Suppose a 100 Ω differential link has to cross a narrow channel between connector escapes. The stacked pair fits in the layout, but the nominal impedance alone will not tell you whether it will work across production variation. Compare the two structures with the same channel requirements, then use a representative coupon and a separate launch check.

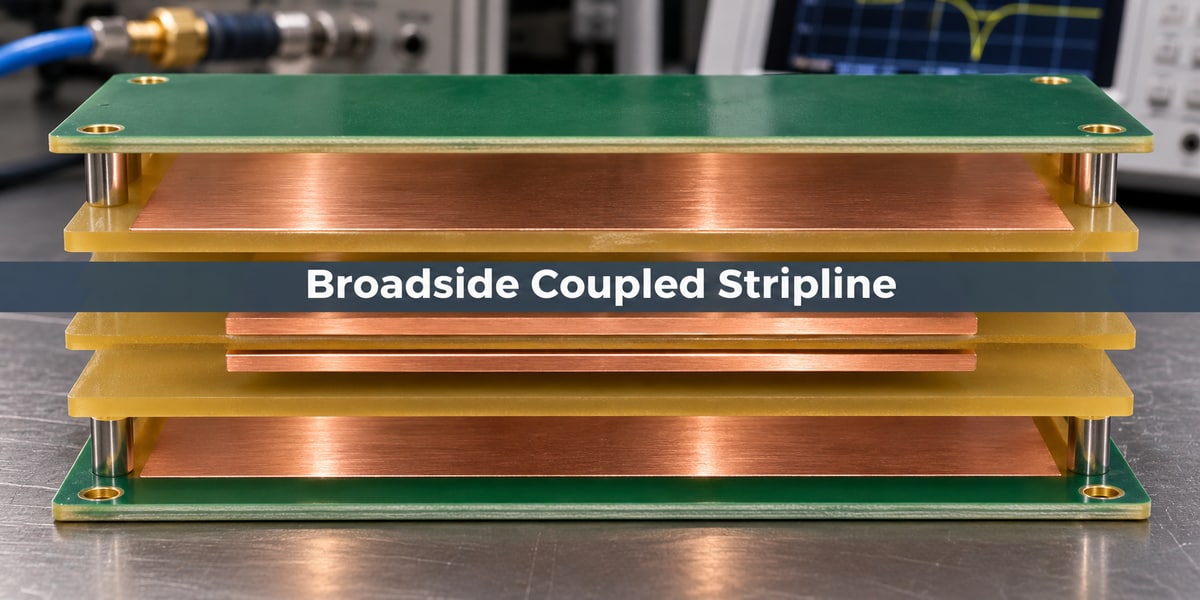
Physical-style demonstration of two internal copper strips stacked between reference planes
Illustration: The copper traces run one above the other; the artwork is not to scale and does not define a buildable stackup.

broadside coupled stripline

Broadside coupled stripline puts the pair’s two conductors on separate signal layers between reference planes. Their wide faces overlap through the dielectric, the insulating material between them. The pair is still a transmission line: the reference planes, the conductors, and the dielectric together determine its electrical behavior.

Draw the cross-section before routing. Identify both reference planes and both signal layers. If a plane sits between the two traces, it is not the intended directly coupled geometry. A pair routed in adjacent layers but far apart laterally also does not behave like an intentionally overlaid pair.

edge coupled vs broadside coupled

Edge coupling uses the narrow facing edges of two side-by-side tracks on the same layer; broadside coupling uses two tracks on different layers. Compare at the same target impedance, route length and channel requirements rather than comparing two unrelated calculator outputs.

Decision factor Edge coupled Broadside coupled
Routing width Two traces and one gap Can share a lateral corridor
Coupling input Etched same-layer gap Interlayer spacing and overlap
Entry and exit Both tracks share one layer Two depths can need different via launches
Use when Channel fits and etch window passes Routing benefit remains after tolerance and launch checks

For the example link, check whether changing the escape pattern would let both traces stay on one layer. A small connector breakout redesign can be preferable to two dissimilar transitions. Keep the stacked route if the saved width matters and the expected process spread is acceptable.

broadside coupled stripline calculator

Use a model that explicitly supports broadside geometry, including lateral offset if that is part of the build tolerance. A generic stripline or edge-pair calculator is not an equivalent model. Ask the fabricator for the proposed pressed stackup and expected finished dimensions, not just the nominal prepreg designation.

Input Unit or form What to vary
Finished track widths and copper µm Both layers separately
Trace-to-trace and plane spacing µm Pressed dielectric dimensions
Relative layer offset µm transverse to route Nominal and both shift directions
Dielectric properties Relative permittivity and frequency Approved construction and model
Differential impedance Ω Nominal and agreed process corners

Start with the aligned geometry, sweep offset alone to understand sensitivity, and then combine relevant limits with width and dielectric changes. For a link that turns through 90 degrees, a registration shift can project differently onto the two route segments. Check both orientations if the process tolerance or routing makes that distinction relevant.

Differential stripline impedance formula

For a symmetric pair with equal and opposite excitation, differential impedance equals twice the per-conductor odd-mode impedance. In this hypothetical 100 Ω link, 50 Ω odd-mode corresponds to 100 Ω differential. That does not mean two isolated 50 Ω traces will remain a 100 Ω pair when brought together.

The relation explains a solver output; it does not calculate impedance from width and spacing by itself. For unequal conductors or asymmetric placement, use a model that represents the actual cross-section, and check both differential behavior and conversion between differential and common modes. Do not reuse a symmetric calculation after making one leg materially different.

pcb layer registration

Registration is the alignment of one fabricated layer to another. A lateral shift can reduce copper overlap and change coupling even when both traces meet their individual width requirements. For two equal 120 µm tracks, a 30 µm transverse shift leaves 90 µm of geometrical overlap, or 75%, in a simple rectangular projection. This is a teaching example; 75% overlap does not mean a 25% impedance change.

Ask what the quoted registration figure refers to: two layers relative to each other, a layer relative to a datum, or another inspection definition. If each layer is only specified to a common datum, get an agreed relative tolerance or justify how the limits combine. Put the layer pair and the direction of the offset in the stackup review, then use that value in the model.

Polished multilayer PCB microsection on a microscope stage
Illustration: A section can check local dimensions and overlap at its cut location. It is not an electrical test of the complete route.

differential pair skew

Skew is the difference in arrival time between the pair’s two conductors. Matching length in the layout editor does not by itself prove matching delay: the two vias can have different lengths, and the two tracks can have different electromagnetic environments. Look at the complete path from transmitter to receiver.

In the connector example, both legs leave a component on the same outer layer and reach different inner layers. Model the two launches, including relevant reference transitions and via stubs, before adding a meander to correct a length number. A geometry change can improve time matching while making a discontinuity worse; check both effects.

differential impedance measurement

A matching differential time-domain reflectometry (TDR) coupon checks impedance along a representative fabricated cross-section. It should use the same signal-layer pair, reference planes, widths and spacing, and a suitable measurement launch. Agree on the trace region to evaluate so the launch and coupon termination are not averaged into the uniform segment.

If the uniform region fails, first confirm the setup and coupon geometry, then compare measured dimensions and registration with the model. If the uniform coupon passes but the link fails, inspect the actual vias, connector and return path. Use channel measurements or an applicable eye test when system performance is the concern. A passing coupon does not certify the complete assembled channel.

pcb layer to layer registration tolerance

Release the stacked pair only when the supplier’s usable registration and pressed stackup limits, the modeled process window, and the inspection plan agree. Put the target, tolerance, coupon structure and review criteria in the release package. Define which changes require a new model or approval, including substitutions that change the dielectric spacing.

For the example, assume the project has separately defined its 100 Ω tolerance and channel limits. If the agreed worst-case geometry fails or cannot be documented, choose the side-by-side routing or renegotiate the stackup before release. After a revision, rerun the same corner set, measure a representative coupon, and verify the assembled link against the project’s own limits.

FAQ

Can I stack the traces under a split in a reference plane?

Do not treat a plane split as equivalent to a continuous reference in the model. Review the return path and discontinuity, and reroute or model the transition if the split cannot be avoided.

Is nominal 100 Ω enough to sign off the routing?

No. The nominal result leaves out process variation and the channel launches. Compare the expected range against the specified window and plan measurements for the finished construction.

Can a surface microstrip coupon verify the inner broadside pair?

No. It does not reproduce the two inner signal layers and their dielectric and plane geometry. It can help validate its own geometry, not substitute for a matched broadside coupon.

Does a section through one location verify alignment across a panel?

No. A section provides local evidence. Agree on sample locations and additional registration evidence when panel variation could affect the result.

Can the two tracks use different widths?

They can be modeled that way if necessary, but an equal-width symmetric model no longer applies. Check the finished cross-sections, impedance, delay and mode conversion before approving the change.

Do I need to tune both tracks if the measured issue is at the connector?

Not necessarily. Locate the discontinuity first. Changing the uniform trace geometry can move the coupon result without resolving a launch problem.

Can I use the same layer-offset value as an etch-width tolerance?

No. Offset moves layers relative to each other; etch tolerance changes a feature within a layer. Use separate variables and supplier data in the model.

Is a broadside pair always better for crosstalk?

No. Pair coupling is not the same as isolation from neighboring routes. Check nearby conductors, plane geometry, the coupled length and the channel’s noise limits.

References

For a Best Technology manufacturing inquiry, send the proposed stackup, layer pair, finished routing geometry, impedance target and coupon requirements to sales@bestpcbs.com. Note any material or layout dimensions that cannot change.

LVDS Termination Resistor Guide: Value, Wiring and Layout

November 10th, 2026

Key Takeaways

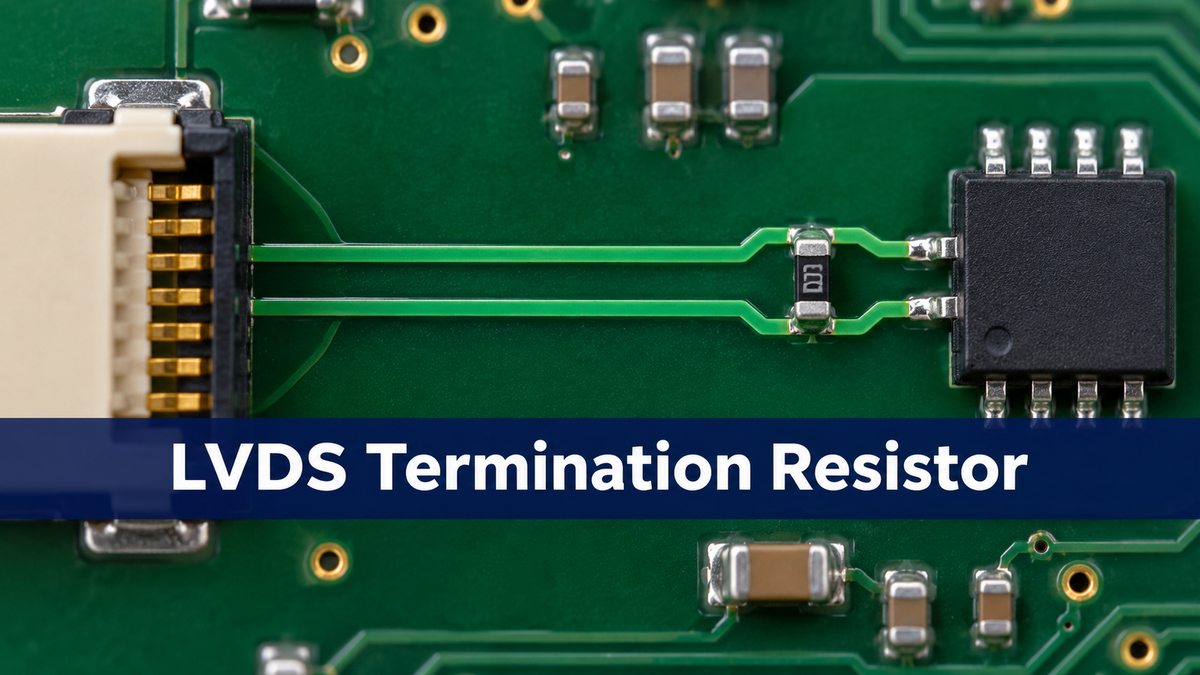
  • A conventional point-to-point LVDS link usually uses one differential termination at the receiver, commonly 100 Ω.
  • The termination both develops the received differential voltage and reduces reflections by matching the transmission line.
  • A representative 3.5 mA current through 100 Ω produces 350 mV; these are nominal teaching values, not universal guaranteed specifications.
  • Internal termination can replace an external resistor only when the exact device, I/O bank and active configuration support it.
  • Two ideal 100 Ω loads in parallel produce 50 Ω. Whether two loads are correct depends on the topology.
  • AC coupling needs appropriate transmitter-side loading, receiver bias and signal behavior—not just two capacitors.
  • Approve the channel using the receiver waveform and timing requirements, not a resistance reading alone.

An LVDS termination resistor is a resistor connected across the two signal conductors at the receiving end of a typical LVDS link. A common value is 100 Ω, selected to match the differential transmission-line impedance and convert the driver’s steered current into a small voltage that the receiver can detect.

Getting it right involves more than selecting a 100 Ω part. The receiver may already contain termination, a connector may extend the electrical path, and AC-coupled or multipoint links need different arrangements. This guide explains the principles, calculations, connection options and PCB decisions so a schematic can become a testable design.

Circuit-board differential traces and a small part near a receiver package
Illustrative rendering, not a reference footprint or validated routing.

what is lvds

LVDS means low-voltage differential signaling: information is represented by the voltage difference between two conductors, rather than by either conductor’s voltage to ground alone. The receiver decides whether P is above or below N.

Define the differential voltage as Vdiff = VP − VN. The common-mode voltage is their average:

VCM=VP+VN2

A positive differential voltage does not require either pin to go negative relative to ground. In an illustrative 1.2 V common-mode system, P = 1.375 V and N = 1.025 V give +350 mV differential. Swapping these levels gives −350 mV. The two states span 700 mV differential peak-to-peak—not 350 mV peak-to-peak.

Consider a hypothetical data-acquisition board carrying ADC data to an FPGA. Each lane needs an electrically compatible receiver and a defined load; successful data capture also depends on clock-to-data timing. LVDS specifies electrical signaling, not the complete data protocol. See TI’s LVDS technology overview.

lvds termination resistor

In the usual DC-coupled point-to-point circuit, the resistor connects from P to N, directly across the receiver input pair. It is not inserted in series with either conductor and is not a pull-down to ground.

The driver steers current out along one conductor, through the load, and back along the other. Reversing the current direction reverses the differential voltage. The high-impedance receiver observes that voltage while the resistor provides the intended current path.

The same resistor is the load at the end of the transmission line. Matching the load to the line helps prevent an arriving edge from reflecting back along the pair. These are related functions: replacing the resistor with an open circuit removes the intended DC load and also creates a large impedance discontinuity.

For the ADC-to-FPGA example, trace the two nets all the way through adapters and connectors before drawing the termination symbol. A resistor already on a mezzanine card is still part of the circuit. Analog Devices explains receiver-end LVDS termination.

lvds termination resistor value

The familiar 100 Ω value follows from the intended differential line impedance and the driver’s operating load. It is a common starting point, not a resistor value to apply indiscriminately to every differential interface.

A nominal current-source model gives:

|Vdiff|≈IRT=3.5 mA×100 Ω=350 mV

TI’s LVDS Owner’s Manual uses this representative model. Actual guaranteed output levels come from the selected driver’s electrical table.

Parameter Value and scope
Differential termination 100 Ω; common design value
Steered current 3.5 mA; nominal model
Differential magnitude 350 mV typical; SN65LVDS1, 100 Ω
Specified output magnitude 247–454 mV; conditions below
Specified output common mode 1.125–1.375 V; SN65LVDS1
Nominal integrated load 110 Ω; SN65LVDT2 only

The SN65LVDS1 range above applies with RL = 100 Ω and 3 V ≤ VCC < 3.6 V under the datasheet’s specified conditions. At lower supply voltage, its minimum differs. The typical value is not a guaranteed minimum, and the nominal 1.2 V teaching example is not a universal input requirement. See the Rev M electrical tables.

lvds impedance matching

Match the termination to the pair’s differential characteristic impedance—not to the resistance of the copper traces. Characteristic impedance describes how a traveling wave relates voltage and current along the interconnect; a multimeter cannot measure it as a DC resistance.

For an ideal uniform line with real differential impedance Zdiff and a resistive termination RT, the load reflection coefficient is:

ΓL=RT−ZdiffRT+Zdiff

These calculations assume a 100 Ω line and an ideal 3.5 mA driver for the separate steady-state voltage estimate:

Load Load reflection Ideal settled magnitude
90 Ω −5.26% 315 mV
100 Ω 0% 350 mV
120 Ω +9.09% 420 mV
50 Ω −33.33% 175 mV

A positive coefficient means the reflected voltage has the same polarity as the incident wave; a negative value means opposite polarity. The percentage refers to the incident traveling voltage, not to bit-error rate or total signal loss. The settled-voltage estimate is not a prediction of the complete transition waveform.

A 120 Ω load can increase ideal settled amplitude while worsening the match to a 100 Ω line. That is why “more voltage” is not automatically better. Nonstandard values require both a device-load check and a channel assessment. The underlying reflection model is described in TI’s LVDS Application and Data Handbook.

lvds termination resistor power rating

Normal LVDS termination dissipation is small, but select the resistor using voltage across the load, not the IC supply voltage. For an ideal 350 mV differential magnitude across 100 Ω:

PR=Vdiff2RT=(0.350 V)2100 Ω=1.225 mW

Both polarities produce the same resistive dissipation. Using the 700 mV differential peak-to-peak value in this formula would overestimate the ideal two-state dissipation by four times.

A 1% external resistor is a practical starting choice when the design does not specify otherwise. Its package, temperature coefficient, rated-power derating and parasitic behavior still matter. A smaller package can simplify a short, symmetric connection, but assembly capability and inspection access also constrain the choice. Calculate margin from the actual maximum operating differential voltage and resistance limits; fault conditions need a separate review.

lvds termination resistor placement

Place an external termination close to the receiver input pins, with short and balanced connections to P and N. The electrical route from the resistor to the input matters more than the distance between component outlines.

If the resistor sits beside a connector but the receiver is farther inside the board, the segment beyond the resistor becomes an unterminated branch of the intended load point. It can still disturb the receiver even though the schematic shows a correct resistor value.

For scale, assume a 20 mm post-termination segment and a propagation delay of 6 ps/mm. Its one-way delay is 120 ps and its round-trip delay is 240 ps. Against a hypothetical 500 ps edge, that is not automatically negligible. These are teaching assumptions, not a universal length limit.

Place the resistor across the incoming pair without a long tee, an asymmetric detour or an avoidable via. A selectable footprint should remain compact even when unpopulated.

lvds internal termination

Internal termination replaces the external load only when the selected receiver actually provides it in the intended operating state. “LVDS-capable input” does not by itself establish that termination is present or enabled.

For example, AMD’s DIFF_TERM documentation describes enabling built-in 100 Ω differential termination. Availability and valid conditions depend on the FPGA family, bank, I/O standard and supply requirements. Treat those conditions as part of the hardware design, not just a software detail.

Choice Trade-off
Internal load Near input; device, bank and settings matter
External resistor BOM controlled; placement and tolerance matter
Selectable Flexible; document the active option

On the ADC board, record the FPGA input standard, bank supply and active termination setting alongside the BOM population option. Check reset and configuration behavior if the ADC starts driving before the FPGA is ready. Do not infer powered internal resistance from an unpowered ohmmeter reading.

lvds double termination

A conventional single-receiver link is overterminated if an external load duplicates the intended internal load. For two ideal 100 Ω resistances at the same receiving point:

Req=100×100100+100 Ω=50 Ω

The ideal 3.5 mA model then gives 175 mV rather than 350 mV. A real driver may depart from that model, and separated loads introduce transmission-line effects. Reduced amplitude alone therefore suggests a loading problem; it does not prove one.

Establish the active receiver setting and populated components, restore the intended load, then compare measurements using the same pattern and probe setup. A different topology, such as M-LVDS, can intentionally require two terminations; “two resistors” is not a universal fault diagnosis.

lvds ac coupling termination

AC coupling blocks the transmitter’s DC common-mode voltage, allowing the receiver side to establish another bias level. It also changes the DC current paths, so it must be designed as a complete interface.

Review three things together:

  1. Transmitter operation: Does the driver need a DC differential load, and where is that path maintained after adding capacitors?
  2. Receiver bias: Is the input internally biased, or does it need an external common-mode network?
  3. Signal behavior: Can the clock or data tolerate startup charging and baseline movement during long intervals without transitions?

TI’s LMK00301 datasheet, AC-coupled differential operation shows arrangements that differ according to receiver termination and bias. Some maintain a driver-side DC load and accept the resulting swing reduction when a receiving load is also present. That is a designed network, not the accidental duplication discussed above.

DC-balanced data or a suitable continuous clock is easier to AC couple than an arbitrary static level. For the ADC example, consider idle patterns and clock stoppage as well as the normal stream. Do not copy a capacitor value without checking the longest transition-free interval, startup requirement and both devices’ input/output conditions.

lvds split termination

Split termination uses two resistors whose series sum provides the differential load. Two 50 Ω resistors connected from P through a midpoint to N present 100 Ω to an ideal differential signal.

The midpoint determines what else the circuit does. A capacitor from that midpoint to ground can provide a common-mode AC return. A prescribed bias network can establish a DC level in an appropriate AC-coupled implementation. A capacitor alone does not establish a DC bias because it is open at steady DC.

With equal 50 Ω resistors and identical common-mode movement on both lines, the resistors appear in parallel toward the midpoint: 25 Ω before the midpoint network. This differs from their 100 Ω differential series path. Mismatched parts or asymmetric routing can spoil that symmetry.

TI SLAA840 includes split-termination examples. Use them when the common-mode or bias requirement justifies the network; adding a midpoint capacitor is not a generic cure for poor differential routing.

lvds multidrop

One driver feeding several receivers is not the same as several devices taking turns driving a bus. Establish that distinction before deciding how many loads to fit.

Topology Load arrangement
Point-to-point LVDS One load at receiver
Single-source LVDS multidrop One far-end load; short taps
Multipoint M-LVDS Both bus ends; matched devices

In the single-source multidrop arrangement described by TI SLAA840, the driver is at one end and the load is at the farthest receiver. Intermediate receivers must not each add another parallel termination. Their capacitance and branch lengths still affect the waveform.

M-LVDS drivers are designed for the heavier loading associated with two bus-end terminations. Two 100 Ω end loads give a 50 Ω DC equivalent, but the distributed bus is not simply a point-to-point LVDS circuit with another resistor added. Use devices and a topology intended for that service. Analog Devices AN-1177 explains the distinction.

lvds pcb layout guidelines

Route the interconnect as a controlled electrical structure, preserving its geometry and reference environment through the entire path. A correct load cannot repair an inconsistent pair.

  • Impedance: derive trace width and gap from the proposed finished stackup, not another board’s nominal dimensions.
  • Reference planes: keep the intended reference continuous beneath the pair; review every layer change and return-path transition.
  • Symmetry: use comparable pad exits, vias, connector paths and protection on P and N.
  • Stubs: keep optional footprints and test connections compact. A long measurement branch becomes part of the circuit.
  • Timing: meet the device’s intra-pair and clock-to-data timing requirements without unnecessary tuning structures.

“100 Ω differential” does not mean any two individually 50 Ω routes will remain a 100 Ω pair when brought together. Coupling changes the result. Finished copper, dielectric height, pair spacing, solder mask and the nearby copper environment must agree with the impedance model.

For a concrete manufacturing handoff, see the Best Technology LVDS PCB routing example; its dimensions are an example, not a universal recipe.

Oscilloscope and differential probe beside a small PCB
Illustrative rendering of a test bench, not a waveform or compliance result.

how to measure lvds signal on oscilloscope

Measure the differential signal at the receiver using a suitable low-loading differential probe, and examine both amplitude and timing. A clean waveform at the transmitter does not establish what arrives at the input.

  1. Record the data pattern, line rate, termination state, supply condition and probe point.
  2. Use bandwidth appropriate to the edge speed, and keep the probe connection short and symmetric.
  3. Measure differential magnitude, ringing and timing; assess common mode with an appropriate setup.
  4. Use an eye diagram and functional error testing where the interface requirements call for them.
  5. Compare results with the selected devices’ input limits and the project’s timing or eye criteria.

Do not attach ordinary grounded probe clips to the signal conductors. Nor should two 50 Ω-to-ground scope inputs be assumed harmless: they can introduce another 100 Ω differential load and alter common mode. Probing can create the fault you are trying to diagnose.

Power-off resistance measurements can identify accessible passive paths when the circuit allows it. They cannot establish characteristic impedance or prove powered internal termination. A TDR coupon checks representative fabricated geometry; the receiver measurement checks the operating channel.

lvds signal integrity

Signal integrity is the combined result of loading, interconnect geometry and timing—not a property established by one resistor reading. Before manufacturing, align the schematic, layout, assembly choices and receiver configuration.

For the hypothetical ADC-to-FPGA board, the release record should identify the exact endpoints, selected input standard, intended termination and population option, approved stackup, target impedance and tolerance, timing constraints, and verification plan.

Observed result Useful next investigation
Unexpectedly low amplitude Effective load and probe loading
Ringing near transitions Stubs, connectors and impedance steps
Good amplitude, capture errors Clock alignment, jitter and timing
Failure only at startup Bias, reset and configuration sequence

These are starting points, not diagnoses. Close the loop by testing the same board revision and operating conditions against defined pass criteria. If a load change improves amplitude but worsens the eye or error rate, the job is not finished.

Frequently Asked Questions

Can a 100 Ω termination make a 3.3 V transmitter compatible with a 1.8 V receiver?

Not by itself. Supply voltage and signal voltage are different quantities. Compatibility depends on differential swing, common-mode range, pin limits and the receiver’s bank rules. Termination does not replace a required level translator.

Can a short LVDS link omit the resistor?

Do not remove it just because the traces are short. A current-steering driver may still require the load to establish its output voltage. A termination-free implementation needs explicit support from the selected device documentation and validation.

Is LVDS a communication protocol like SPI?

No. LVDS describes electrical signaling. The interface still needs defined data organization, clocking and timing. Two devices can both use LVDS levels without exchanging compatible data.

Does an idle receiver automatically produce a known logic state?

No. Failsafe behavior depends on the device and the fault condition: open inputs, shorted inputs and an undriven terminated line are different cases. Select a receiver with the required behavior or use its recommended bias arrangement.

Should every unused receiver input get 100 Ω?

Not automatically. Follow the device’s unused-input instructions. A resistor across an unused input does not necessarily establish a valid logic state, while adding loads to connected bus taps can overterminate the bus.

Can an ordinary series resistor replace the parallel termination?

No. Series source termination is a different method. A resistor inserted in one or both conductors does not provide the receiving-end current path and load required by a conventional LVDS circuit.

Does a working clock prove that the data lanes are correct?

No. Each lane can have a different load, interconnect or timing relationship. Verify the affected lanes and their relationship to the sampling clock rather than approving the interface from one clock trace.

When is AC coupling the wrong starting point?

When the interface must convey a static state indefinitely, has uncontrolled long idle intervals, or lacks a defined bias and startup plan. Begin with the device-supported DC-coupled arrangement unless there is a specific reason to isolate common-mode levels.

Conclusion

For a conventional LVDS link, start with the intended differential impedance, one receiving-end load and compatible input conditions. Then make the resistor value, placement, internal configuration and PCB geometry describe the same circuit. For a Best Technology PCB fabrication discussion, send the stackup, controlled net list, impedance requirements and receiver-area routing to sales@bestpcbs.com. Bare-board manufacturing checks and complete-channel electrical validation serve different purposes; define both where the application requires them.

Technical References

USB 2.0 Common Mode Choke: Check EMI and the Eye

November 10th, 2026

Add a USB 2.0 common mode choke only if the evidence points to noise on the data pair and the part improves emissions without consuming too much High-Speed signal margin. Compare a populated choke and a qualified bypass under the same test conditions. If emissions improve but the eye fails, the choke is not ready for production.

USB connector and a nearby small component on a circuit board
Illustrative rendering of a USB connector region, not a validated layout.

usb 2.0 common mode choke

A two-line choke uses coupled windings in series with D+ and D−. Ideally, signals flowing in opposite directions see little added impedance, while noise flowing in the same direction on both lines sees more. Real devices also have parasitics and differential loss. The part does not replace ESD protection, nor does it establish the pair’s PCB impedance.

usb common mode noise

First decide which path is carrying the noise. In a hypothetical USB service port, a radiated peak appears only when the cable is attached. That makes the cable a useful clue, not proof that D+ and D− are the source. Compare activity with controlled traffic and examine the shield and power paths. A data-pair choke will not necessarily address noise predominantly carried on VBUS or the shield.

common mode choke impedance

Read common-mode impedance versus frequency, then check the differential transmission and balance data. For example, Murata lists 90 Ω ±25% at 100 MHz for DLW21SN900SQ2 under its specified test conditions. That number is common-mode impedance at one frequency; it is not a differential routing target, bandwidth, or guarantee of attenuation in the product.

Parameter What to compare
Common-mode impedance, Ω Curve around the suspect frequency
Differential loss, dB Curve across the relevant signal band
DC resistance, Ω Maximum and balance between lines
Package and pinout Channel mapping and footprint

usb common mode choke selection

Prefer a device with relevant mixed-mode data and enough signal margin in the implemented layout. A higher catalog impedance at one frequency can still be the wrong choice if loss or imbalance increases. Keep a qualified bypass option where practical, but do not assume a jumper footprint is electrically invisible. Compare the routing geometry and inspect the built boards.

usb common mode choke placement

Follow the actual PHY and protection guidance. TI’s TUSB121x example places the choke close to the receptacle, on the PHY side of the ESD devices. That is a named implementation, not a universal placement rule. Preserve the shortest protection path from the connector and review the two parts together. See the USB 2.0 ESD placement guide for the separate transient-path check.

usb differential pair routing

Keep the pair symmetric through the connector, protector, choke pads and layer changes. If you provide bypass footprints, avoid an unused branch hanging from only one line. A common-mode problem can be aggravated by imbalance in the routing, so compare both the footprint and the continuous reference before asking the choke to hide a layout problem.

usb 2.0 radiated emissions

Compare the two builds using the same cable, orientation, equipment arrangement and representative activity. In the example, suppose the suspect peak falls by 4 dB after fitting the choke. That is an illustrative comparison, not a lab result or a compliance claim. Confirm the absolute result against the project’s applicable limit and check repeatability before crediting the component.

Outcome Decision
Emissions and eye both meet limits Confirm repeatability before release
Emissions improve but eye fails Reject; revisit part or routing
Eye passes but emissions do not improve Trace the actual noise path

usb 2.0 eye diagram

Verify the 480 Mbit/s High-Speed eye in the applicable test mode and fixture, not just enumeration or a short file transfer. A tight result with one cable is a reason to repeat the approved test under the required conditions, not to declare the change safe. For the controller example, release the choke only after the emissions result and the applicable USB electrical result both meet the agreed criteria.

USB test fixture and cable on a bench beside an oscilloscope
Illustrative rendering of a test bench. Use the specified USB test fixture and real capture for acceptance.

FAQ

Is the choke needed on every High-Speed port?

No. Use evidence from the intended system and the device guidance. A correctly working port need not add unnecessary loading.

Can I select a choke using only its 100 MHz impedance?

No. Compare frequency-dependent common-mode behavior, differential loss and the actual board measurements.

Can a bypass trial leave the pads empty?

Not if that opens the signal lines. Use the qualified bypass connection for the designed footprint.

Does enumeration show the High-Speed eye passes?

No. Enumeration is a functional observation. Use the applicable electrical test for the eye and signal limits.

Will the choke fix ESD resets?

Not by default. Inspect the discharge path and protection design separately, then verify the system’s ESD behavior.

Should I compare different cables in the first A/B test?

Keep the cable fixed for the first comparison. Test additional required cables separately to verify system robustness.

Can a data-pair choke fix VBUS noise?

Only if the coupling path involves the data pair and the change is shown to help. Inspect the power path if that is the dominant source.

Does a lower measured peak mean the product is compliant?

No. Check the applicable limit, modes and repeatability. A relative improvement and a compliance result are different claims.

Sources

TI TUSB121x board guidelines; TDK: USB 2.0 EMC practice; Murata DLW21SN specifications.

Project Review

For a Best Technology fabrication discussion, send the stackup, D+/D− geometry, connector footprint and choke or bypass options to sales@bestpcbs.com.

Microvia Reliability: Read the Reflow Resistance Trace

November 10th, 2026

Don’t release an HDI lot on the strength of a cold continuity check alone when the purchase requirements call for reflow-monitored resistance. First verify that the coupon reproduces the critical via structure. Then compare its resistance trace with the agreed reference and temperature profile. A chain can read normally after cooling even if it opened during heating.

Mounted PCB cross-section with copper interconnections and dielectric layers
Illustrative rendering of a cross-section specimen. Use the actual stack drawing and coupon record to identify via geometry.

microvia reliability

Microvias connect adjacent PCB layers in dense layouts. During soldering, the board expands and contracts, stressing these connections. A room-temperature continuity result answers whether the path conducts at that moment. It does not reveal an interruption that occurs only at elevated temperature. Ask for the evidence that matches the anticipated assembly exposure.

stacked vs staggered microvias

A stacked design places one microvia above another. A staggered design offsets them and joins the paths on a shared layer. When the board uses both, identify which geometry each coupon actually represents. A result from a staggered chain should not be used to approve an unrepresented stacked interface. For routing and construction trade-offs, see the BestPCBs comparison guide.

Board feature Check on the coupon
Stacked microvias Same layer spans and stacked interface
Staggered microvias Correct layer spans and offset pattern
Mixed connections Coverage of each structure required for release

pcb daisy chain

A daisy chain connects many via structures in series so that a change anywhere in the path can appear in the resistance record. Ask for the chain ID, layer pairs, structure count and panel-to-coupon relationship. The resulting trace describes the chain, not the resistance or failure location of an individual via. A chain that includes other structures may require fault isolation.

Bare test coupon and measurement leads on an electronics lab bench
Illustrative rendering of a coupon setup, not a test log or a pass result.

pcb reflow profile

Compare traces only under the approved profile and measurement convention. Record the test method and revision, profile, cycle count, temperature measurement location and reference resistance. For a performance-based evaluation under IPC-TM-650 2.6.27, use the reference and acceptance criteria in the applicable revision and procurement agreement. Do not silently substitute a cold baseline for a specified hot reference.

Report field Why it matters
Profile and cycle Matches the specified exposure
Resistance in Ω or mΩ Identifies the measured chain and reference
Change in % Shows the result at the specified comparison point
Temperature and time Locates the event within the cycle

microvia failure

Consider an illustrative chain with a specified hot reference of 0.500 Ω. A comparable point in a later cycle reads 0.530 Ω. The relative rise is (0.530 − 0.500) ÷ 0.500 = 6%. If the project limit were 5%, the reading would exceed it. A normal cold reading afterward does not cancel the event. These values are a worked example, not a test report or a universal limit.

Check whether the event is synchronized with temperature and whether other channels show a simultaneous fixture disturbance. Preserve the original trace and reference coupon. When instrumentation remains a plausible cause, use the documented investigation or retest procedure instead of deleting the event or releasing on the final reading alone.

pcb microsection analysis

Use the electrical record to choose where to section. A section can show a physical discontinuity at a sampled interface, but a clean section elsewhere cannot rule out a hot-only failure in the chain. Ask the lab to correlate the section location with the failed net, stack and panel rather than accepting an unlabeled image.

interconnect stress test pcb

Convection reflow simulation reproduces an agreed assembly heat exposure. DC current-induced thermal cycling is a different test method with a different heating mechanism and protocol. Don’t accept one in place of the other simply because both include resistance readings. Match the report to the contracted exposure, specimen and evaluation method.

pcb thermal cycling test

Specify separately any cycling needed to qualify the board for service. A reflow simulation result alone does not establish lifetime under operational temperature changes. For lot release, verify the approved coupon map, profile, complete trace and disposition of any anomalies. If the controlling geometry or hot record is missing, mark the evidence incomplete rather than treating the omission as a pass.

FAQ

Is the final resistance value enough?

No when the requirement covers behavior during the cycle. Inspect the agreed measurement interval and preserve any anomalous excursion.

Can an unmarked coupon represent every panel?

Not without documented traceability and an agreed sampling plan. Link its identity to the appropriate panel, lot and build.

Does a resistance excursion prove a microvia crack?

No. It locates a suspect time and chain. Check the test setup and use targeted failure analysis before assigning a cause.

Can I compare two chains with different numbers of vias directly?

Not by raw resistance alone. Geometry and chain length affect the value. Use the prescribed baseline and compare equivalent structures where possible.

Does a passed stacked coupon qualify a deeper stack?

Not automatically. Additional interfaces and different layers can change the behavior. Confirm that the evidence represents the intended construction.

Does the oven setpoint equal coupon temperature?

No. Confirm the recorded measurement convention and coupon temperature rather than assuming the displayed setting is the specimen profile.

Can I approve the lot if the report only says pass?

Only if that is sufficient under the agreement. When the purchase requires traces, conditions or specimen details, request the missing evidence before release.

What should I retain for a repeat order?

Keep the approved stack, coupon ID and drawing, reference convention, test profile, original records and disposition together with the production revision.

Sources

IPC-TM-650 2.6.27B: convection reflow assembly simulation; IPC-TM-650 2.6.26A: DC current-induced thermal cycling.

Project Review

For a Best Technology fabrication discussion, send the critical via stack, intended assembly exposure and coupon acceptance requirements to sales@bestpcbs.com.

PCB Thermal Relief Troubleshooting: Find the Hot Spot

November 10th, 2026

If a power terminal runs hot, don’t replace its thermal relief with a solid connection until you know where the voltage is lost. Under a controlled load, compare the terminal and joint with the pad-to-plane transition and the downstream copper. Only change the relief when the evidence points to that transition, then retest both solder quality and operation.

Bare PCB showing a through-hole pad connected to a copper area through relief spokes
Illustrative rendering of a relief connection. Use the actual exported copper to count and measure spokes.

what is thermal relief in pcb

Thermal relief leaves a gap between most of the pad perimeter and its same-net copper plane, with short copper spokes bridging that gap. Less copper cross-section slows heat flow out of the pad while soldering. The same restriction remains in service, so easier soldering and lower operating resistance are separate goals.

thermal relief vs direct connect

A direct connection is a useful comparison build when the suspect span is the pad-to-plane transition. Keep the connector, copper build and load the same. Changing the connector and the pad in the same trial makes it hard to tell which part of the current path improved. The general thermal relief design guide covers first-pass layout decisions; this article starts with a board that is already running hot.

Connection When to consider it Verify
Relief spokes Plane slows joint heating Joint, drop and heat
Direct copper Spokes limit current path Joint and copper neck
Revised spoke geometry Both constraints matter Actual fill and tests

thermal relief spoke width

Use finished width, length and copper thickness when estimating a spoke path. Increasing width or adding equivalent spokes can lower its resistance but also lets more heat leave the pad during assembly. In an ideal group of equal spokes, their conductances add in parallel. Real current distribution depends on where the plane is fed, so a layout with four spokes drawn does not necessarily share current evenly.

Parameter What to verify
Spoke width and length, mm Finished geometry on each connected layer
Remaining spoke count Connections after zone refill and export
Copper thickness, µm Applicable layer and fabrication build
Drop and temperature Named points and defined load conditions

pcb thermal relief gap

The relief gap separates the rest of the pad from the plane. A larger gap can lengthen the copper bridge; a nearby clearance can remove a spoke entirely. Refill the zone after a routing change, run the connection checks and inspect the released copper layer. A net name or a schematic check cannot establish what was fabricated.

pcb thermal relief high current

Use the actual operating load and allowable drop to judge the power pad. In a hypothetical 8 A terminal comparison, suppose a four-wire measurement across matched pad-to-plane points gives 3 mΩ for one build and 1 mΩ for another. The corresponding drops are 24 and 8 mV; calculated dissipation in that measured span is 0.192 and 0.064 W. These values are not ratings or measured results. They show why a milliohm-scale restriction can matter.

Plan accessible, named voltage-sense points before energizing the setup. If the board exposes them, use the terminal metal, the PCB pad and the plane just beyond the relief as three successive references. Put the load-current leads outside the sense span. A large terminal-to-pad drop points to the joint and intervening metal; a large pad-to-plane drop points to the PCB transition. If the pin-to-pad boundary is not accessible, report the combined span instead of assigning the loss to the joint. A distant point on the plane can add the loss of an unrelated narrow region.

Compare like-for-like at the same load and thermal state. If the hot spot remains but all measured local voltage drops are small, check for a nearby heat source or an unsuitable surface for infrared temperature measurement before blaming the spokes. The busbar joint resistance guide shows the same principle of separating a joint from its conductor.

thermal relief soldering

Check the actual assembly method before treating a solid connection as a defect. A joint that is hard to make by hand may be acceptable under a qualified production process. Conversely, a low-resistance layout is not ready if the joint fails the required inspection. Compare the relief and direct options using representative boards and the intended process; don’t compensate with unapproved soldering conditions.

Power terminal on a circuit board with copper areas and nearby through-hole pads
Illustrative rendering of a power terminal. A real comparison requires the same load, assembly process and measurement span.

pcb copper pour

Trace the current from the connector through the pad, spokes or direct entry, layer transitions and the next component. The useful width is the narrowest effective path, not the largest patch of copper in the layout view. Keep unrelated pads on the chosen general rule; apply a documented override only where the individual connection needs it.

pcb thermal relief guidelines

Decide what to change based on the span that failed. For a joint issue, review solder fill and the assembly method. For a PCB transition issue, compare wider spokes or direct copper. For loss downstream, fix the neck or layer transition and leave a sound pad unchanged. Release only after the revised joint, drop and temperature rise meet the agreed limits at the intended load, ambient and enclosure conditions.

FAQ

Are four spokes always better than two?

No. More effective copper can lower resistance, but the result depends on geometry and feeding. It also changes heat flow during soldering.

Does increasing board copper weight fix a missing spoke?

No. First fix or qualify the actual connection. Extra copper cannot replace a segment removed by the pour clearance.

Can I apply the same relief to every ground pad?

Not by default. A signal return, power terminal and heat-dissipating pad may have different connection needs even when they share a net.

Is an exposed package thermal pad the same as thermal relief?

No. A package thermal pad may need to conduct heat away in service. Relief spokes deliberately reduce the copper path around a pad.

Can I use a trace-width calculator as the final acceptance test?

No. It can help screen the layout, but it does not capture every local bottleneck or reproduce the full assembly and load conditions.

Should I measure resistance cold or after loading?

Record both when useful and keep the measurement span fixed. The operating drop and temperature should be checked under the specified load.

Why does my CAD tool report incomplete relief?

A zone rule or nearby clearance can prevent the required number of spokes from connecting. Refill and inspect the actual copper before changing the rule.

Can the same choice be reused after a connector change?

Recheck the pad geometry, copper path, current and assembly conditions. The prior result applies to the tested construction, not automatically to a new footprint.

Sources

KiCad PCB Editor: zone and pad connection settings.

Project Review

For a Best Technology fabrication discussion, send the finished copper thickness, high-current pad geometry, expected load and intended assembly process to sales@bestpcbs.com.

CAN FD Termination Guide: Check Resistance and Ringing

November 10th, 2026

Start with two matched end terminations on a conventional linear CAN FD bus. With the bus safely de-energized and the applicable network isolated, about 60 Ω across CANH and CANL is a useful check for two nominal 120 Ω ends in parallel. It cannot tell you where those resistors are or whether a long stub is causing ringing. Check the physical ends next, then measure the differential and common-mode waveforms separately.

CAN controller PCB beside a twisted pair connected to a terminal block
Illustrative rendering of a CAN interface, not a validated circuit or a compliance result.

can fd termination

Termination matches the end of a transmission line to reduce reflected edges. The physical ends of the trunk are the ends that matter, not the two nodes with the lowest software addresses. Confirm the bus topology and cable impedance before applying the conventional two-end model. An engineered non-linear network needs its own analysis rather than extra resistors added by trial and error.

can bus termination resistor location

Walk the actual harness and mark both ends, every branch and any switchable termination. A termination at an intermediate node can still contribute the expected DC resistance while leaving a length of cable beyond it unterminated. In a hypothetical controller and sensor harness, a service node is plugged in midway and accidentally has termination enabled. If the far end is also missing its resistor, the meter can still show 60 Ω, yet the far end remains electrically open to an arriving edge.

can bus termination resistor value

For the conventional 120 Ω network, use a nominal 120 Ω differential termination at each physical end. In a split arrangement, two matched nominal 60 Ω resistors form one 120 Ω end. The midpoint capacitor adds a path for common-mode AC energy without adding a DC resistor across the pair.

Parameter What to verify
Nominal end resistance 120 Ω for the conventional cable
Split pair Two matched 60 Ω resistors per end
Midpoint capacitor Value, rating and return for this design
Resistor power Check fault voltage, duration and part rating

can bus termination resistance

With power removed and the network in the intended measurement state, compare the reading with the expected parallel combination. Two 120 Ω resistors give 60 Ω, one gives 120 Ω and three give 40 Ω in the ideal calculation. Treat those as clues, not acceptance limits: tolerances, other DC paths, internal switches and the connected harness can change the reading. Segment the harness as permitted and identify each termination before concluding that a board needs rework.

can fd split termination

Use a single resistor when the end is correctly matched and the common-mode behavior meets requirements. Consider split termination when the end match is right but common-mode disturbance remains an issue. It adds parts and a return path to review. It does not move a termination to the right place or shorten a stub.

Option Use when Verify
Single resistor End match and emissions are acceptable Value and physical location
Split pair plus capacitor Common-mode improvement is needed Matching, return and EMC result
Topology correction There is an incorrect end or long stub Reflection at the affected receiver

can bus split termination capacitor value

Choose the starting value from the transceiver and system guidance. NXP’s FS2400 example lists 4.7 nF as a nominal option, not a universal requirement. In a simplified common-mode model, the two 60 Ω branches act in parallel, so the effective resistance is 30 Ω. Together with 4.7 nF that gives about 1.13 MHz for the ideal RC corner. Cable and return impedances, parasitics and other components change the real response. That number is not a CAN FD data-rate limit and cannot predict compliance.

can bus signal reflections

If errors cluster after edges or at the faster data phase, look for timing and topology clues before changing the capacitor. On the hypothetical service harness, restore termination at the physical far end and disable the misplaced branch termination. Repeat the same capture. If ringing persists at one branch, compare the branch connection and length against the approved network design. A changing common-mode signal alone is not proof of a differential reflection.

can bus oscilloscope waveform

Measure CANH minus CANL for differential behavior and, with a suitable referenced and matched setup, use their average to inspect common mode. Follow the instrument and equipment safety instructions and avoid grounding a floating bus through the probe. Compare the same receiver, harness, traffic and supply conditions before and after changes. Release only when the correct end map, resistance, waveform or timing limits, error behavior and any required system EMC tests meet the project plan.

CAN evaluation board and twisted pair on a bench near an oscilloscope
Illustrative rendering of a scope bench. Use calibrated measurements and the actual receiver location for comparison.

FAQ

Why do I see 60 Ω but still get errors?

The meter cannot locate the resistors or see stubs, receiver timing or interference. Confirm the end map, then capture signals at the failing receiver.

Should every node include an enabled 120 Ω resistor?

No. In a conventional linear trunk, enable termination at the two physical ends. An optional resistor footprint on an intermediate node can remain unpopulated or disabled.

Does split termination change the nominal differential DC resistance?

Not when each end still sums to the specified end resistance and the midpoint capacitor has no DC conduction path under the measurement conditions.

Can I choose capacitor size by looking at the data rate?

Not alone. The midpoint network targets common-mode behavior. Start from the device guidance and verify it against the actual noise and immunity requirements.

Does unplugging a node always leave the resistance unchanged?

No. The unplugged module may contain an end resistor or active termination. Identify what was removed and re-evaluate the expected reading for that configuration.

Should I fit a common-mode choke before changing the layout?

Check the failure mechanism first. A choke may help a specific emissions or immunity issue, but it will not correct an unterminated cable end or an overly long stub.

Is a clean waveform at the transmitting node enough?

No. Check the receiver that sees errors and other electrically distinct points. A reflection that is mild at one location may be significant at another.

What if the conventional 60 Ω rule does not fit this network?

Use the network designer’s topology and expected measurement state. Switched termination, active networks and branches require interpretation beyond the simple parallel model.

Sources

NXP AN14183: CAN components example; TI: TCAN evaluation module termination options; TI: split termination and common-mode behavior.

Project Review

For a PCB fabrication discussion, send Best Technology the board stackup, connector region and proposed termination footprints at sales@bestpcbs.com. If the protocol itself is still being selected, see the CAN bus vs LIN bus guide.

USB 2.0 ESD Protection: Where to Put the Diode on a PCB

November 10th, 2026

For a USB 2.0 High-Speed port, start with a low-capacitance ESD diode close to the connector. Route D+ and D− past the protection pads without long branches, and give the diode a short return into the intended reference. Verify both USB signal quality and system ESD behavior: a board can enumerate and still reset during a discharge, or survive a strike and still fail the High-Speed eye test.

USB-C receptacle with small protection components at the edge of an assembled PCB
Illustrative rendering of a connector area, not a reference layout or a test result.

usb 2.0 esd protection

Protect the path from the exposed connector to the USB transceiver. When a transient exceeds the diode’s operating region, the diode conducts current into its return path instead of allowing all of the pulse to continue toward the transceiver. During normal signaling the device should remain off, but its capacitance still loads the pair. The goal is to minimize both the discharge loop and the disturbance seen by the data signals.

usb esd protection circuit

Draw two paths before choosing the footprint: the D+/D− signal path from the connector to the PHY, and the transient current path from each exposed data line through its protector into the designated return. The reference circuit for the selected part determines which pin is the return and whether the device uses a rail reference. A D+/D− protector does not establish protection for VBUS, CC or SuperSpeed pairs. For the rest of the interface, see the USB-C PCB design guide.

usb 2.0 esd protection diode

Choose a device against the PHY and connector requirements, not the largest advertised discharge rating. For example, TI’s USB application note lists ESD122 as a dual-channel D+/D− option with a 3.6 V reverse working voltage and 0.2 pF listed capacitance. Those figures belong to that device; use its current datasheet for test conditions and limits, then check actual layout and system behavior.

Parameter Decision check
Working voltage, V Check against normal line voltage
Line capacitance, pF Use stated test conditions and PHY budget
Clamping voltage, V Compare only at matching pulse conditions
Channel and package Confirm pin map and a routable return
Discharge rating, kV Check method; verify on the complete product

esd diode placement

Put the protector at the first practical point after the connector and keep both the connection to the data pads and the discharge return short. A component can look close in the placement view while its ground trace makes a long trip around a cutout. Check the copper layers and return vias, not just the component outline. Do not route the unprotected connector segment alongside sensitive circuitry if it can be avoided.

Close-up of a board-edge USB-C receptacle and a nearby black leadless component
Illustrative rendering. Verify the chosen footprint and discharge return on the actual PCB.

usb esd protection layout

Prefer flow-through routing when the part and footprint allow the data traces to pass directly through the protection-pad area. The diode remains a shunt element; the name describes the routing, not a series electrical connection. A short branch can be an alternative if the pinout forces it and the implemented design passes both signal and system ESD tests.

Routing option Use and trade-off
Flow-through First choice when pad map and return align
Very short branch Possible when constrained; measure the result
Long branch or remote clamp Revise: extra stub and transient loop

usb differential pair routing

Keep the two data paths physically similar through the connector, protector and first layer transition. Review reference continuity and avoid adding a long test stub to only one member of the pair. In a hypothetical compact service-port board that resets during cable-side testing, first inspect the discharge route and nearby reset or power circuits. If the same board also shows poor High-Speed signaling, check the diode capacitance, pad discontinuities and pair asymmetry before choosing a different clamp rating.

usb 2.0 differential impedance

The usual High-Speed differential routing target is 90 Ω nominal; confirm the tolerance and stackup requirements for the design. A calculated trace width covers the uniform section, not the pad and via transitions. Review those transitions separately, and include the protection device’s capacitance. The relevant data rate is 480 Mbit/s in High-Speed mode, but edge behavior is not determined by the bit rate alone.

usb 2.0 eye diagram

After a layout revision, verify the applicable High-Speed electrical test separately from the system ESD test. Use the specified USB test mode and fixture for the electrical test; for ESD, record the strike point, polarity, operating mode and allowed recovery behavior under the product test plan. Monitor real data traffic, resets and re-enumeration. Release only when the electrical result meets its applicable limits and the product meets its own ESD performance criterion. Successful charging or idle enumeration is not a substitute for either check.

FAQ

Can one array cover VBUS and the two data lines?

Some products can, but check the channel specifications and routing. VBUS operating voltage and exposure may differ from the data lines.

Is a larger TVS diode always a safer upgrade?

No. A larger part may add capacitance or create a worse return path. Check clamp behavior under comparable pulse conditions as well as link quality.

Can I place the protector on the bottom side?

Sometimes. Compare the complete path including signal vias, return vias and loop geometry. Verify the actual implementation rather than judging it by distance in a top view.

Should the common-mode choke go before the diode?

In TI’s TUSB121x example it follows the ESD protection. Confirm the sequence in the PHY and protector references and qualify it on the actual board.

Does a connector shield replace the data-line protector?

No. Shield bonding and signal-line protection address different paths. Follow the intended chassis and board grounding architecture rather than assuming they are interchangeable.

Why might the port restart even though no diode failed?

A transient can disturb the supply, reset path or reference. Capture the symptom and investigate the current route and nearby sensitive circuits before replacing the diode. The PCB ground bounce guide explains how a changing local reference can show up in a measurement.

Is a device-level rating proof of system compliance?

No. The assembled product adds connector, enclosure, layout and grounding variables. Verify it with the applicable system test and performance criteria.

Does this placement apply unchanged to USB SuperSpeed?

No. Check the separate transmit and receive paths, channel budget and AC coupling architecture. This guide addresses USB 2.0 D+ and D−.

Sources

Texas Instruments: ESD and Surge Protection for USB Interfaces; Texas Instruments: TUSB121x board guidelines; Nexperia: ESD protection for USB 2.0 interfaces.

Project Review

For a PCB fabrication discussion, send Best Technology the proposed stackup, pair geometry and connector-to-protector region at sales@bestpcbs.com.