

PCB manufacturing PCB manufacturing
Home > Blog

KiCad MCP: How to Connect AI to KiCad and Check the Results

September 11th, 2026

KiCad MCP connects an AI assistant to tools that can read or change a KiCad project. You can use it to investigate component connections, make supported design edits, and request checks against actual project data. The available operations depend on the MCP server you install.

This guide uses Windows, KiCad 10, Konnect, and Claude Desktop to explain the connection process and a first PCB edit. You will move one footprint, compare the result with its starting state, and check whether the edit introduced a board-rule violation. The walkthrough follows project documentation; the example is a practice exercise rather than a measured test result.

KiCad MCP

What Is KiCad MCP?

KiCad MCP is a general name for integrations that give AI applications access to KiCad-related tools through the Model Context Protocol. Different servers expose different features, so there is no single installation that represents every KiCad MCP project.

The connection works like this:

Your request → AI application → MCP server → KiCad data or tools

The AI application interprets your request and calls an available tool. The server carries out the operation through its supported interface, such as KiCad’s API, a project file, or a command-line tool. The Model Context Protocol provides the communication framework between the application and server.

For example, you might ask which pins connect to a particular net before investigating a schematic problem. In an editing workflow, you might ask the assistant to move a footprint to a specified position. The practical benefit is that the answer or action can be tied to the design you are working on.

Which AI Assistants Work with KiCad MCP?

Claude Desktop, Claude Code, GitHub Copilot in VS Code, Cursor, and Windsurf have configuration routes documented by the projects below. Choose a combination with instructions for both your AI application and your selected server.

AI application Documented connection route
Claude Desktop Konnect’s local server setup, used in this guide
Claude Code Konnect’s project-level MCP configuration
GitHub Copilot in VS Code The original KiCAD-MCP-Server configuration
Cursor or Windsurf Seeed’s MCP client configuration

A model name alone does not establish compatibility. The application hosting the model must support the server’s connection method and permit tool calls. For the walkthrough below, run Claude Desktop and KiCad on the same Windows computer.

Which KiCad MCP Server Should You Use?

For the live footprint edit in this guide, use Konnect with KiCad 10. If your main task is schematic analysis or you already maintain a different integration, compare the alternatives by the work you need to perform.

Server When to consider it Setup consideration
Konnect Editing a live KiCad 10 board through its IPC API Native plugin package; currently identified as beta
Original KiCAD-MCP-Server Continuing or adapting an existing workflow built around this implementation Separate Python/TypeScript dependencies; do not use Konnect’s installation instructions
Seeed-Studio kicad-mcp-server Investigating components, nets, and pin connections in project files Its documented full PCB analysis setup uses KiCad’s Python environment

Konnect is the original project’s successor, while the original server remains maintained. For a new installation following this article, staying with Konnect keeps the package, configuration, and editing tools consistent. Check the chosen project’s license before adopting it for your intended use.

For Seeed’s server, the Python environment affects the information available: its documented system-Python fallback offers more limited PCB analysis. That distinction matters if your task needs detailed board information rather than basic component or net data.

How Do You Connect AI to KiCad Using MCP?

Install the plugin, enable KiCad’s API connection, register the server in Claude Desktop, and confirm that it can read your board. Use a separate practice copy of an existing project, keeping its board, schematic, and project settings together.

1. Install the Konnect plugin.

Download the Windows PCM ZIP from Konnect Releases. In KiCad 10, open Plugin and Content Manager, choose Install from File, select the ZIP, and restart KiCad. Check Tools → External Plugins in the PCB Editor for Konnect. The PCM ZIP is the plugin package; other release archives may contain standalone server binaries.

2. Connect Konnect to the open board.

Open the practice board and enable the KiCad API under Plugins in KiCad’s preferences. Copy the complete listening address, including ipc://. In Konnect’s settings, paste that address into the IPC Socket field and save it. This address must come from your own KiCad session.

3. Register Konnect in Claude Desktop.

Edit %APPDATA%\Claude\claude_desktop_config.json. If you have no existing server configuration, use the following structure. Otherwise, add only the konnect entry inside your existing mcpServers object, keeping the other entries intact.

{
  "mcpServers": {
    "konnect": {
      "command": "C:\\Users\\YOUR_NAME\\Documents\\KiCad\\10.0\\3rdparty\\plugins\\com_github_mixelpixx_konnect\\bin\\konnect.exe"
    }
  }
}

Replace the example command with the actual installed executable path. The doubled backslashes are required by JSON string escaping. Check that the executable exists, save the configuration, and fully restart Claude Desktop.

4. Read the practice board.

Keep the board open and send this prompt:

Use Konnect to inspect the board currently open in KiCad. Report the board file path, copper layer count, and component references. Do not change anything. Include the tool output that identifies whether you accessed the live board or a saved file; if the tool does not report this, say so.

Compare the file path and references with your practice project. Proceed when the returned information matches. If tools are visible but the board cannot be read, use the connection troubleshooting section before requesting an edit.

KiCad MCP

How Do You Edit a PCB with KiCad MCP?

Describe the object, the change, and the properties that must stay fixed. A first edit should be easy to inspect, such as moving one unlocked, unrouted resistor on a practice board.

The Konnect tool directory covers schematic operations, footprint placement, routing, and checks. These are distinct tasks: moving a component is a useful introduction to editing, while routing requires its own instructions and review.

Prepare a baseline before changing anything.

Choose a resistor with enough clear space around it for a 2 mm move. Save the practice project and keep an untouched copy for comparison. In the PCB Editor, run Inspect → Design Rules Checker with zone refill enabled and save the report. This gives you the board’s starting condition, including any existing unconnected items.

Read the component’s starting state.

Use its actual reference in this prompt; R1 is the example:

Find R1 on the practice board. Report its X and Y coordinates in millimetres, rotation, board side, and pad net names. Do not modify it.

Check these values in KiCad’s footprint properties and pad properties. Use the same coordinate origin and units throughout the comparison. If the returned data does not match, resolve the discrepancy before continuing.

Request one specific edit.

Move R1 by +2.0 mm along the board’s X axis. Keep its Y coordinate, rotation, board side, and pad net assignments unchanged. Do not change tracks, vias, other components, or design rules. Stop if R1 is locked or the operation cannot be completed as specified.

An axis and distance give you a measurable result. An instruction such as “improve the layout” leaves the assistant to decide which objects and relationships it can change.

Read back the position.

Read R1 again using the board tools. Report its current coordinates, rotation, board side, and pad net names, and compare them with the starting values.

The expected relationship is:

X_after = X_before + 2.0 mm; Y_after = Y_before

Verify the result in KiCad. Reading R1 back establishes its reported state; checking for unrelated changes requires a wider comparison, as described below.

How Do You Check AI Changes in KiCad?

Check three things: whether the requested change happened, whether other design objects changed, and whether the board developed new rule violations. Each requires different evidence.

Check Evidence to use
Requested footprint move Before-and-after footprint and pad properties in KiCad
Unrelated changes A comparison with the untouched board, including object properties and saved-file differences where needed
New board-rule violations DRC reports from before and after the edit, using the same settings

Inspect the board beyond the moved footprint.

Look for overlap with adjacent components, movement across the board edge, and unexpected changes to nearby tracks or vias. Compare the edited board with the untouched copy before accepting the change. A saved-file diff can reveal additional edits, but formatting changes and generated data still need interpretation.

A visual review is useful for placement; it does not establish that every property stayed unchanged. If you have only checked R1, keep the conclusion limited to R1. An AI statement that “nothing else changed” needs supporting comparison data.

Compare the DRC results.

Run the checker again with zone refill enabled, using the same rules as the baseline. Inspect individual findings and their locations. A board can have the same total error count while one old problem disappears and a different problem appears.

On an unrouted practice board, existing unconnected items may remain after a successful move. Investigate newly introduced violations and any unexpected changes to the earlier findings. If the edit is wrong, undo it in KiCad or restore the practice copy, then recheck before trying again.

Match the check to the design change.

A footprint-only move calls for placement, connectivity, and board-rule review. If you also change the schematic, run electrical rule checking and check that the schematic and PCB remain consistent. Neither test establishes the circuit’s functional performance.

KiCad MCP

How Do You Fix KiCad MCP Connection Problems?

First determine whether the failure is between Claude Desktop and the server, or between the server and KiCad. Visible MCP tools confirm only the first part of that connection.

Symptom First action
No Konnect tools appear Check the executable path and JSON syntax, then fully restart Claude Desktop
Tools appear, but the board is unavailable Open the board, enable KiCad’s API, and save the current IPC address in Konnect
Results miss your latest edits Check whether the tool read a saved file or the live editor before requesting further work
An older installation seems to be running Use get_installation_info to check the active executable and build
A check reports that kicad-cli is missing Check the CLI path and the active Konnect configuration

After correcting a setting, repeat the read-only board prompt from the connection section. Confirm that the expected project is accessible before resuming edits.

If you need help, include the exact error, installed versions, and last successful step. “Konnect tools appear, but reading the open board fails” identifies the failing stage more clearly than “KiCad MCP does not work.”

FAQs About KiCad MCP

Is KiCad MCP an official KiCad product?

The servers discussed here are third-party projects. Using KiCad’s API does not make an integration an official KiCad product.

Can KiCad MCP work without the PCB Editor open?

Yes, for supported file-based operations. For example, schematic-file analysis can use a different access method from live board editing. The footprint exercise in this guide uses an open PCB Editor and an active IPC connection.

Does KiCad MCP include an AI model?

The server supplies tools. Your AI application supplies model access, with its own account and usage requirements.

Can I ask AI to design an entire PCB immediately?

Some servers provide schematic creation, placement, and routing tools, so a larger design request can involve several supported operations. Their availability does not guarantee a correct complete board from a short prompt. You still need to define the circuit requirements and review the electrical and physical design. This guide covers the first connection and edit.

Does a clean DRC report mean the PCB is ready to manufacture?

No. It means the board passed the enabled checks. Fabrication and assembly readiness also depend on the chosen stackup, manufacturing capabilities, and component requirements.

When you are ready to turn the reviewed design into hardware, EBest Circuit (Best Technology) can discuss PCB fabrication and PCBA requirements with you. Contact sales@bestpcbs.com with your KiCad MCP project requirements to discuss manufacturing support.

How Does IPC-SM-840C Apply to PCB Solder Mask?

September 11th, 2026

IPC-SM-840C is the C revision of the specification for qualifying permanent solder mask used on printed circuit boards. It connects the coating’s electrical, physical and environmental performance with its intended application. For your PCB, the practical questions are which mask class applies, how the coating fits the layout, and whether it is compatible with fabrication and assembly. At EBest Circuit (Best Technology), we provide PCB manufacturing and assembly support to help turn those requirements into a buildable board.

Conceptual illustration of IPC-SM-840C solder mask on a printed circuit board

What Is IPC-SM-840C?

IPC-SM-840C addresses the qualification and performance of permanent polymer solder mask, also called solder resist. The coating covers selected copper and laminate surfaces while leaving soldering pads, contacts and other specified areas exposed. It helps protect conductors and define where solder should wet during assembly.

The C revision dates to January 1996, with Amendment 1 issued in June 2000. It is a historical edition, so an existing drawing may name it even when a current material datasheet names a later revision. The standard concerns both material evaluation and the way the mask is used on a board. For example, a coating qualified on a test substrate still needs a suitable application process on the actual copper pattern.

What Do IPC SM 840 Classes T and H Mean?

Class T and Class H distinguish solder mask performance requirements by end-use reliability needs. Class T covers telecommunications and other high-performance commercial or industrial equipment. Class H addresses high-reliability applications where continued operation is critical. For drawings that specify IPC-SM-840C Class T or IPC SM 840C Class H, the required designation should carry through to the selected mask material.

Solder mask classApplication emphasisWhat to specify for your board
IPC SM 840 Class TLong service life in commercial and industrial electronicsRequired revision, compatible mask material and intended assembly conditions
IPC SM 840 Class HHigher assurance where uninterrupted operation is essentialRequired revision and class, with the qualification evidence applicable to that material and process

These letters describe the solder mask requirement. The finished PCB’s IPC-6012 Class 2 or Class 3 requirement is a separate specification covering the rigid board. Keeping both requirements explicit makes the intended coating performance and overall board quality clear.

Which Solder Mask Properties Affect PCB Reliability?

Adhesion, electrical insulation and resistance to processing exposure determine whether the coating can protect the circuit throughout manufacture and use. Colour and surface appearance matter for inspection and product presentation, but the functional properties are the basis for material selection.

Property groupWhat it addressesRelevance to the finished PCB
Adhesion and mechanical integrityBonding to the underlying surface; resistance to cracking or peelingMaintaining coverage around tracks, pads and machined edges
Electrical performanceDielectric strength and insulation resistanceHelping preserve insulation between neighbouring conductors
Soldering and chemical resistanceExposure to soldering heat, fluxes and process chemicalsKeeping the mask intact through board finishing and assembly
Environmental performanceMoisture exposure, thermal changes and electrochemical migrationMatching the material to the board’s service conditions
Cure and surface conditionDeveloped film properties and usable surface qualitySupporting consistent handling and subsequent processing

For our FR4 printed circuit boards, solder mask selection belongs alongside copper layout, surface finish and assembly requirements. A controller with exposed test points has different mask artwork needs from a densely populated communications board, even when both use the same laminate family.

How Does LPI Solder Mask Become a Protective Pattern?

Liquid photoimageable solder mask is applied as a coating and patterned by light exposure and development. A typical LPI soldermask process includes surface preparation, coating, preliminary drying, imaging, development and final cure. The result is a permanent film with openings matched to the circuit artwork.

Surface preparation supports adhesion; imaging and development define the openings; final cure develops the required film properties. Their combined effect explains why the material name alone is only part of the finished-board result. Dry-film photoimageable solder mask offers another material format, with different behaviour over the board’s raised copper features.

The phrase LDI vs LPI solder mask can cause confusion: LPI describes liquid photoimageable material, while laser direct imaging describes an imaging method. An appropriately formulated LPI material can be used with direct imaging. Material selection and imaging compatibility therefore need to be considered together.

What Is the Recommended Thickness for PCB Solder Masks?

The recommended finished thickness is material- and layout-specific; one universal value does not describe every PCB. Solder mask thickness affects protection over copper edges, available clearance and the local surface height around component pads. A patterned PCB is not flat: copper traces, planes and gaps create different coating conditions. Thickness over a conductor and thickness beside it may therefore differ.

Not-to-scale conceptual cross-section showing solder mask covering raised copper traces and laminate

An IPC SM 840 solder mask thickness requirement should identify the measurement location and the agreed finished-film requirement. A value measured over bare laminate is not directly interchangeable with one measured over copper. The material system, copper profile and circuit geometry determine the practical coating window.

This becomes especially relevant on our heavy copper PCBs: taller conductors make edge coverage and coating transitions more demanding. Providing the outer-layer copper requirement with the mask artwork allows these features to be considered together, rather than treating the mask as a uniform flat sheet.

Why Do Pad Openings and Mask Dams Matter?

Pad openings expose the intended solderable surface, while a solder mask dam is the narrow strip of coating between adjacent openings. Registration is the alignment between the mask pattern and the copper pattern. Together, these features influence usable pad area and separation around fine-pitch components.

Conceptual top view of fine-pitch solder pads with separate openings and green solder mask dams

For our HDI boards, the pad pitch, opening size and achievable registration must work together. If a proposed dam is too narrow to manufacture consistently, the layout or opening strategy needs adjustment. The package’s land-pattern requirements remain important, particularly when choosing solder-mask-defined or non-solder-mask-defined pads.

Via tenting is a separate artwork choice: mask covers the via opening rather than filling the hole. Keep probe-access test points exposed, and specify via filling separately where that structure is required. These details help us preserve both assembly access and the intended coverage during DFM review.

How Do Surface Finish and Assembly Affect Mask Selection?

The mask must tolerate the selected board-finishing process and subsequent assembly exposure. ENIG, immersion tin and HASL use different chemical or thermal processing routes. Reflow, wave soldering and cleaning add further conditions after the bare board has been manufactured.

We offer finishes including ENIG, lead-free HASL, OSP, immersion silver and immersion tin. Sharing your intended finish and assembly route helps us discuss the appropriate board construction and mask compatibility. For a mixed SMT and through-hole assembly, the total processing sequence matters more than considering one reflow pass in isolation.

Mask colour can also affect imaging and cure settings within a material family. A green-to-black or green-to-white change is therefore a material/process choice as well as a cosmetic one. Its effect on fine features should be reviewed with the board requirements.

Solder Mask vs Conformal Coating: What Is the Difference?

Solder mask protects selected areas of the bare PCB and defines soldering openings. Conformal coating is normally applied after assembly to protect the populated board from its environment. They occupy different places in the build and can be used together.

Conceptual comparison of solder mask on a bare PCB and a translucent protective coating over an assembled circuit

For an industrial sensor exposed to humidity, the bare board may use solder mask while the completed assembly receives a compatible conformal coating. Connectors and test interfaces can require selective exclusion from that later coating. Adhesion between the two coatings and compatibility with cleaning residues become part of the assembly design.

Our PCB and PCBA services let you discuss bare-board manufacture and assembly as a connected project. Where additional protective coating is required, include that requirement with the assembly information so the intended materials and exposed areas are clear.

IPC SM 840 Latest Version: Is Revision C Still Current?

No. As of September 2026, the IPC document revision table lists revision E, issued in December 2010, after revision D from April 2007. C remains relevant to legacy specifications, but new project documentation should identify the edition actually required.

In the IPC SM 840 family, IPC SM 840C was followed by IPC SM 840D and IPC SM 840E. Revision E’s scope includes flexible cover materials as well as permanent solder mask. The revision letter therefore conveys technical scope, not merely a newer publication date.

If your drawing calls for C and the proposed mask documentation references E, send both with the project files. We can discuss the specified material and manufacturing route with you; any change to the drawing’s requirement should be agreed before production. The selected edition and class provide a clearer requirement than simply writing “IPC solder mask.”

How Can We Support Your PCB Solder Mask Requirements?

We combine PCB manufacturing, DFM support and assembly services, helping you match the solder mask pattern to the actual circuit. Our FR4 capability extends to 32 layers, and our HDI capability includes minimum line/space down to 2/2 mil, subject to materials, stack-up, board dimensions and engineering review. These are circuit-fabrication capabilities; the mask opening and dam requirements are reviewed separately.

For a board specified to IPC-SM-840C, send the Gerber files, fabrication drawing, required class, mask colour, surface finish and any critical pad or via details. Add assembly files when PCB assembly is part of the project. Contact our team at sales@bestpcbs.com or through our PCB manufacturing enquiry page to discuss your board.

What Does IPC-6012 Class II Mean for Your PCB?

September 11th, 2026

IPC-6012 class II identifies a performance level for rigid printed circuit boards used in dedicated-service electronics. Usually written Class 2, it addresses the quality of the manufactured bare board, including its conductors, plated holes, insulation and structural integrity. It is not simply an appearance grade. At EBest Circuit (Best Technology), we manufacture PCBs and help you connect the specified performance class with a practical board construction, so your assembly starts with the right foundation.

Conceptual illustration of IPC-6012 Class II rigid PCB quality with a plated board and inspection coupon

What Is IPC-6012 Class II?

IPC-6012 Class II means the Class 2 requirements within the qualification and performance specification for rigid printed boards. Class 2 serves equipment where dependable operation and an extended service life matter, but uninterrupted operation is not as critical as it is for Class 3 applications. The numeral II does not mean a two-layer board or revision two of the standard.

IPC 6012 class 2 can apply to different rigid constructions, from a double-sided controller board to a multilayer interconnect. Layer count, laminate grade and surface finish still need their own specification. A Class 2 designation therefore answers one important question about acceptance, but does not define every feature of your PCB.

Which Products Are Suitable for Class 2 PCBs?

Class 2 is a relevant starting point for many commercial instruments, communications peripherals and industrial controls whose service requirements match dedicated-service electronics. The application name alone does not determine the class: the consequence of failure and the required operating conditions matter more.

Application exampleWhat the PCB contributesWhat still needs application-specific attention
Commercial measurement instrumentStable connections between sensing, conversion and display circuitsLeakage paths, noise-sensitive layout and calibration requirements
Communications peripheralInterconnects for processing, power and external interfacesControlled impedance, connector loading and signal integrity
Non-safety-critical industrial controllerReliable mounting and connections for control and input/output circuitsTemperature cycling, contamination and terminal mechanical loads
Conceptual industrial controller assembly showing a rigid PCB application, not a customer product or conformity claim

For these types of circuits, our FR4 printed circuit boards provide a manufacturing route from prototypes to multilayer builds. We review the board design against the requested construction; an instrument’s safety function or environmental exposure may require additional requirements beyond a general Class 2 designation.

What Do IPC 6012 Class 2 Requirements Cover?

IPC 6012 class 2 requirements cover the finished bare board’s physical and electrical quality, not just its visible surface. The areas below explain why a board can look acceptable yet still need evidence about its internal connections or insulation.

Quality areaExamples of relevant featuresValue to your product
Conductors and spacingTrace geometry, copper continuity and separationMaintains intended current paths and reduces short-circuit risk
Holes and interconnectionsHole copper, registration and connection to internal landsSupports reliable connections between layers and component leads
Laminate and structureBonding integrity and response to specified thermal stressReduces vulnerability to internal damage during subsequent processing
Solderable surfaces and maskSurface condition, coverage and mask alignmentProvides a suitable foundation for component assembly
Dimensions and flatnessFinished geometry, hole position, bow and twistHelps the board fit fixtures, connectors and the enclosure
Electrical performanceContinuity and insulation-related requirementsChecks conditions that appearance cannot establish

The applicable revision and your agreed drawing determine the actual acceptance limits. Our PCB testing capabilities include AOI, microsection analysis and flying-probe testing. These address different types of evidence; a continuity pass alone does not demonstrate every structural requirement.

Why Are Hole Copper and Annular Rings Important?

A plated hole is an electrical connection through the board, while its annular ring is the copper land around the hole. Their geometry and integrity affect whether a connection remains reliable after soldering and use. Drilling, layer registration and plating all contribute to the finished result.

Conceptual four-layer PCB cutaway with a continuous plated through-hole and annular ring; not to scale

The copper weight chosen for a surface layer is not the same measurement as hole-wall plating thickness. Likewise, a round pad in the design file does not guarantee the same annular ring after drill and registration tolerances. Preserving manufacturing allowance around these features helps avoid late layout changes and marginal interconnections.

For our HDI boards, the connection between a microvia and its target land is also important. A small surface footprint can save routing space, but microvia construction needs its own engineering review; it should not be treated as a scaled-down conventional through-hole with identical behavior.

How Do Laminate and Thermal Stress Affect Reliability?

The laminate must maintain insulation and structural integrity through the thermal conditions relevant to the build. Copper and resin expand differently, so soldering heat places stress on the board and its interconnections. This is why material selection and plated-hole quality work together rather than as separate purchasing choices.

Conceptual rigid PCB in a thermal chamber illustrating thermal exposure; not an actual factory test or a specified IPC test setup

Our high-Tg PCBs are relevant when the assembly and operating conditions call for a suitable higher-Tg laminate. However, Tg alone is not a complete reliability rating: moisture behavior, thermal expansion, board thickness and the soldering profile also matter. A higher-Tg material does not automatically turn a Class 2 board into Class 3.

For your product, the useful distinction is between the specified board qualification evidence and the environment the assembled equipment will actually encounter. Repeated field temperature cycles or a harsh environment may need additional validation even when the bare board meets its agreed acceptance requirements.

IPC 6012 Class 2 vs Class 3: Which Fits Your Application?

The central difference in IPC 6012 class 2 vs class 3 is the required level of service performance and the associated acceptance criteria. Class 3 is intended for applications where continued operation is more critical. It is not simply the same board with a better finish or an extra final inspection.

DecisionClass 2Class 3
Service expectationDependable operation and extended serviceHigher-performance service where continued operation is critical
Design and fabrication impactFeatures must meet the agreed Class 2 requirementsSome features need tighter acceptance conditions and corresponding manufacturing allowance
Project implicationAppropriate when product requirements fit this classNeeds early alignment of design, fabrication and qualification requirements

IPC 6012 class 1 addresses general electronic products and is not a substitute for a required Class 2 build. At the other end, specifying IPC 6012 class 3 does not by itself establish compliance with every medical, automotive or aerospace requirement. Relevant addenda and product-specific obligations can apply. Choosing the class early is more effective than trying to upgrade a completed lot through inspection alone.

How Does IPC-6012 Differ from IPC-A-600 and IPC-A-610?

IPC-6012 defines rigid-board qualification and performance requirements; IPC-A-600 helps interpret printed-board acceptability visually; IPC-A-610 concerns electronic assemblies. These documents address related but different parts of the product, so they are not interchangeable.

A solder joint on a mounted component belongs to the assembly discussion, whereas a plated hole inside the bare board belongs to board fabrication. If your project includes both PCB manufacture and assembly, we can support both stages, but each needs its appropriate acceptance basis. Our IPC-A-600 bare PCB inspection explanation describes how visual and internal observations complement performance requirements.

Does Class 2 Determine Layer Count, Finish or Impedance?

No. Class 2 is not a complete stack-up or electrical design. A board can require controlled impedance, a particular laminate or a specific surface finish in addition to Class 2 acceptance. Those choices come from the circuit and its assembly requirements.

For example, a communications board may need a defined impedance structure, while an industrial control board may place greater emphasis on current capacity and terminal spacing. Both can use a Class 2 acceptance basis without sharing the same construction. We offer FR4 builds up to 32 layers, subject to engineering review. We can discuss the stack-up, routing density and assembly needs together to identify a suitable construction for your design.

Early DFM support helps connect your intended circuit with manufacturable pads, holes and conductor geometry. It also makes special requirements visible before production, rather than leaving them to be inferred from a general class note.

Which IPC-6012 Revision Applies?

The IPC 6012 latest revision listed in the official revision table is IPC-6012F, September 2023, checked on September 11, 2026. The agreed revision for an existing product can differ. The letter identifies the edition; Class 2 identifies a performance level within that edition.

A legacy drawing referring to IPC 6012D class 2 should therefore not be silently treated as a Class 2 callout under revision F. Where your product moves to a newer edition, the affected requirements need to be aligned with the design and manufacturing agreement. Different editions of an IPC-6012 PDF are not interchangeable simply because they discuss the same class.

What Does IPC-6012 Certification Mean?

IPC-6012 certification can refer to different things, including an individual’s training credentials or a manufacturing qualification program with a defined scope. Neither should be confused with the conformity of a particular board lot. The certificate, issuing organization and scope determine what a certification claim actually establishes.

For the PCBs you receive, the useful evidence relates to the agreed board revision, specified class and applicable manufacturing or test records. A company-level quality certificate alone does not replace that product-specific evidence, and a bare-board acceptance result does not prove the completed equipment’s functionality.

How Can We Support Your Class II PCB Project?

We support PCB fabrication, DFM and PCB assembly, helping you carry the intended board requirements from design into a practical build. Our available inspection and test capabilities include microsection preparation and analysis, copper-thickness checks, AOI and flying-probe testing. Tell us which test reports your project needs so we can confirm the test scope and delivery documentation with your build.

Send your board files, fabrication drawing and intended application to sales@bestpcbs.com. At EBest Circuit (Best Technology), we can review your IPC-6012 class II requirements alongside the stack-up, material and assembly needs, so the board specification supports the product you are building.

PCB feed-through card: Vias, Connectors and Filters

September 11th, 2026

A PCB feed-through card can carry power or signals between connections in an equipment assembly, with filtering added where the circuit needs noise suppression. Understanding that electrical path makes it easier to distinguish the board itself from its connectors, plated holes and filter components—and to choose a replacement that preserves the original function.

EBest Circuit (Best Technology) combines PCB fabrication and component sourcing with SMT, through-hole and mixed PCB assembly. For a board combining connector pins and small filter components, this means both assembly methods can be handled within the same project. We also support customer-supplied components, giving you the option to retain specified connectors while arranging the remaining procurement and assembly with us. Contact sales@bestpcbs.com to discuss a suitable build option.

PCB feed-through card

What does PCB feed-through card mean?

The phrase is an equipment-specific description: it identifies a board or assembly by its connection function. It does not specify one universal circuit, connector arrangement or pinout. To understand a particular card, distinguish the complete assembly from the features that form its electrical paths.

The board, connection and filter perform different jobs:

  • The card carries the circuit. Its copper tracks establish connections between terminals or other parts of the equipment.
  • Vias connect copper layers. They let a connection continue through the board thickness.
  • Connectors provide the interface. They join the board or equipment to wiring or a mating assembly.
  • Filter components control noise. Where fitted, they change how unwanted high-frequency energy travels through the connection.

Consider a simple pass-through board connecting an incoming cable to an internal circuit. A connector accepts the cable, copper tracks route its connections, and vias move selected tracks between layers. Adding a feed-through filter to a power connection gives that route a noise-suppression function. These features can work together; they are not alternative names for the same object.

The schematic reveals which arrangement a particular card uses: direct connections, filtered connections, or additional circuitry. That distinction explains more about its operation than the word “feed-through” alone.

Feed-through vias vs. component mounting holes

A feed-through via is a plated electrical connection between PCB layers. A component hole receives a physical lead or pin. The difference is easiest to see around a through-hole connector: its pins enter the component holes, while nearby vias connect tracks or ground areas to another copper layer.

Hole typeWhat occupies the hole?What determines its design?
Plated viaNormally no component leadInterlayer routing, plating and electrical requirements
Plated component holeA component lead or connector pinThe component's pin dimensions and attachment method
Non-plated mounting holeA screw, locating feature or empty clearanceMechanical fit and positioning

For a soldered connector pin, the finished hole must accommodate the lead and the intended solder joint. A via has no inserted pin to accommodate, so its dimensions serve the routing and electrical requirements instead. Selecting one hole size for both jobs can therefore compromise connector fit or waste routing space.

On a through-hole circuit board, the manufacturing drawing therefore needs to distinguish component holes, vias and mechanical holes. This prevents a connector's mounting requirements from being mistaken for ordinary routing-hole dimensions.

PCB feed-through card

What does a feed through connector do?

A feed through connector carries an electrical connection across a physical boundary, such as an enclosure wall. It provides a defined point where external wiring meets the equipment inside. Depending on the design, the internal side connects to another cable, terminals or a PCB.

The connector and the PCB solve different parts of the connection. The connector establishes the mating interface; the PCB routes those contacts onward. A panel-mounted feed-through may be supported by the enclosure, while a board-mounted connector depends on its PCB attachment and any additional mechanical supports. The mounting arrangement determines where mating forces are carried.

For a replacement, pin pitch alone is insufficient. Two connectors with the same spacing can have different keying, contact numbering or mating depths. An apparently matching plug can therefore connect the wrong circuits or fail to engage correctly.

An ordinary conductive feed-through passes the intended electrical connection continuously. Insulation separates adjacent contacts or separates them from the housing; galvanic isolation requires a different circuit arrangement. Filtering and sealing are additional functions of specified products, not inherent properties of every feed-through connector.

When are feed through capacitors needed?

Feed through capacitors are useful when high-frequency noise must be reduced along a power or suitable signal path. In a three-terminal feed-through arrangement, current passes through the component's conductive path, while its capacitance provides a path for noise to ground. The low-inductance structure helps it remain effective at frequencies where a conventional capacitor's parasitic inductance limits suppression.

Choose the connection according to the problem being solved:

  • Noise travelling along a power line: A through connection places the filter in that route. The supply trace is interrupted so that current flows through the component's input and output terminals.
  • Local IC supply-voltage fluctuations: A non-through connection uses the component for bypass decoupling while retaining the main supply trace. Because noise can also continue along that trace, it offers less suppression of escaping noise than the through arrangement.
  • A line carrying useful signals: The filter must pass the required signal spectrum. If unwanted noise lies close to useful signal frequencies, indiscriminately adding capacitance can suppress signal harmonics as well as noise. The filter response must suit both.

For a power-line through connection, first eliminate parts that cannot meet the operating voltage and current. Then compare attenuation over the troublesome frequency range and the voltage drop caused by the component's DC resistance.

A simple voltage-drop example: If a candidate filter has 20 mΩ of DC resistance and carries 2 A, its calculated drop is 40 mV:

Voltage drop = current × resistance = 2 A × 0.020 Ω = 0.040 V.

That is an illustrative calculation, not a rating for a particular product. It shows why a filter can have suitable noise performance yet consume too much of a low-voltage rail's available voltage margin. Select for both electrical delivery and noise suppression.

How do PCB layout and grounding affect feed-through filters?

The filter's ground connection is part of the noise-current path. A long, narrow route to ground adds inductance, making that path harder for high-frequency current to follow. Consequently, the same filter can produce different attenuation on two boards.

Three layout choices have a direct effect:

  • Ground-trace length and width: Short, wide connections reduce the inductance added between the filter's ground pads and the grounding structure.
  • Distance to the ground plane: A via reaching a nearby plane has a shorter connection than one reaching a plane near the opposite board surface. Stackup matters even when the top-view layout looks identical.
  • Ground connections at the component: In a multilayer mounting comparison, connecting both ground sides through vias gave greater attenuation than using a single ground-side via; shorter vias also improved performance. These are results for that arrangement, not a universal via-count rule.

Keep the incoming and outgoing routing distinct around the filter as well. Closely coupled input and output structures can allow some high-frequency noise to couple around the component. Both the through/non-through choice and this input/output routing effect determine whether noise actually follows the intended filtering path.

For a multilayer PCB, the practical priority is to establish the ground-plane position and the filter's connection paths together. Changing the ground-layer depth during a board revision can change filtering behavior even if the component and its surface footprint remain unchanged.

What must match when replacing a feed-through card?

A successful replacement preserves how the card connects, fits and behaves in the equipment. Three differences are especially easy to miss when comparing boards by appearance.

Pin mapping can change without changing the connector outline.

Imagine two boards using the same six-position connector. On one, contact 1 carries supply power; on the other, it carries ground. The plug may fit both perfectly, but the boards are electrically incompatible. Connector orientation and contact numbering must therefore be interpreted from the specified viewing direction, not guessed from a photograph.

A filtered connection can look like a simple pass-through.

Replacing a filter with a copper link preserves DC continuity but removes its intended noise suppression. Even a capacitor with the same nominal capacitance may differ in internal construction, resistance or high-frequency response. A replacement should preserve the relevant electrical characteristics, not merely the marking value.

Mechanical fit includes the assembled components.

A board can match the original outline yet place a connector too high, reverse its mating direction or leave insufficient clearance inside the enclosure. Board thickness, mounting-hole positions and connector location need to work as one assembly.

The original assembly part number and revision provide a useful starting point for these comparisons. When reproducing an obsolete board, concentrate first on its connection map, populated components and assembled geometry. Resolve those differences before treating a similar-looking board as interchangeable.

PCB feed-through card

FAQs About PCB feed-through card

Is a multilayer PCB required for a feed-through card?

No. A simple connection board may use a simpler layer structure. Additional layers become useful when routing density, grounding or signal requirements justify them. The term “feed-through” does not specify a layer count.

Can one card combine through-hole connectors and surface-mount filters?

Yes. Connector pins and small filter components can use different mounting methods on the same board. This calls for mixed assembly rather than treating the whole card as exclusively SMT or through-hole.

Will a continuity test verify the card's filtering performance?

No. Continuity checks whether a conductive path exists. Filtering concerns how the circuit behaves across frequency, so it requires a measurement suited to the noise or signal requirement. Both checks can be useful, but they answer different questions.

Can I supply the connectors for a custom build?

Yes. EBest Circuit supports consignment and partial turnkey assembly, allowing you to supply specified components while we arrange the agreed remaining procurement and assembly. This is useful when a connector must match existing equipment or cable assemblies.

Should I order a bare PCB or an assembled card?

Order a bare PCB when you will install the connectors and other components yourself. Order an assembled card when you need those components fitted. A bare board reproduces the copper and hole structure; the populated components complete the specified circuit.

Planning a custom PCB feed-through card for your equipment? EBest Circuit can manufacture the board and assemble its specified connectors and components, including mixed SMT and through-hole builds. Email sales@bestpcbs.com to discuss turning your board design into an assembled unit ready for your equipment trials.

How Do You Use IPC-A-600 for Bare PCB Inspection?

September 11th, 2026

IPC-A-600 gives PCB manufacturers and customers a common visual reference for judging bare-board workmanship. It is used alongside the agreed performance specification, product class and drawing requirements. At EBest Circuit (Best Technology), we manufacture custom PCBs and provide inspection and testing capabilities that help evaluate the boards before assembly. For your project, the practical question is how these requirements and checks relate to solderable pads, sound interconnections and the circuit you expect to receive.

Conceptual illustration of IPC-A-600 bare PCB inspection under an optical microscope

What Is IPC A 600, and Why Does It Matter for Your PCB?

The IPC A 600 standard is an illustrated acceptability reference for unassembled printed boards. Its title, IPC A 600 Acceptability of Printed Boards, covers the board itself: the conductive pattern, laminate and interconnections that will later support your components. It is not an assembly solder-joint standard.

For a customer, a shared reference makes a quality discussion more specific. A pad, hole or board edge can be evaluated against an agreed requirement instead of an impression that it looks unusual. For us as a fabricator, that same distinction connects the intended board construction with the features that need examination. Appearance is one part of acceptance; measurements and testing supply the additional evidence required by the design.

Which IPC-A-600 Revision Applies to Your Order?

The revision agreed for your order is the applicable baseline. The IPC A 600 latest revision is IPC-A-600M, released in May 2025. A repeat order may still reference an earlier edition; a newly released standard does not automatically change an existing contractual requirement.

Using the IPC A 600 current revision for a new design and maintaining an established revision for an existing product are different decisions. We can discuss the revision stated in your fabrication requirements as part of the engineering review. This helps keep the requested board, inspection expectations and subsequent repeat builds aligned.

An authorized IPC A 600 PDF or printed copy contains the detailed criteria for the selected edition. This article explains their role in PCB manufacturing; the complete standard and your agreed specification remain the references for individual acceptance decisions.

How Do Class 2 and Class 3 Affect PCB Acceptance?

The product class expresses the service expectations behind the acceptance requirements. In an IPC A 600 class 2 vs class 3 comparison, the useful distinction is the intended level of service, not the appearance of the finished board or a universal quality ranking.

Class referenceService expectationMeaning for your board
IPC A 600 class 2Dedicated-service products requiring extended life and continued performanceThe specified Class 2 criteria establish the relevant acceptance baseline.
IPC A 600 class 3High-performance products where continued operation is especially importantThe applicable Class 3 criteria and any additional requirements need to be reflected in the build requirements.

A drawing may use the wording IPC A 600 class II for Class 2. The class, revision and any customer-specific requirements together define what is requested. We can review those requirements against your stack-up and features before manufacture; assigning a class alone does not establish every material, construction or test requirement.

How Does IPC-A-600 Relate to IPC-6012 and IPC-A-610?

IPC-A-600 helps interpret observable board conditions, while the applicable performance specification defines requirements for the board construction. IPC A 600 vs IPC 6012 is therefore a comparison of complementary documents, not two interchangeable inspection options.

DocumentScopeConnection to the product we supply
IPC-A-600Illustrated acceptability of bare printed boardsA common reference for interpreting visible and sectioned board features.
IPC-6012Rigid-board qualification and performance requirementsRelevant to specifying rigid PCB fabrication requirements.
IPC-6013Flexible and rigid-flex board qualification and performance requirementsRelevant to constructions with flexible sections.
IPC-A-610Acceptance of electronic assembliesRelevant after components are assembled onto the PCB.

For IPC A 600 vs IPC A 610, the key boundary is bare PCB fabrication versus electronic assembly. We offer both PCB manufacturing and PCB assembly, so these are distinct stages of a project: board acceptance addresses the substrate and circuitry; assembly acceptance addresses the populated product.

Which Bare-Board Features Affect Assembly Quality?

Pads, conductor geometry, holes and solder-mask openings form the interfaces between a bare PCB and the assembly process. Their condition matters because components must fit, intended soldering areas must remain accessible, and conductors must retain the geometry required by the design.

Conceptual view of bare PCB pads, holes and conductor patterns examined with a magnifier
  • Exposed lands: pad condition and unwanted mask coverage affect the available soldering surface.
  • Conductor patterns: unwanted copper connections or missing conductor material can change the intended circuit.
  • Holes and mounting features: finished dimensions affect lead insertion, mounting and mechanical fit.
  • Board outline and laminate: edge condition and visible material damage can affect handling and fit in the assembly.

Our PCB inspection capabilities include AOI, hole-diameter inspection and dimensional measurement. These methods support different questions: an optical examination locates a visible feature, while a measurement establishes its size or position. For your board, the relevant drawing requirements provide the link between what is observed and what the assembly needs.

What Can Microsection Analysis Reveal Inside Your PCB?

Microsection analysis exposes internal construction that cannot be assessed from a surface photograph. A prepared section can show the relationship between a plated hole, inner-layer copper and the surrounding laminate. That is valuable when the question concerns an interconnection inside the board rather than an exposed pad.

Conceptual PCB microsection showing a plated hole wall and internal copper connections, not to scale

We provide microsection preparation and analysis and copper-thickness testing as part of our PCB testing capabilities. For our HDI boards, the question may involve a microvia interface or an interconnected via structure. The section location and represented construction therefore matter as much as the image itself.

The benefit for your project is evidence about an otherwise hidden feature. A section represents the sampled area; additional sampling or reliability evaluation may be needed for the application’s requirements. The illustration above explains the inspection concept and is not a production micrograph.

How Does Electrical Testing Complement Visual Inspection?

Electrical testing evaluates whether intended nets are connected and separate nets remain isolated under the test conditions. Visual inspection examines physical features. Together they address two different aspects of the bare board: its construction and its circuit connectivity.

Conceptual flying-probe test station contacting separate pads on an unpopulated PCB

Our PCB testing capabilities include flying-probe testing, universal electrical testing and open/short testing. These are directly relevant to finding connectivity faults before components are added. A conductor pattern may appear complete yet contain an open connection; electrical testing addresses that question without relying on appearance alone.

For designs with controlled-impedance traces, we also provide impedance testing. This answers a different question from continuity: whether the specified transmission-line characteristic is achieved. The tests required for a particular board depend on its design and the agreed requirements; an electrical pass is not a substitute for every other specified evaluation.

Why Do Different PCB Constructions Need Different Checks?

Different constructions contain different interfaces and interconnections. The acceptance reference remains useful across them, but the features relevant to a two-layer rigid board are not identical to those in a multilayer HDI or rigid-flex design.

PCB constructionRelevant featuresWhat they mean for your design
FR4 printed circuit boardsOuter patterns, plated holes and the internal connections present in the stack-upComponent mounting and the intended paths between copper layers.
HDI boardsMicrovia interfaces and filled or capped vias where specifiedConnections that support dense routing and fine-pitch component layouts.
Rigid-flex circuitsCoverlay openings, bonded regions and rigid-to-flex transitionsElectrical connections and the mechanical interfaces involved in installation or flexing.

Our FR4 manufacturing capability extends to 32 layers, subject to the stack-up, dimensions, materials and engineering review. As internal connections become more complex, the construction information becomes more important to selecting meaningful inspection evidence. This is why layer count alone is not enough to describe the board we are being asked to manufacture.

How Can Inspection Evidence Help Resolve a Board Concern?

A useful quality discussion connects the observed condition to the affected feature and its requirement. If you have a concern about a supplied board, we can review it with your part information, the location of the feature and the relevant photographs or measurements. That gives both teams a specific technical issue to discuss.

For example, a question about whether a lead will fit a hole calls for finished-hole dimensions and the component requirement. A concern about an internal connection may call for sectioning or electrical evidence instead. The benefit is a response directed at the actual board function, rather than a general judgment based on one photograph. Any proposed change to an agreed acceptance requirement needs customer agreement.

What Does IPC-A-600 Certification Mean for Customers?

IPC A 600 certification refers to personnel training and assessment credentials. It answers a question about knowledge of the standard, whereas inspection and test results answer questions about a particular board or lot. These are different forms of evidence.

For your project, the relevant discussion with us is the required board construction, acceptance basis and available inspection or testing support. Personnel credentials, when required, need separate confirmation of their scope and validity. A credential is not a replacement for evidence about the product being delivered.

How Can We Support Your Next PCB Build?

We combine custom PCB manufacturing, DFM engineering review and PCB testing support. This lets us discuss your acceptance requirements in the context of the actual board, from its stack-up and holes to its surface finish and assembly interfaces.

For an IPC-A-600 question about your next build, contact sales@bestpcbs.com with your fabrication data and the requirements already defined for the project. At EBest Circuit (Best Technology), we can review the design and discuss the applicable inspection and testing needs before manufacture.

Paste Volume Variation PCB: Causes and Printing Fixes

September 11th, 2026

For “paste volume variation PCB” problems, the right correction depends on whether deposits are consistently off target or changing unpredictably. A small aperture that always prints low may need a design change; deposits that deteriorate during a run may need cleaning or better paste handling. Raising pressure for both problems can leave the original cause unresolved.

EBest Circuit (Best Technology) combines PCB fabrication and assembly support with laser-cut, electropolished stencils and solder paste inspection. Smooth aperture walls support paste release, while SPI identifies uneven deposits before component placement. For help matching stencil and inspection requirements to your next assembly, contact sales@bestpcbs.com.

paste volume variation PCB

What Is Paste Volume Variation in PCB Assembly?

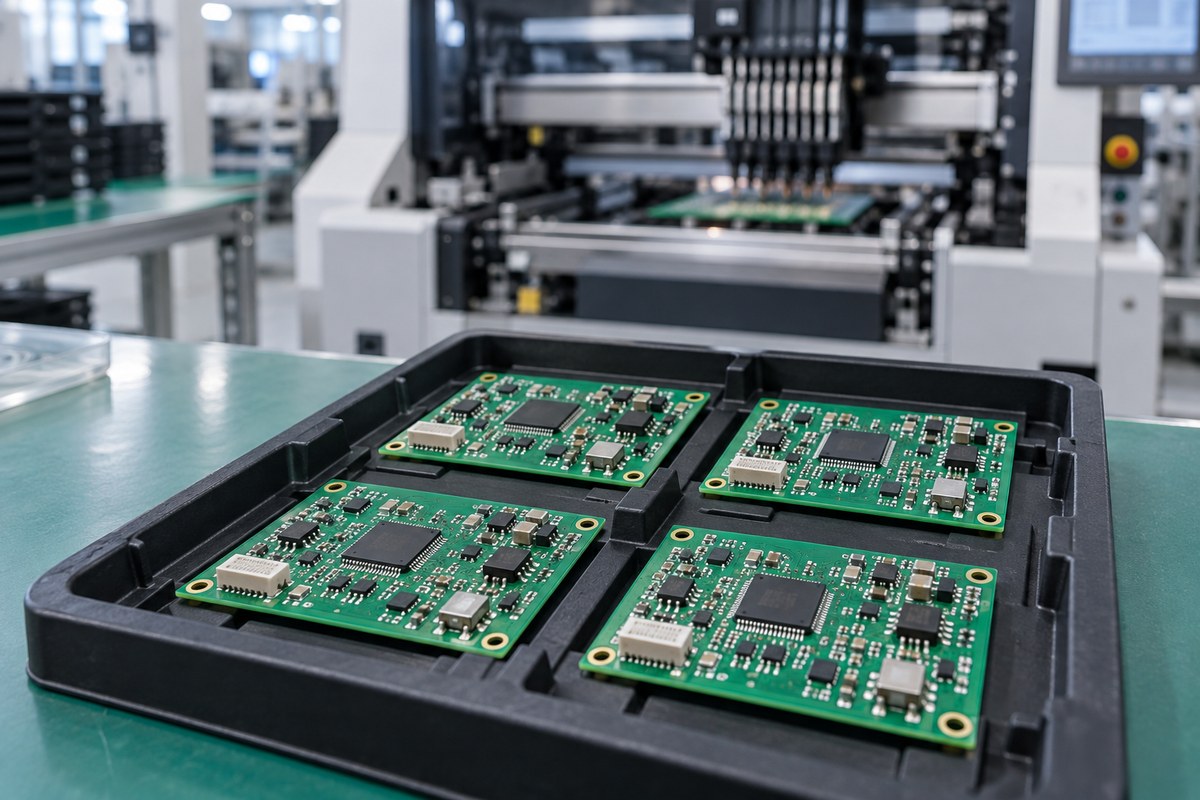
Paste volume variation is the difference between solder paste deposits that should perform consistently. It can occur between equivalent pads on one board, between repeated circuits in a panel, or at the same pad on successive boards.

Different component terminations often need different paste volumes. A connector tab and a small resistor pad should not be compared simply by their measured volume in mm³. Compare each deposit with its own target, then evaluate the spread within groups of similar apertures.

Location and timing help separate the causes. A problem that follows one aperture points toward that opening or its release conditions. A problem covering one panel region points toward local contact or support. A change after a pause points toward restart behavior. These patterns narrow the investigation before printer settings are changed.
How Is Solder Paste Volume Measured with SPI?

In 3D solder paste inspection, the system reconstructs the deposit surface and calculates volume above a reference plane. Volume combines height and footprint: a broad, shallow deposit can contain less paste than its top view suggests.

For a straight-walled rectangular aperture:

Theoretical aperture volume = length × width × stencil thickness

Transfer efficiency (%) = measured deposit volume ÷ theoretical aperture volume × 100

For example, a 0.40 × 0.25 mm aperture in a 0.10 mm stencil has a theoretical volume of 0.010 mm³. If SPI measures 0.009 mm³, transfer efficiency is 90%.

That percentage is meaningful only with its reference. An SPI program may use a specified nominal deposit volume rather than theoretical aperture volume. Keep the reference consistent when comparing results across boards or recipe revisions.

Before treating small differences as printer drift, repeat the measurement on the same deposit. If the reported volume changes appreciably without another print, resolve the measurement or reference issue first. Otherwise, adjusting the printer may compensate for inspection noise rather than improve deposition.

Why Can Average Paste Volume Hide Printing Problems?

High and low deposits can cancel each other in an average. The following hypothetical results all use the same nominal volume:

Set Five measured results Average
A 97%, 99%, 100%, 101%, 103% 100%
B 70%, 85%, 100%, 115%, 130% 100%

Set A spans six percentage points; Set B spans sixty. Both averages are on target, but they describe very different printing behavior. The example does not establish acceptance limits.

Keep two views of the data: the average shows centering, while the distribution shows consistency. A narrow cluster below target calls for correcting a persistent shortfall. A wide cluster calls for stabilizing the process before moving its center. Both volume and spread are used in solder paste performance evaluation.

Also keep critical locations visible. Averaging hundreds of larger deposits with a small fine-pitch group can conceal the group responsible for rejects. Compare similar aperture groups and retain the sequence of prints; a gradual decline is easier to recognize in order than in a combined histogram.

How Do Stencil Thickness and Aperture Design Affect Paste Release?

Stencil thickness sets theoretical capacity, while aperture geometry affects how readily that capacity transfers to the board. A thicker stencil holds more paste but also gives it more sidewall area to separate from.

Area ratio = aperture opening area ÷ aperture sidewall area

For a rectangular opening of length L, width W, and thickness t:

Area ratio = LW ÷ [2(L + W)t]

Using the earlier 0.40 × 0.25 mm opening, increasing thickness from 0.10 to 0.15 mm raises theoretical volume by 50%, but reduces area ratio from approximately 0.77 to 0.51. The larger cavity therefore does not guarantee a proportionally larger deposit. Area ratio and actual transfer efficiency describe different parts of the printing problem.

When small openings print inconsistently, consider reducing local thickness or revising opening geometry to improve release. Enlarging an opening is appropriate only where pad geometry and spacing allow the resulting deposit; it cannot be used indiscriminately around fine-pitch connections.

When larger terminations need more paste, a local step-up region may provide capacity without thickening the fine-feature area. Conversely, a step-down region can serve smaller openings. The step layout must still allow effective blade travel and stencil contact.

EBest Circuit supplies electropolished SMT stencils, including step-up and step-down options. These provide ways to address wall finish and local volume requirements within the stencil design, rather than relying entirely on printer adjustments.

How Do PCB Support and Squeegee Settings Affect Paste Volume?

Restore stable board-to-stencil contact first. An unsupported area can deflect during the print stroke, changing the seal around the apertures. Poor contact lets paste spread underneath the stencil instead of staying within the intended openings. Add or reposition suitable support beneath the affected area, correct clamping that lifts the board away from the stencil, and accommodate underside components in the tooling. This stabilizes the geometry on which pressure adjustments depend.

Use enough pressure to wipe the stencil clean. Too little pressure can leave paste on the top surface after the stroke. Increase it only until the blade produces a clean wipe under the chosen conditions. If excess force is needed, address blade wear, setup, or support rather than continuing to increase pressure.

Match speed to the paste’s filling behavior. The rolling paste bead drives material into the apertures. Changing speed changes both the available filling time and the paste’s response to shear. For a speed-sensitive paste that loses fill at higher speed, a lower setting can help. Other formulations perform well at higher speeds, so “slower is better” is not a universal rule.

Adjust separation for the difficult apertures. The board’s withdrawal from the stencil affects whether the deposit detaches cleanly or stretches and remains partly in the opening. Compare separation settings using the smallest troublesome group, while keeping the print stroke unchanged. Choose the setting that improves release and consistency, rather than automatically selecting the slowest separation.

paste volume variation PCB

How Can You Reduce Paste Volume Variation Across Repeated Prints?

A stable setup can still drift as residue builds up, paste sits idle, or material condition changes. Match the correction to the event that precedes the volume change.

Clear restricted apertures and remove underside residue. If particular deposits fall in volume as prints accumulate, examine those openings for retained material and clean them using the approved stencil-cleaning process. If paste spreads outside the intended footprint, remove underside contamination and restore contact. Shorten the cleaning interval when deterioration repeatedly starts before the next scheduled clean. More frequent cleaning will not repair poor support or an unsuitable aperture.

Prevent the cleaning cycle from introducing another variable. Use a cleaning agent compatible with the paste and avoid flooding the apertures. Complete the required drying stage before printing resumes. If the first print after cleaning is abnormal, correct the cleaning cycle rather than treating that print as ordinary production drift.

Control restart conditions after pauses. Apply the paste supplier’s recommended conditioning or kneading procedure where required, then inspect the restart print before placement. If stoppages are frequent, select a paste whose response-to-pause performance suits those interruptions. Changing the routine or material is more effective than repeatedly accepting a poor first print as inevitable.

Keep material handling consistent. Allow refrigerated paste to reach working temperature in its closed container before opening; opening it cold can introduce condensation. Track opening time and time on the stencil, follow the product’s working-life limits, and replace material that no longer meets those conditions. Do not assume all containers warm at the same rate.

Confirm the improvement over the event that previously triggered the problem. A cleaning adjustment should remain effective through the revised interval; a restart correction should work after a representative pause. Use the same aperture groups and volume references before and after the change so the comparison reflects the process improvement.

What Soldering Defects Can Uneven Paste Deposits Cause?

The effect depends on whether a connection receives too little paste, too much, or an amount that is badly balanced against a neighboring connection.

  • Insufficient solder or open connections: a severely underprinted location may lack enough solder to form the intended connection. Low deposits can also reduce contact margin where termination coplanarity or package warpage is already challenging.
  • Bridging: excess or spread-out paste can connect neighboring lands, creating a path for a solder bridge during reflow. Deposit position and spacing matter alongside volume; a misplaced deposit can cause trouble even when its volume is near target.
  • Tombstoning: unequal deposits on the two ends of a small chip component can contribute to an imbalance in wetting forces, allowing one end to lift.
  • BGA connection defects: uneven deposit heights can leave some balls with less contact than others. Warpage and oxidation can further interfere with coalescence, including in head-in-pillow failures.

These are possible outcomes, not a one-to-one defect code. Tombstoning also depends on thermal and wetting balance, while head-in-pillow involves the interaction between paste, solder balls, and package movement.

Trace the failed connection back to its SPI location. Repeated failures at the same low, high, or imbalanced deposits strengthen the case for a printing correction. If the deposits are consistent at those locations, investigate placement, solderability, and reflow instead of repeatedly changing the stencil.

paste volume variation PCB

FAQs About paste volume variation PCB

What paste volume tolerance should be used in SPI?

Set limits for the relevant aperture and component groups using the intended deposit volume and assembly results. A broad whole-board window can overlook sensitive locations; a tighter window is useful only when measurement repeatability supports it.

Can a deposit pass the volume limit and still be defective?

Yes. It may be offset, smeared, or connected to another deposit. Volume, position, and shape need to be considered together before components are placed.

Should the stencil be replaced if cleaning does not fix low volume?

Not automatically. Separate persistent geometry limitations or damage from paste-condition and printer-setup problems. Replacement makes sense when the opening or stencil condition is the confirmed limitation; an identical new stencil will not resolve an unsuitable design.

Is changing to a finer solder powder always the solution?

No. Powder size is one part of the paste formulation. A candidate paste must demonstrate suitable release through the actual openings, stability through production pauses, and acceptable reflow performance.

Can poor printing be corrected by changing the reflow profile?

A reflow adjustment cannot add missing solder or reposition a misplaced deposit. Correct unacceptable prints before placement, then use the qualified reflow process to form the joints.

For a new build or a repeat order with recurring print rejects, EBest Circuit can bring stencil supply and PCB assembly requirements into the same project discussion. Contact sales@bestpcbs.com to discuss whether your assembly needs a change in local paste volume, more consistent release, or closer inspection of specific component locations.

High-Frequency PCB Manufacturer in Israel: Comparing Capabilities, Quality, and Lead Time

September 11th, 2026

Choosing a high-frequency PCB manufacturer in Israel requires a comparison of the actual fabrication site, RF material controls, stackup ownership, impedance verification, quality records, and delivery route. An Israeli address may identify a factory or a local engineering and sourcing company, so the quotation must name where the bare board will be built.

Use the same released stackup, material requirements, test limits, quantities, and delivery destination when requesting quotes so differences in capability, evidence, and lead time can be compared on equal terms.

High-frequency PCB manufacturers in Israel comparison with RF laboratory equipment and an Israel flag overlay

Which High-Frequency PCB Manufacturers in Israel Can You Consider?

Three Israel-based suppliers have relevant public RF or microwave information, but they do not represent the same supply model. PCB Technologies and Eltek identify manufacturing operations in Israel; APEX PCB presents an Israel-based engineering and supply service supported by a global supplier network.

Manufacturer Address Manufacturing Capabilities Lead Time Advantages
PCB Technologies 7 Ahoman St., Migdal HaEmek, Israel RF and microwave boards, controlled impedance, RF materials, hybrid constructions, prototypes, PCB fabrication, and assembly Confirmed after stackup, material availability, inspection scope, quantity, and assembly review Direct coordination with an Israeli fabrication and assembly operation for engineering-intensive RF projects
Eltek 20 Ben Zion Gelis St., Petah Tikva, Israel Rigid and rigid-flex boards, multilayers, mixed-material low-Dk and low-Df constructions, and RF and microwave applications Quoted for the approved material set, construction, test plan, quantity, and factory loading Israeli PCB manufacturing route for complex rigid, rigid-flex, and mixed-material RF constructions
APEX PCB Kibbutz Hazorea, Israel High-frequency boards, controlled multilayer structures, material selection, impedance modeling, prototype coordination, and quality control Depends on the named partner factory, material allocation, production route, inspection, and international delivery Israel-based technical coordination with access to a wider supplier network for prototype and production sourcing

What Should You Compare Between Israel High-Frequency PCB Manufacturers?

Compare suppliers against one released design and one acceptance package. This exposes differences in factory responsibility, material control, RF engineering, evidence, delivery, and total commercial risk without mixing unlike quotations.

high-frequency PCB manufacturer in Israel, close-up of a high-frequency RF PCB with controlled-impedance traces and RF connectors
  • Fabrication site: Record the factory name, street address, and processes performed there, including lamination, drilling, plating, imaging, etching, surface finish, electrical test, and final inspection.
  • Material control: Compare approved laminate grades, prepregs, bondplies, copper foils, thickness availability, storage, lot traceability, and substitution rules.
  • RF engineering: Confirm who creates the production stackup, calculates impedance geometry, approves trace-width adjustments, designs coupons, and closes technical exceptions.
  • Quality evidence: Define the material certificates, impedance results, microsections, dimensional reports, electrical-test records, and first-article documents supplied with the order.
  • Delivery route: Compare engineering review, material procurement, fabrication, inspection, assembly, freight, customs, and receiving inspection to the same arrival point.
  • Change control: Require written approval before changing the factory, laminate, dielectric thickness, copper foil, stackup, artwork compensation, surface finish, coupon, or test method.

A supplier remains on the shortlist only when its factory, process, evidence, and schedule all match the same project requirements.

Can the Manufacturer Support Your RF and Microwave PCB Requirements?

The manufacturer must support the complete signal path, not only purchase a high-frequency laminate. Review whether its processes can hold the conductor geometry, dielectric construction, plated features, reference planes, and surface interfaces used by the design.

  • Controlled transmission lines: Provide target impedance, tolerance, line type, reference plane, nominal geometry, and affected layers. The factory should return production dimensions before release.
  • Multilayer registration: Ask for achievable layer-to-layer registration on the proposed panel and material system because misregistration changes trace-to-plane geometry and via capture.
  • Advanced vias: Specify finished hole, aspect ratio, via-in-pad filling, blind or buried spans, backdrill depth, stub limit, and sequential-lamination requirements.
  • RF transitions: Mark connector launches, grounded coplanar sections, cavities, plated edges, castellations, and controlled-depth features, then define how their dimensions will be inspected.
  • Surface control: State copper-profile restrictions, finish thickness, solder-mask clearance around RF conductors, flatness, cleanliness, and wire-bondable areas when applicable.
  • Assembly interface: Separate bare-board acceptance from assembled RF performance. Define connector installation, shielding, thermal interfaces, cleaning, and functional or RF tests.

Capability is credible when the factory can return a manufacturable stackup, controlled dimensions, inspection method, and acceptance record for every critical RF feature.

Which Materials and PCB Structures Should RF PCB Manufacturers in Israel Support?

The required materials follow the loss budget, frequency, power, thermal environment, mechanical design, and production volume. A qualified manufacturer should support the exact approved grades or propose alternatives with comparable electrical and processing data for engineering approval.

  • Low-loss hydrocarbon ceramic laminates: Confirm grade, thickness, copper type, bondply, and panel construction for designs where insertion loss and phase consistency matter.
  • PTFE-based materials: Verify specialized drilling, plasma treatment, hole preparation, dimensional compensation, and lamination controls.
  • Low-loss epoxy systems: Use these where the measured performance, multilayer process, assembly conditions, and cost fit the actual frequency and geometry.
  • Hybrid stackups: Combining RF laminate with FR-4 can control cost and thickness, but the factory must manage bonding, resin flow, z-axis expansion, registration, and material movement.
  • Rigid-flex or flex structures: Confirm controlled dielectric, copper, coverlay, bend geometry, launch design, and transition capability at the named facility.
  • Metal-backed structures: High-power RF boards may need heat spreaders, metal cores, coins, cavities, or bonded carriers with separately defined thermal and grounding interfaces.

The approved stackup should name the material grade, dielectric thickness, copper foil, bond system, finished copper, and permitted alternatives. Family names alone do not control the finished board.

How Can You Check Whether a Supplier Can Meet Your Impedance and Signal Loss Requirements?

Set impedance and loss as measurable acceptance requirements before fabrication. The supplier should model the production stackup, obtain approval for geometry changes, and use coupons or board-level structures that represent the critical signal paths.

high-frequency PCB manufacturer in Israel, RF PCB connected to a vector network analyzer for impedance and loss verification
  • Lock the inputs: Use the actual laminate grade, process-relevant Dk, pressed dielectric thickness, finished copper, copper profile, trace width, spacing, solder mask, reference-plane distance, and surface finish.
  • Control artwork changes: Require a returned impedance table showing customer dimensions, production dimensions, calculated values, tolerance, and approval status.
  • Use representative coupons: Place structures on the same panel with the same layer, dielectric, copper, and processing conditions as the board.
  • Separate impedance from loss: TDR verifies characteristic impedance and discontinuities; it does not prove insertion loss, return loss, phase response, or connector performance.
  • Define RF measurements: For loss-sensitive designs, specify frequency range, fixture, de-embedding method, reference structure, sample quantity, limits, and report format.
  • Correlate results: Compare coupon data, board measurements, material lots, microsections, and production geometry.

Accept the lot only against the agreed method and limits. A capability statement or one TDR screenshot cannot replace a controlled measurement plan.

How Should You Verify the Quality of High-Frequency PCBs Before Ordering?

Quality verification should begin with process review, continue through a representative prototype, and finish with evidence tied to the delivered lot. Each checkpoint should show whether the construction matches the RF model and whether the factory can repeat it.

  1. Approve the factory and route: Confirm the fabrication site, material source, stackup owner, subcontracted processes, inspection responsibility, and change-control contact.
  2. Complete RF-focused DFM: Review stackup, impedance tables, via structures, backdrill, registration, copper balance, panelization, finish, solder-mask clearances, and coupons.
  3. Build a representative prototype: Use the intended material family, copper profile, finish, critical geometry, and manufacturing site.
  4. Inspect the first build: Compare dimensions, microsections, impedance data, material records, electrical testing, visual inspection, and required RF measurements with the released limits.
  5. Correlate assembly performance: Document connectors, soldering, fixtures, calibration, test conditions, and limits so failures can be assigned to the board, assembly, or test interface.
  6. Freeze the qualified configuration: Record deviations, tooling assumptions, coupon design, test method, and reporting format. Requalify changes that affect the RF construction.

This sequence turns qualification into a repeatable release process instead of a one-time sample approval.

What Inspection and Test Reports Should You Request From a High-Frequency PCB Manufacturer?

Request reports that close a specific manufacturing risk. The final document package should connect the approved material, finished geometry, electrical continuity, impedance, and RF measurements to the same purchase order and lot.

  • Material records: Require laminate and prepreg grade, lot identity, thickness, copper type, supplier certificate, and approved substitution record.
  • Stackup release: Retain the final construction, pressed dielectric targets, finished copper, impedance geometry, artwork compensation, and approvals.
  • Impedance report: Request coupon ID, layer, line type, target, tolerance, measured values, method, equipment, date, lot association, and result.
  • Microsection report: Define sampled locations and dimensions such as dielectric thickness, copper, plating, registration, hole quality, via fill, and backdrill stub.
  • Electrical-test report: Confirm netlist source, method, quantity tested, criteria, and lot result. Continuity does not replace impedance or RF testing.
  • Dimensional inspection: Identify critical trace, hole, routing, cavity, edge-plating, flatness, and connector-interface dimensions with sampling and limits.
  • RF test report: Specify frequency sweep, fixture, calibration, de-embedding, S-parameters, sample size, environmental condition, and limits before quotation.
  • Nonconformance record: Require deviation approval, failure description, disposition, containment, root cause, corrective action, and affected-lot traceability.

An order-linked evidence pack is more useful than certificates that cannot be matched to the delivered boards.

Which Certifications Should You Check When Comparing PCB Manufacturers in Israel?

Check certifications against the legal entity, factory address, scope, revision, and validity period required by the project. A certificate supports the system named in its scope; it does not replace board-specific material, process, inspection, or test evidence.

  • ISO 9001: Verify the stated quality-management scope and certified site. The order still needs product-specific acceptance criteria.
  • AS9100: Aerospace and defense programs may require a covered entity, traceability, risk controls, configuration management, and customer approvals.
  • ISO 13485: Medical projects should confirm that the relevant PCB or PCBA work falls within the certified medical-device quality scope.
  • IATF 16949: Automotive programs should verify site scope, customer-specific requirements, production controls, and change notification.
  • UL recognition: Match material, flammability, thickness, copper, coating, and marking conditions to the applicable factory file.
  • IPC requirements: State the applicable performance and acceptability documents, class, amendment, and customer additions. IPC documents are product requirements, not factory certifications.

The correct certificate covers the named site and service. The correct board evidence proves compliance with the released order.

How Should You Compare Prototype and Production Lead Times?

Compare schedules by milestone rather than one turnaround number. Prototype work often spends more time on engineering closure, while production adds material allocation, capacity planning, lot inspection, assembly, and shipment controls.

Milestone Prototype Production Buyer Check
Engineering release DFM, stackup, impedance geometry, coupon, and exception approval Frozen revision, approved deviations, tooling, inspection plan, and change controls Date when fabrication can start with no open technical questions
Material allocation Available stock, minimum panel purchase, or expedited procurement Reserved quantity, lot strategy, shelf life, approved alternatives, and reorder coverage Grade, quantity, allocation date, and substitution approval status
Fabrication Small-lot route with required laminations, drilling, plating, finish, and tests Scheduled panels, process capacity, sampling, yield response, and lot release Business days by process, including queue time and weekends
Inspection First-article records and customer review before assembly or shipment Lot reports, deviation closure, source inspection, and release authorization Report date, review owner, approval window, and rework contingency
Delivery Courier shipment or transfer to assembly and engineering evaluation Scheduled freight, customs, buffer stock, receiving, and line-side date Committed arrival location and responsibility for transit delays

Request dates for each milestone and compare the committed arrival date, not a fabrication time that excludes engineering, material, inspection, or transport.

What Factors Can Affect High-Frequency PCB Lead Time in Israel?

Lead time changes when the design requires scarce materials, repeated lamination, specialized drilling or plating, extensive evidence, assembly, or international logistics. The quotation should show which dependency controls the schedule and when it becomes firm.

  • RF material availability: Nonstandard grades, thicknesses, copper profiles, bondplies, and minimum purchase quantities can delay release. Confirm allocated stock rather than catalog availability.
  • Engineering closure: Open stackup, impedance, trace-compensation, panelization, coupon, or finish questions stop the manufacturing clock. Assign owners and approval deadlines.
  • Construction complexity: Hybrid materials, rigid-flex structures, sequential lamination, high layer counts, tight registration, cavities, and controlled-depth features add operations.
  • Via processing: Small drills, laser microvias, via fill, planarization, backdrill, and multiple plating cycles require specific equipment and inspection capacity.
  • Test scope: Impedance coupons, microsections, dimensional layouts, VNA measurements, source inspection, and customer approval add named milestones.
  • Assembly inputs: Component availability, RF connectors, shielding, thermal hardware, stencils, programming, fixtures, and functional testing can control the PCBA date.
  • International delivery: For partner or overseas factories, include export documents, freight, customs clearance, Israeli receiving days, and nonconformance contingency.

A reliable schedule identifies the longest dependency and its owner. A short number without material status, release conditions, and delivery endpoint is not a usable commitment.

What Information Should You Provide When Requesting Quotes From High-Frequency PCB Manufacturers in Israel?

A comparable RFQ gives every candidate the same design revision, material rules, electrical limits, quality evidence, quantity, assembly scope, and delivery destination. Missing inputs force suppliers to quote different assumptions and hide cost or schedule risk.

  • Fabrication data: Supply Gerber or ODB++, fabrication drawing, drill data, netlist, impedance table, stackup, panel requirements, revision, and file-precedence notes.
  • Material specification: Name laminate, prepreg or bondply, dielectric thickness, copper foil and profile, finished copper, approved alternatives, and substitution approval.
  • RF requirements: State frequency, line type, impedance and tolerance, loss or S-parameter limits, power, reference structures, method, fixture, and report format.
  • Mechanical features: Identify thickness, dimensions, hole tolerances, via structures, backdrill, cavities, plated edges, controlled depth, flatness, and connector interfaces.
  • Quality package: Define IPC class or customer criteria, material records, coupons, microsections, dimensional reports, electrical testing, first-article inspection, RF testing, traceability, and retention.
  • Commercial quantities: Request prototype, pilot, and production prices with tooling, testing, engineering, material minimums, assembly, packaging, freight, and taxes separated. Include the BOM, placement data, and assembly drawings when PCBA is required.
  • Delivery terms: Provide the Israeli delivery address, required arrival date, Incoterm, freight method, customs responsibility, partial-shipment rules, and documents.
  • Supplier response: Require factory identity, proposed stackup, material status, production lead time, delivery lead time, exclusions, subcontracted steps, and quotation validity.

Send the same package to each shortlisted high-frequency PCB manufacturer in Israel and compare returned assumptions line by line.

FAQs About High-Frequency PCB Manufacturers in Israel

Q1: When should the manufacturer review the RF stackup?

A1: Request review before routing is frozen. The factory should return the production stackup, controlled-impedance geometry, coupon method, material status, and exceptions before tooling.

Q2: Can the manufacturer change controlled-impedance trace widths?

A2: Only with written approval. The returned impedance table should show customer dimensions, proposed production dimensions, calculated values, tolerances, and affected layers.

Q3: Is a TDR report enough to qualify an RF PCB supplier?

A3: No. TDR checks impedance and discontinuities; it does not prove insertion loss, return loss, phase, material identity, plating reliability, or assembled RF performance.

Q4: Can an RF laminate and FR-4 be combined in one stackup?

A4: Yes, when bonding, resin flow, z-axis expansion, registration, copper balance, and RF performance are validated for the exact construction. The approved stackup should identify every material and interface.

Q5: Should the same factory build prototypes and production boards?

A5: Using one factory reduces transfer variables but is not mandatory. If production moves, freeze the material, stackup, artwork compensation, coupons, tests, limits, and deviations, then requalify the transferred build.

Choose the supplier that can build the released material and stackup, measure the required electrical performance, provide order-linked quality records, and commit to a complete delivery schedule.

If an overseas manufacturing route is acceptable, EBest Circuit is a China-based PCB and PCBA supplier serving international projects. Send your Gerber or ODB++, stackup, RF requirements, quantity, assembly scope, test plan, delivery address, and target date to sales@bestpcbs.com for a free DFM review and quotation.

Thermal Pads: Materials and Selection Guide

September 11th, 2026

In electronic assemblies, thermal pads are preformed thermal interface materials placed between a heat source and a heat sink, cold plate, shield, or chassis. They deform under controlled pressure to replace insulating air gaps with a more conductive path, making them useful where surfaces are uneven or the gap is too large for a thin layer of paste.

A pad is not selected by thermal conductivity alone. Thickness, compression, hardness, contact area, dielectric behavior, surface tack, temperature range, and the PCB’s heat-spreading design all affect the result. This guide explains how to choose and install thermal pads without creating poor contact, board bending, or electrical risk.

Thermal pads positioned between PCB components and an aluminum heat sink

What Are Thermal Pads and How Do They Work?

Thermal pads work by conforming to the microscopic roughness and larger mechanical gap between two surfaces. Their polymer matrix holds thermally conductive fillers, while their softness allows the material to contact both the component and the cooler more completely than air can.

The heat path is normally component package → pad → heat sink or chassis. The pad improves the interface, but it does not create heat-sink capacity by itself. The cooler still needs enough surface area and airflow, and the PCB must move heat away from the component through copper planes, exposed pads, or vias.

Heat flow from a PCB component through a thermal pad into a heat sink

Thermal Pads vs Thermal Paste: Which Interface Should You Use?

The choice between thermal pads vs thermal paste depends mainly on the gap, surface geometry, assembly process, and service requirements. Paste is suited to a very thin interface between closely mated surfaces. A pad is better when a defined gap must be bridged, multiple components have different heights, or production needs a clean and repeatable pre-cut part.

Interface Material Best Fit Gap Handling Assembly Trade-off
Thermal pad Uneven surfaces, height variation, repeatable placement Defined and measurable gaps Clean and reworkable, but thickness must be correct
Thermal paste or grease Closely mated CPU, GPU, or power-package surfaces Very thin bond lines Low interface thickness, but application amount and pump-out must be controlled
Gap-filler gel or putty Variable gaps and complex component topography Conforms to irregular three-dimensional spaces Dispensing can be automated, but volume and cure behavior require process control
Phase-change sheet Thin, controlled interfaces that soften at operating temperature Small gaps with specified clamping pressure Easy handling, but suitability depends on the package and operating profile

Do not substitute one interface material for another only because its advertised W/m·K value is higher. Compare thermal impedance at the intended thickness and pressure, then check electrical insulation, temperature cycling, rework, and contamination requirements.

What Are Thermal Pads Made Of?

Most conformable thermal pads use silicone or acrylic elastomers filled with thermally conductive ceramic particles. The filler moves heat through the pad, while the polymer provides flexibility and electrical insulation. Silicone-free pads are available when siloxane contamination, optical surfaces, relays, or downstream coating and bonding processes create concern.

Graphite sheets form another category. They can spread heat efficiently along the plane of the sheet but may be electrically conductive and may behave differently through their thickness. Material names alone therefore do not define performance; the supplier’s datasheet and the actual assembly stack must be reviewed together.

Different thermal pad materials and thickness measurement tools

Which Specifications Matter When Choosing a Thermal Pad?

The most useful specification is the one that predicts performance in the real joint. Bulk thermal conductivity is important, but it does not include every contact resistance or the effect of thickness and compression.

Specification Why It Matters What to Verify
Thermal conductivity Describes heat conduction through the bulk material Test method, direction, temperature, and comparison basis
Thermal impedance or resistance More directly reflects the complete interface at a stated condition Pad thickness, area, pressure, surface finish, and test setup
Thickness and tolerance Determines whether the pad bridges the gap without excessive stress Minimum and maximum assembled gap across production tolerances
Hardness and compression Control conformability, contact, and mechanical load on the PCB Compression-deflection curve and allowed clamp force
Dielectric properties Prevent unintended electrical contact when isolation is required Dielectric strength, volume resistivity, and puncture risk
Temperature and aging Affect long-term softness, adhesion, and thermal stability Operating range, cycling data, outgassing, and material compatibility

How Do You Choose the Correct Thermal Pad Thickness?

Choose pad thickness from the worst-case assembled gap, not from a visual estimate or the uncompressed gap alone. Measure the distance between the component surface and the cooler, include package-height, PCB-flatness, enclosure, fastener, and tolerance variation, then select a pad that reaches the supplier’s specified compression window without overloading the assembly.

  1. Measure the gap at several points or derive it from the mechanical stack drawing.
  2. Calculate minimum and maximum gaps across component, PCB, heat-sink, and fastener tolerances.
  3. Check the pad’s thickness tolerance and compression-deflection curve.
  4. Confirm that clamp force will not bow the PCB, crack a package, or reduce connector alignment.
  5. Build representative samples and verify contact pattern and temperature under load.

A pad that is too thin may leave air gaps. A pad that is too thick or too hard can prevent the cooler from seating, reduce contact on neighboring components, or bend the board. Stacking multiple pads is normally a poor uncontrolled substitute for selecting the correct thickness.

Where Are Thermal Pads Used in GPUs, CPUs, Laptops, and PCB Assemblies?

Thermal pads for GPU assemblies are commonly used over memory devices, VRM power stages, and other components that sit below the cooler plate. The bare GPU die often requires the OEM-specified paste or phase-change interface instead, because the bond line is much thinner and heat flux is concentrated.

Thermal pads for CPU applications should follow the processor and cooler manufacturer’s interface recommendation. A conventional soft gap pad should not automatically replace paste on a closely mated CPU heat spreader, but pads can be appropriate for nearby power components, embedded systems, and mechanically defined enclosure-to-package gaps.

Thermal pads for laptop cooling must match the original component locations, thicknesses, and compression behavior. Using one thickness everywhere can lift the heat pipe away from the CPU or GPU die. Industrial PCB assemblies also use pads between power devices, shields, chassis walls, battery modules, LED assemblies, and heat spreaders.

How Should Thermal Pads Be Installed?

Install a thermal pad on clean, dry surfaces with the protective liners removed at the correct step and the pad aligned to the intended contact area. Avoid touching the active surface, stretching the material, trapping debris, or allowing the pad to cover connectors and components that should remain exposed.

  1. Power down and follow the product’s electrical safety procedure.
  2. Remove old interface material without scratching the component or cooler.
  3. Clean both mating surfaces with a compatible method and allow them to dry.
  4. Cut or use a die-cut pad that covers the heat-transfer area without excessive overhang.
  5. Remove the first liner, place the pad without stretching, then remove the second liner.
  6. Lower the cooler evenly and tighten fasteners in the specified sequence and torque range.
  7. Check temperatures, contact pattern, and mechanical seating on a representative assembly.
Technician measuring and installing a thermal pad on PCB power components

What Problems Cause Poor Thermal Pad Performance?

Poor thermal performance usually comes from incomplete contact or an unsuitable mechanical stack rather than from the pad simply being “low quality.” Common failure causes include:

  • Incorrect thickness, hardness, or compression range
  • Protective liner left on one side
  • Dust, oil, or particles trapped at the interface
  • Pad area that is too small, misaligned, or obstructed
  • Uneven fastener torque or warped heat-sink surfaces
  • Using an electrically conductive sheet where insulation is required
  • Material aging, tearing, pump-out of an adjacent paste, or chemical incompatibility
  • Assuming a high W/m·K rating guarantees low total thermal resistance

Inspect the imprint after a controlled assembly trial. A uniform contact pattern helps reveal whether the pad is reaching both surfaces, while thermal testing confirms whether the complete path works under realistic power and airflow.

How Do Thermal Pads Affect PCB and Heat-Sink Design?

A thermal pad is only one element of the thermal network. Heat must first leave the semiconductor junction and package, then spread through package lands, PCB copper, and possibly thermal vias before it reaches the interface and cooler. A bottleneck at any stage can limit the benefit of a higher-performance pad.

Coordinate the PCB, cooler, and enclosure as one tolerance stack. For effective PCB heat sink design, check keepouts, pad overlap, screw locations, component height, board stiffness, copper spreading area, via placement, creepage and clearance, and access for assembly or rework. Thermal simulation and prototype testing should use the actual pad thickness and pressure-dependent interface data whenever available.

FAQ About Thermal Pads

1. Are thermal pads better than paste?

Neither is universally better. Pads are cleaner and more repeatable for defined gaps or components with different heights. Paste usually suits very thin interfaces between closely mated surfaces. Compare the complete joint’s thermal resistance, gap tolerance, pressure, insulation, aging, and assembly process instead of comparing W/m·K alone.

2. Can thermal pads be reused?

Reuse is risky because a removed pad may be torn, contaminated, permanently compressed, or no longer aligned with the original contact area. Follow the equipment and material supplier’s service instructions. For controlled production or critical repairs, a new pad of the specified material and thickness is usually the safer choice.

3. Can you stack thermal pads?

Stacking adds interfaces, changes compression, and makes the final thickness less predictable. It may also let layers shift during assembly. Use a single pad designed for the measured gap whenever possible. If stacking is proposed, the complete joint needs engineering validation rather than assumption.

4. Do thermal pads conduct electricity?

Many ceramic-filled silicone or acrylic pads are electrically insulating, but not every thermal sheet is. Graphite and metal-based materials may be electrically conductive. Check dielectric strength, volume resistivity, edge exposure, puncture risk, and the supplier’s datasheet before placing a material near live conductors.

5. What are IC package thermal pads?

The phrase may refer either to a separate thermal interface pad above an IC package or to the exposed thermal land beneath a package such as a QFN. These are different structures. The external pad bridges the package-to-cooler gap; the PCB land is soldered and often connects to copper and vias for heat spreading.

6. How can you tell whether a thermal pad is too thick?

Warning signs include a cooler that does not seat, excessive fastener force, PCB bowing, reduced contact on neighboring components, or a worse temperature result after replacement. Confirm the mechanical stack and inspect the contact imprint rather than judging only by whether the pad visibly compresses.

How Can EBest Circuit Support the PCB Side of Thermal Management?

A reliable thermal path starts with coordinated mechanical, material, and PCB decisions. At EBest Circuit, we can review the manufacturability of copper spreading areas, thermal-via structures, stackups, board materials, and component land patterns as part of a PCB project. Send us your Gerber files, stackup, assembly drawing, component power information, cooler interface requirements, and quantities at sales@bestpcbs.com for engineering review and quotation.

Half Wave Rectifier: Circuit, Waveform, Formula & PCB Layout

September 11th, 2026

A half wave rectifier converts one half of an AC waveform into pulsating DC, normally with one series diode. It is simple and inexpensive, but it leaves a full line-cycle gap between output pulses, so ripple and transformer utilization are worse than in a full-wave circuit.

This guide explains the circuit and waveform, separates the formulas for unfiltered and capacitor-filtered outputs, and shows how diode ratings, charging current, and PCB layout affect a practical design.

Half Wave Rectifier circuit board, transformer, capacitor, and oscilloscope waveform

What Is a Half Wave Rectifier?

A half wave rectifier is a one-direction AC-to-DC conversion stage that passes either the positive or the negative half-cycle and blocks the other half-cycle. The result is unidirectional voltage, but it is not smooth DC unless a filter and, where required, a regulator are added.

The basic circuit needs an AC source, one rectifier diode, and a load. A transformer may provide isolation and change the voltage before rectification. A reservoir capacitor can then store energy between the conducting peaks. The Analog Devices half-wave rectifier definition also notes a theoretical maximum rectification efficiency of about 40.5% for the basic circuit.

Because only half the input waveform delivers energy, this topology is best suited to low-power auxiliary rails, signal detection, simple chargers with proper current control, and circuits where cost or part count matters more than ripple and transformer utilization.

How Does a Half Wave Rectifier Circuit Work?

A half wave rectifier circuit works by forward-biasing its diode during one AC polarity and reverse-biasing it during the opposite polarity. With the diode oriented for positive rectification, current flows through the load on positive half-cycles and stops on negative half-cycles.

  1. Positive half-cycle: the diode anode is more positive than its cathode, so the diode conducts after the input exceeds its forward voltage.
  2. Peak region: load current follows the source in an unfiltered circuit; with a capacitor, a short charging pulse replenishes the stored energy.
  3. Negative half-cycle: the diode is reverse-biased and blocks current, so an unfiltered load voltage falls to zero.
  4. Next positive half-cycle: conduction starts again, producing one output pulse per AC cycle.

The diode band marks the cathode and must agree with the intended output polarity. Our guide to diode direction and current flow explains how the schematic symbol, package marking, and PCB footprint should correspond.

Half Wave Rectifier Diagram

A half wave rectifier diagram contains one diode in series with the load and a return path to the AC source. In the positive version below, D1 points from the source toward the load, so the right side receives positive pulses.

Half wave rectifier diagram with AC input, diode D1, load, and pulsating DC output
  • AC input: the source may be an isolated transformer secondary or another AC signal that meets the circuit ratings.
  • D1: the diode provides one-way conduction and must withstand forward current, surge current, and reverse voltage.
  • Load: the load sets the current and determines whether the pulsating output is usable without filtering.
  • Return path: this closes the current loop and should be clear in both the schematic and PCB layout.

Reversing D1 creates a negative half-wave output. The topology is unchanged; only the passed polarity changes.

Half-Wave Rectifier Waveform

A half-wave rectifier waveform shows every accepted half-cycle at the output and a zero-voltage interval during every blocked half-cycle. A 60 Hz input therefore produces 60 output pulses per second; a 50 Hz input produces 50 pulses per second.

Half-Wave Rectifier Waveform comparing sinusoidal AC input with positive rectified output pulses

The real pulse peak is lower than the transformer-secondary peak by the conducting diode’s forward voltage and any source drop. A silicon diode may lose roughly 0.6–1.0 V at practical current, but the correct value must come from its datasheet curve at the expected current and junction temperature.

Adding a capacitor changes the output from separated half-sine pulses to a DC level with sawtooth-like droop. It does not double the recharge frequency: a half-wave reservoir still receives only one charging opportunity per line cycle.

Half Wave Rectifier Formula

The standard half wave rectifier formula set below applies to an ideal sinusoidal source, an ideal diode, and a resistive load without a smoothing capacitor. Let Vm and Im be the output peak voltage and current.

Quantity Ideal formula Meaning
Average DC output voltage VDC = Vm / π ≈ 0.318Vm Average of the unfiltered positive half-sine over one complete cycle
RMS output voltage VRMS = Vm / 2 Heating-equivalent value of the complete rectified waveform
Average load current IDC = Im / π Average current for a resistive load
RMS load current IRMS = Im / 2 RMS current for loss and heating calculations
Ripple factor r ≈ 1.21 AC ripple divided by DC content for the unfiltered ideal output
Maximum rectification efficiency η ≈ 40.6% The theoretical limit of the basic resistive-load circuit

For a 12 V RMS transformer secondary, Vm = 12 × √2 = 16.97 V. The ideal unfiltered average is therefore 16.97 / π = 5.40 V, while the ideal RMS output is 8.49 V. Do not use the 5.40 V result for a capacitor-input supply: the capacitor charges near the peak, so that case needs a different calculation.

Half Wave Rectifier With Capacitor Filter

A half wave rectifier with capacitor filter charges the capacitor near each input peak and lets the capacitor supply the load while the diode is off. The output rises close to the input peak minus diode and source losses, then falls between peaks as the capacitor discharges.

A useful first estimate of peak-to-peak ripple is:

ΔV ≈ Iload / (fline × C)

For 100 mA, 60 Hz, and 1000 µF, the estimate is 0.1 / (60 × 0.001) = 1.67 V peak-to-peak. With a 12 V RMS secondary and an assumed 0.8 V diode drop, the capacitor charges to about 16.2 V and the average may be roughly 15.3 V before transformer regulation and source resistance are included. At 50 Hz, the same load and capacitor produce about 2.0 V peak-to-peak ripple.

This shortcut is suitable for an initial capacitor value, not final verification. ESR, ripple-current rating, tolerance, temperature, diode conduction angle, transformer impedance, load transients, and inrush current all affect the real waveform. The onsemi single-diode bulk-capacitor design note uses input power, line frequency, peak voltage, and minimum bulk voltage for a more complete calculation.

The diode reverse-voltage check also changes. With a resistive load and no capacitor, peak inverse voltage is approximately Vm. With a charged reservoir capacitor, reverse stress can approach 2Vm, so the selected repetitive reverse-voltage rating needs appropriate margin.

How Does a Half-Wave Rectifier Differ From a Full-Wave Rectifier?

A half-wave rectifier uses one input half-cycle and produces one recharge pulse per cycle, while a full-wave rectifier uses both half-cycles and produces two recharge pulses per cycle. At the same line frequency, the full-wave circuit therefore has a shorter capacitor-discharge interval and usually needs less capacitance for the same ripple target.

Feature Half-wave rectifier Full-wave bridge rectifier
AC half-cycles used One Both
Typical diode count One Four, with two conducting at a time
Ripple frequency Same as input frequency Twice the input frequency
Ideal maximum efficiency About 40.6% About 81.2%
Typical reason to choose it Minimum part count at low power Lower ripple and better transformer use

Use our detailed full wave rectifier guide when the design needs both half-cycles, bridge-current paths, or a lower-ripple reservoir supply.

Where Is a Half Wave Rectifier Used?

A half wave rectifier is used where the load is small, the waveform itself carries information, or one diode is more valuable than low ripple. Practical examples include AC presence detectors, envelope or peak detectors, low-current auxiliary bias rails, simple polarity-dependent sensing, educational circuits, and low-duty charging stages with suitable current and voltage control.

It is usually a poor choice for a regulated rail that supplies a processor, radio, motor driver, or other load with meaningful continuous current. Those loads generally benefit from full-wave rectification, a switching stage such as a buck converter, or a purpose-designed offline power supply.

A single diode is also common in precision signal processing, but a low-level signal may be smaller than the diode’s forward drop. An active or precision half-wave rectifier uses an operational amplifier to compensate for this error, as shown in the Analog Devices MT-212 tutorial.

What Are the Main Advantages and Disadvantages?

The main advantage is a one-diode power path; the main disadvantages are high ripple, DC bias in the transformer, poor transformer utilization, and low theoretical conversion efficiency. These trade-offs make the topology attractive only when simplicity outweighs output quality.

  • Advantages: low component count, easy polarity selection, simple analysis, and low PCB area for light loads.
  • Disadvantages: one long discharge interval per cycle, larger capacitor for a given ripple target, pulsed charging current, possible transformer core bias, and more difficult regulation as load increases.
  • Decision boundary: choose half-wave only after confirming ripple, peak current, thermal rise, reverse voltage, and source utilization are acceptable.

How Should You Select the Diode and Capacitor?

Select the diode from repetitive reverse voltage, average forward current, surge current, forward drop, recovery speed, leakage, temperature, and package thermal limits; select the capacitor from capacitance, working voltage, ripple-current rating, ESR, tolerance, temperature, and life.

Part Parameter to verify Practical check
Rectifier diode VRRM, IF(AV), IFSM, VF, recovery, leakage, junction temperature Check steady load, capacitor-charging peaks, turn-on surge, and the highest reverse voltage
Reservoir capacitor Capacitance, voltage, ripple current, ESR, tolerance, temperature, endurance Calculate ripple, then verify heating and life at the actual ambient and load profile

For line-frequency, low-current prototypes, the Vishay 1N4007 is a concrete through-hole example rated 1 A and 1000 V in a DO-41 package. The onsemi MRA4007T3G is a surface-mount standard-recovery example rated 1 A and 1000 V in SMA, with a 30 A surge rating under its stated test conditions. These ratings do not make either device automatically suitable: temperature derating, repetitive charging pulses, board cooling, certification, and the complete datasheet remain part of selection.

Fast-switching or high-frequency sources need a diode with suitable reverse-recovery behavior. Low-voltage circuits may favor a Schottky diode for lower forward drop, but reverse leakage and voltage rating become more important at elevated temperature.

How Should a Half Wave Rectifier Be Laid Out on a PCB?

Lay out a half wave rectifier by keeping the source–diode–capacitor charging loop short and wide, placing D1 and C1 close together, and routing the load return so charging pulses do not corrupt sensitive ground references. The highest di/dt occurs when the diode briefly recharges the reservoir near the AC peak.

PCB layout concept for a half wave rectifier showing a short charging loop around diode D1 and capacitor C1
  • Place by current path: keep the AC input, diode, and reservoir capacitor physically close.
  • Size copper for pulses: do not size the trace only from average load current; include charging peaks and temperature rise.
  • Separate returns: join the high-current rectifier return and sensitive circuit ground at a controlled point.
  • Show polarity: make the diode cathode, electrolytic polarity, connector pinout, and output polarity unambiguous on silkscreen and assembly drawings.
  • Manage heat: provide copper area and spacing based on component loss, package limits, and neighboring heat sources.
  • Provide test access: add points for AC input, rectified node, output ground, and filtered DC.

If the source is connected to hazardous voltage, isolation, fusing, surge protection, creepage, clearance, material group, pollution degree, altitude, and touch safety must be determined from the applicable product standard. A generic blog value is not a substitute for that assessment.

How Can You Test and Troubleshoot the Circuit?

Test a half wave rectifier by confirming component polarity first, measuring AC input and DC output second, and then checking ripple, diode temperature, charging current, and reverse voltage under the real load. Use appropriately rated isolated instruments and probes whenever the source can be hazardous.

  1. Power off: inspect the diode band, capacitor polarity, connector orientation, solder joints, and shorts.
  2. No load: verify the secondary RMS voltage and the rectified peak without assuming the transformer’s nameplate value is exact.
  3. Rated load: record average DC voltage and ripple peak-to-peak at minimum and maximum input.
  4. Current and heat: check diode surge at startup, steady temperature after thermal equilibrium, and capacitor ripple current.
  5. Fault response: test expected open-load, short-load, reversed-connection, and brownout behavior only with suitable protection and a controlled test plan.

Zero output commonly indicates a reversed or open diode, an open source path, or incorrect measurement reference. Excessive ripple points to insufficient capacitance, high ESR, an overloaded output, low input voltage, or missed conduction. A hot diode usually indicates excessive average current, narrow high-current charging pulses, poor thermal layout, or an underrated package.

FAQ About Half Wave Rectifiers

What is the main disadvantage of a half wave rectifier?
The main disadvantage is high ripple because the load receives energy during only one half-cycle and waits one full AC period for the next charging peak.
Does a half wave rectifier change AC frequency?
No. Its output pulse frequency equals the AC input frequency: 50 Hz produces 50 pulses per second and 60 Hz produces 60 pulses per second.
Can a half wave rectifier charge a battery?
It can be part of a low-current charger, but the battery still needs the correct voltage limit, current limit, reverse-current protection, charge profile, and safety controls for its chemistry.
Can a half wave rectifier power a phone?
Not by itself. A phone supply requires safe isolation where applicable, regulated output, low ripple, current capability, transient protection, and the correct charging interface.
How do you reduce ripple in a half wave rectifier?
Increase reservoir capacitance, reduce load current, or use a full-wave topology; then verify capacitor ripple current, inrush, diode stress, and regulator headroom.
Does a half wave rectifier work with DC input?
With DC input it acts only as a series polarity diode: it passes one polarity and blocks the other, so there is no rectification cycle.

When Is a Half Wave Rectifier Ready for PCB Production?

A half wave rectifier is ready for PCB production only after its input range, load current, ripple target, diode reverse and surge ratings, capacitor stress, thermal rise, safety requirements, and test points have been verified together. A circuit that works at no load can still fail when the capacitor draws short charging pulses or when the transformer voltage changes with load.

At EBest Circuit, we can review the rectifier current path, polarity markings, copper allocation, component footprints, thermal spacing, and test access before PCB fabrication and assembly. Send your Gerber files, BOM, input range, load current, ripple limit, and test requirements to sales@bestpcbs.com for a project-specific review and quotation.

PCB and PCBA manufacturer USA: Compare Your Options

September 10th, 2026

For a PCB and PCBA manufacturer USA buyers can work with directly, options include Sierra Circuits, Gorilla Circuits, and Cirexx. These companies offer domestic fabrication and assembly, with services covering standard FR4 prototypes, complex multilayer boards, and specialized constructions. Small-order availability and HDI capability help distinguish the services within that market.

For projects that allow overseas production, EBest Circuit (Best Technology) combines PCB manufacturing, component sourcing, and assembly in China. Our capabilities include FR4 boards up to 32 layers and BGA assembly down to 0.25 mm pitch, supporting projects from bare-board prototypes to populated assemblies. Discuss your US project with our team at sales@bestpcbs.com, or arrange a factory visit to see our manufacturing operations firsthand.

PCB and PCBA manufacturer USA

US PCB Manufacturers Offering Fabrication and Assembly

Sierra Circuits, Gorilla Circuits, and Cirexx each provide both PCB fabrication and assembly. Their service ranges cover different board technologies and production needs.

Manufacturer PCB manufacturing Assembly services
Sierra Circuits Standard rigid FR4 and custom advanced boards, including HDI In-house assembly and component procurement
Gorilla Circuits Multilayer boards, hybrid constructions, and semiconductor test boards In-house assembly, parts procurement, and testing options
Cirexx Rigid, flex, rigid-flex, HDI, and RF/microwave boards Turnkey, partial turnkey, and consignment assembly

Sierra Circuits offers a defined route for conventional prototypes through Turnkey PRO, which combines rigid-board fabrication, parts, and assembly. More complex constructions use its custom services.

Gorilla Circuits fabricates and assembles boards at its San Jose, California campus. Its semiconductor test work includes final-test and probe-card boards, making this a relevant area of experience for buyers sourcing complex test hardware.

Cirexx combines fabrication and assembly within the same facility. Flex and rigid-flex assembly are particular areas of specialization, alongside rigid-board and HDI work.

Do All PCB Manufacturers Offer Assembly?

No. A PCB fabrication order normally supplies bare boards; assembly adds the components. Some manufacturers provide both services, while others specialize in one stage.

  • PCB fabrication: bare boards ready for component assembly.
  • Consignment assembly: assembled boards using customer-supplied materials.
  • Full turnkey PCB assembly: fabrication, component purchasing, and assembly managed by the supplier.

An assembler can also purchase bare boards from a fabrication partner. Consequently, turnkey service does not necessarily mean both processes happen in the same factory.

If you already have an assembly partner, a specialist bare-board manufacturer may fit your project well. If you need finished assemblies and want one point of coordination, a fabrication-and-assembly provider can handle the transition between the two stages.

US Manufacturing vs. Overseas Supply to the USA

US production offers proximity; overseas production broadens the manufacturing options available to US buyers. The balance changes with the way a project is developed and ordered.

Consideration US manufacturing Overseas supply to the USA
Factory access Easier domestic visits and sample exchanges Visits require international travel
Engineering communication Greater overlap with US working hours Responses span different working hours
Shipping Domestic transport to the customer International transit before US delivery
Repeat orders Convenient for closely coordinated local production Can suit scheduled orders with planned shipping

During active development, proximity can be valuable. A team making frequent revisions may benefit from easier sample exchanges and direct factory interaction. The relevant schedule is the complete cycle from placing a build to evaluating the hardware.

For a stable design, manufacturing fit becomes more prominent. Materials, copper construction, component availability, and the supplier's ability to repeat the build can matter more than how often the team can visit. Overseas production is worth considering when international transport fits that schedule.

Neither location guarantees a lower total price. Compare equivalent finished boards: the same materials, components, assembly scope, and delivery destination. A bare-board quotation and a complete PCBA quotation cover different purchases.

Which US PCB and PCBA Manufacturers Accept Small Orders?

Sierra Circuits, Cirexx, and PCB Unlimited offer services for prototype or low-volume assembly. Their small-order arrangements differ:

Provider Small-order service Relevant option
Sierra Circuits Turnkey PRO: generally 2–100 assembled boards, depending on the design Standard rigid FR4 turnkey builds
Cirexx High-mix, low-quantity assembly; prototype through medium volume Custom rigid, flex, and rigid-flex projects
PCB Unlimited USA assembly service with no minimum order quantity Turnkey or customer-supplied-material assembly

PCB Unlimited offers US assembly services. Sierra and Cirexx also provide in-house board fabrication. For Sierra, confirm availability before planning a one-board assembled order.

A small quantity can still involve a custom board. A five-board rigid-flex project or a four-layer PCB with a specified stackup may need a custom service rather than a standard prototype package.

Small runs also share production preparation across fewer finished boards. Stencil preparation and machine programming are needed even for a short run, so doubling the assembled quantity does not necessarily double the total price. When several engineers need hardware simultaneously, pricing the actual number of working samples can be more useful than starting with the smallest possible order.

PCB and PCBA manufacturer USA

Which US Manufacturers Offer HDI PCB Fabrication and Assembly?

Sierra Circuits and Cirexx offer both HDI fabrication and assembly. Their capabilities include the board interconnections and component assembly needed for dense designs.

Manufacturer HDI fabrication Assembly support
Sierra Circuits Custom HDI boards with advanced via structures Turnkey HDI assembly with component sourcing
Cirexx Laser-drilled microvias, blind/buried vias, sequential lamination, and via-in-pad Double-sided HDI SMT/BGA assembly

Sierra's HDI projects use its custom manufacturing route. The standard Turnkey PRO package excludes HDI and multiple laminations, so it is a separate service from the company's advanced-board offering.

Cirexx combines HDI fabrication with dense assembly work. Its fabrication processes include laser direct imaging and controlled-depth drilling, while its assembly service covers double-sided SMT/BGA builds and flex or rigid-flex boards.

For a compact BGA board, this combination is important: the fine-pitch package must be supported by a manufacturable routing and via structure beneath it. Choosing a supplier that handles both allows those fabrication and assembly requirements to be addressed together.

PCB and PCBA manufacturer USA

How EBest Circuit Supports US PCB and PCBA Buyers

With EBest Circuit, US customers can source bare PCBs, populated boards, or a complete turnkey build through one manufacturing partner. Our PCB manufacturing capabilities cover conventional FR4 and more demanding multilayer constructions.

Capability EBest Circuit support
FR4 layer count Up to 32 layers
HDI trace width/spacing Down to 2/2 mil
Small-component assembly Down to 01005
BGA assembly Down to 0.25 mm pitch
Assembly methods SMT, through-hole, and mixed assembly

The applicable combination depends on the board construction and component layout.

Keep component purchasing flexible. Our PCB assembly services include full turnkey, partial turnkey, and consignment work. You can use components already held by your team while we source the remaining parts, or have procurement included with the build.

Combine fine-pitch assembly with solder-joint inspection. Fine-pitch placement supports compact layouts, while AOI and X-ray inspection provide complementary checks for visible features and hidden solder joints.

Plan prototype and repeat builds with clear timing. Standard PCBA service is approximately one week, with expedited options for eligible projects. Our production lead times distinguish PCB fabrication from assembly; component procurement and delivery to the USA also need to fit the overall schedule.

Case Study: A 4-Layer Medical PCB for a US Customer

EBest Circuit worked with a US customer on a four-layer FR4 PCB for a medical product. The project required TG170 material, a finished thickness of 1.6764 mm ±10%, and 2 oz finished copper on every layer. The customer's PDF defined the layer structure.

Three requirements gave this board its specific manufacturing character:

  • The same finished copper requirement on all four layers. Both inner and outer layers required 2 oz copper. An outer-layer-only 2 oz specification would not describe this board correctly, and the customer's stackup formed part of the required construction.
  • Copper retention around non-plated holes. Where a pad was larger than an NPTH, the customer required its position and copper to remain unchanged. Secondary drilling was specified to produce the hole without treating the surrounding pad copper as material to remove.
  • A defined PTH copper requirement. Minimum hole-wall copper had to follow IPC-6012 Class 3 requirements. This was a distinct requirement from the 2 oz finished copper specified for the circuit layers.

The board also required lead-free HASL, glossy green solder mask on the top side, and white silkscreen clear of the pads. Routed internal corners had to follow the maximum radii on the drawing.

FAQs About PCB and PCBA manufacturer USA

Can a US assembly company work with overseas-manufactured PCBs?

Yes, if it accepts customer-supplied boards or sources them through a fabrication partner. This arrangement lets you retain a bare-board supplier while assembling closer to your US team.

Can prototype orders use a custom stackup?

Yes. Small quantity and custom construction can be combined. The order needs a service that accepts the specified stackup rather than a package limited to the supplier's standard constructions.

Can I provide some components and have the supplier purchase the rest?

Yes. Partial turnkey assembly supports this arrangement. It is useful when you already hold selected devices but want the manufacturer to procure the remaining components.

Does PCB electrical testing replace PCBA functional testing?

No. Bare-board electrical testing checks circuit connectivity before assembly. Functional testing evaluates the populated board against its intended functions and requires an appropriate test method.

Can EBest Circuit support a US project from bare boards through assembly?

Yes. EBest Circuit provides PCB fabrication, component sourcing, and assembly in China for US customers. The project can be supplied as bare boards or developed into a turnkey assembly order.

Discuss your next PCB or PCBA project with EBest Circuit at sales@bestpcbs.com. If you would like to meet the team and see our production operations before choosing a manufacturing partner, we welcome you to arrange a factory visit. PCB and PCBA manufacturer USA